
 EN
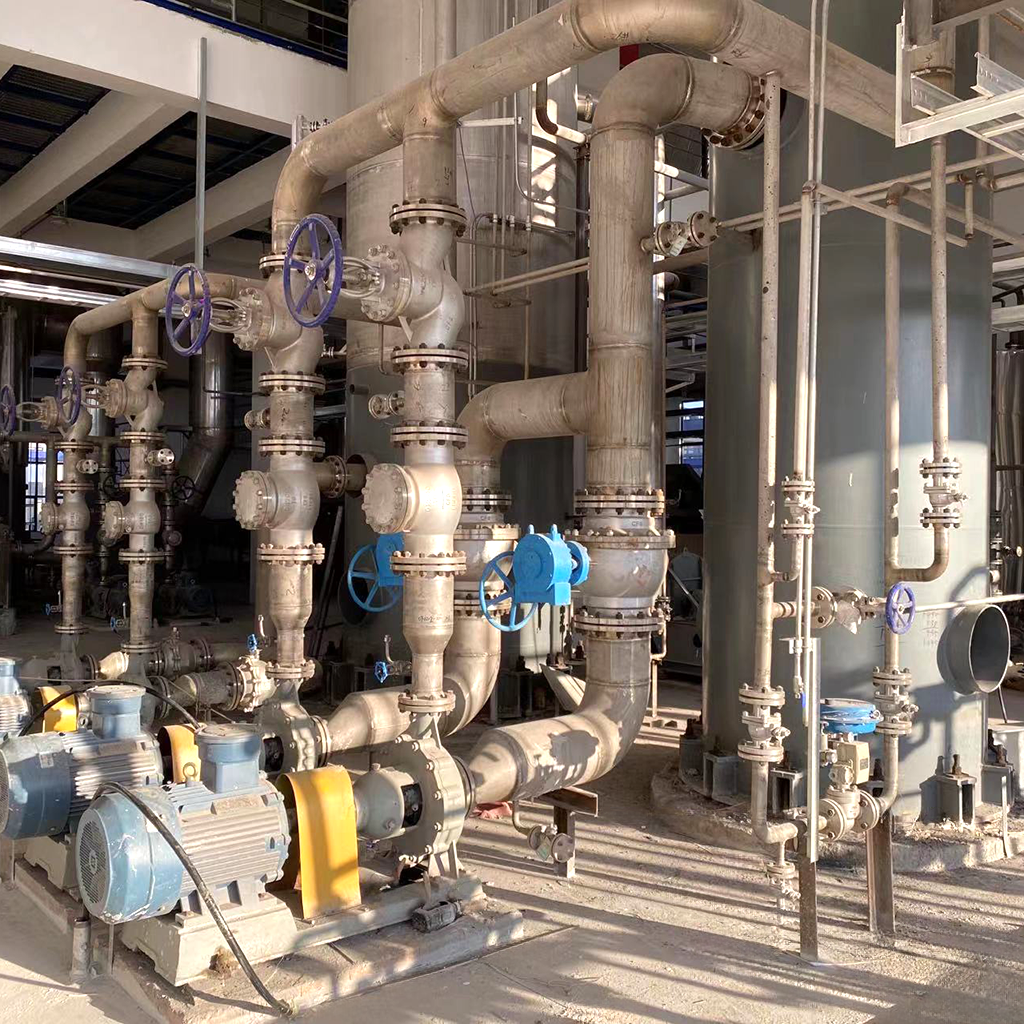
Tackling the Extreme Realities of Ethoxylation Machinery Selection
Industrial ethoxylation processes form an absolute bedrock within the global chemical manufacturing sector, serving as the critical foundational pathway for producing high-demand surfactants, non-ionic detergent intermediates, and specialized chemical products worldwide. This sophisticated chemical conversion relies entirely on the precise, highly controlled reaction of highly reactive ethylene oxide with active hydrogen compounds such as diverse industrial alcohols, fatty acids, and specialized amines. Operating a commercial-scale ethoxylation manufacturing facility introduces extraordinary technical and mechanical challenges, primarily driven by the extremely reactive, toxic, flammable, and explosive nature of ethylene oxide feedstocks. At the very center of these complex processing units lies an intricate rotating equipment network—comprising heavy-duty chemical process pumps, multi-stage synthesis compressors, and specialized reactor agitators—which must perform continuously and flawlessly under severe operating pressures and temperatures. Selecting, configuring, and maintaining this specialized machinery requires an uncompromising commitment to mechanical integrity, precision engineering design, and absolute safety compliance to ensure uninterrupted plant productivity without risking environmental contamination, fugitive emissions, or catastrophic equipment failure.
Optimizing Seal Integrity and Hydraulic Performance in Severe Services
A truly successful rotating equipment strategy for an advanced ethoxylation plant begins with rigorous attention to hydraulic design and, most importantly, advanced shaft sealing systems. Because ethylene oxide and its hazardous intermediate reaction mixtures present severe toxicity, acute flammability, and spontaneous polymerization hazards, even minor fugitive emissions or microscopic atmospheric seal leaks can quickly escalate into disastrous safety incidents within the processing environment. Drawing directly from extensive, hands-on field experience gathered across numerous international petrochemical plant construction projects and modular fabrication initiatives, seasoned mechanical engineers specify hermetically sealed canned motor pumps or advanced magnetic drive pump configurations to eliminate dynamic shaft seal leakage entirely from critical process loops. Where conventional heavy-duty centrifugal pumps are strictly required by plant layout specifications, tandem or double pressurized mechanical seals equipped with fully compatible barrier fluids, dual pressure control panels, and automated flush systems are deployed. Furthermore, comprehensive hydraulic profiling, detailed fluid vaporization margin evaluations, and Net Positive Suction Head margin calculations are rigorously enforced during the engineering design phase to prevent destructive internal cavitation, excessive vibration, and premature bearing wear within high-pressure transfer loops.
Meeting Strict International Mechanical Standards and Safety Codes
Operational reliability and safety within hazardous chemical plant rotating machinery can never rely on intuition, shortcuts, or basic design formulas; it must be firmly anchored in strict, unyielding compliance with globally recognized engineering codes and industrial standards. Leading technical authorities and industrial institutions, including the American Petroleum Institute through standards such as API for heavy-duty centrifugal pumps and industrial compressors, alongside the International Organization for Standardization, provide the essential engineering baselines required for robust machinery fabrication, rigorous shop testing, and structural performance. Top-tier engineering design teams supplement these baseline standards with exhaustive hazardous area classifications, including strict ATEX and IECEx directives, ensuring that all driving electric motors, instrumentation packages, and mechanical couplings are fully certified as explosion-proof. By aligning every single machinery selection and procurement milestone with these stringent international safety benchmarks, plant operators effectively eliminate operational hazards, protect on-site personnel, and guarantee flawless regulatory compliance throughout the entire asset lifecycle.
Balancing Initial Capital Expenditure with Long-Term Asset Reliability
From a broader commercial and financial perspective, the careful, deliberate selection of rotating equipment directly dictates the long-term financial viability and overall operational profitability of an industrial ethoxylation facility. While specifying specialized metallurgy, leak-free canned motors, redundant barrier fluid systems, and API-compliant heavy-duty machinery naturally demands a higher initial capital expenditure layout during the initial procurement and plant construction phase, this targeted strategic investment yields immense, quantifiable dividends over time. Unplanned emergency downtime, catastrophic bearing seizures, or mechanical seal failures in a primary ethylene oxide service line can result in staggering daily production losses, severe environmental regulatory fines, and extremely costly emergency contractor repairs. High-integrity machinery design significantly extends the mean time between failures, reduces routine maintenance overhaul intervals, and optimizes ongoing operating expenditures over decades of continuous service. Transparent lifecycle cost evaluations, detailed energy efficiency assessments, and proactive risk mitigation ensure that facility investors achieve a predictable, highly rewarding return on capital investment.
Securing Project Success Through End-to-End Engineering Expertise from SL-TECH
Executing complex mechanical engineering designs, precise equipment selections, and reliable integration for hazardous chemical manufacturing environments requires a trusted, highly capable industry partner backed by deep technical mastery, extensive fabrication know-how, and robust global supply chain execution capabilities. As a recognized leader in advanced chemical technology solutions, SL-TECH delivers exceptional engineering services, specialized core equipment integration, and full-lifecycle project execution for essential processing industries across the globe. From initial process design consulting, customized equipment specification, and precision procurement to professional site installation, rigorous system commissioning, and thorough operator training, SL-TECH stands fully prepared to support your upcoming facility expansion or plant modernization initiative. Partnering with an experienced specialist like SL-TECH allows your facility to harness cutting-edge mechanical engineering, streamline global supply chain networks, and secure long-term operational excellence for your next major chemical project.
Table of Contents
- Tackling the Extreme Realities of Ethoxylation Machinery Selection
- Optimizing Seal Integrity and Hydraulic Performance in Severe Services
- Meeting Strict International Mechanical Standards and Safety Codes
- Balancing Initial Capital Expenditure with Long-Term Asset Reliability
- Securing Project Success Through End-to-End Engineering Expertise from SL-TECH