
 EN
Navigating Modern Modular Chemical Engineering
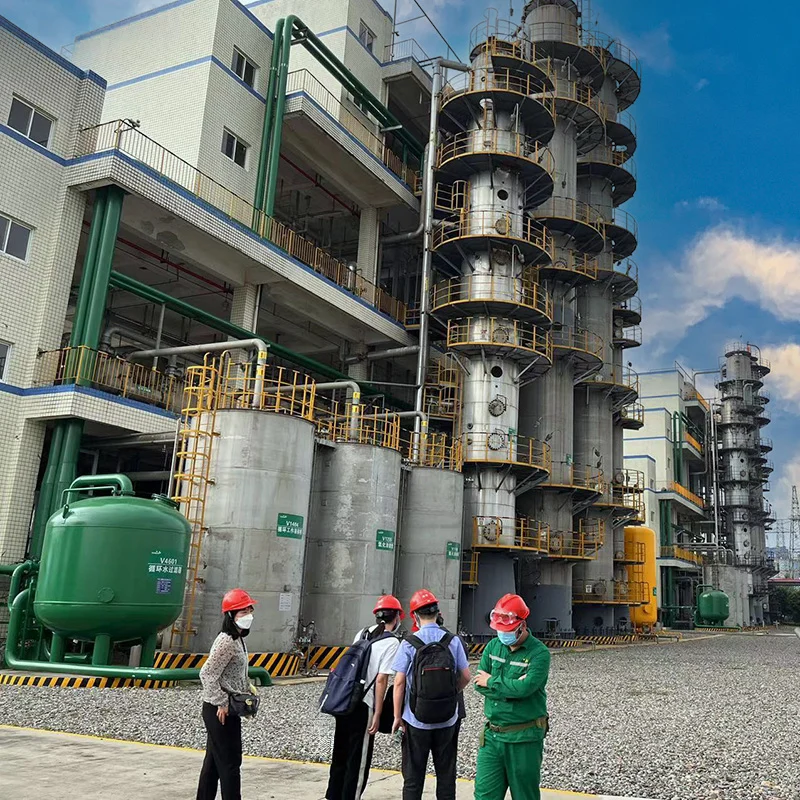
In the dynamic landscape of contemporary chemical processing, operational agility, high precision, and fast execution define true industry leadership. Traditional stick-built chemical plants are frequently plagued by prolonged construction timelines, unpredictable on-site labor costs, severe labor shortages, and complex regulatory compliance hurdles that can easily derail capital expenditure budgets. Drawing from extensive practical field experience in deploying advanced modular process systems across diverse global terrains, modern engineering practices have systematically shifted toward standardized modular architecture. A skid-mounted modular plant integrates essential process infrastructure—including specialized pumps, chemical reactors, shell-and-tube heat exchangers, and fractional distillation columns—onto a unified, pre-fabricated structural steel framework. When combined with advanced physical separation technologies like Pressure Swing Distillation (PSD), this innovative delivery model fundamentally transforms how specialty chemicals such as methylal are synthesized, separated, and purified on a commercial scale, yielding remarkable reliability, optimal energy efficiency, and predictable plant performance across long-term lifecycle operations.
The Technical Imperative of Methylal and Pressure Swing Distillation
Methylal functions as an increasingly vital green solvent and chemical intermediate widely utilized across high-performance resins, structural adhesives, personal care cosmetics, and clean fuel oxygenate additives. However, producing high-purity methylal presents a classic, stubborn thermodynamic challenge: it forms a low-boiling azeotropic mixture with unreacted methanol and water. Standard fractional distillation columns inherently fail to cross this thermodynamic azeotropic boundary because the vapor and liquid compositions at the azeotropic point remain identical. To decisively overcome this barrier, senior engineering teams leverage Pressure Swing Distillation, an advanced, thermodynamically sophisticated method that exploits the distinct shift in azeotropic composition under varying operating pressure regimes. By alternating operating pressures across dual or multi-column configurations, the system successfully breaks the azeotrope without introducing extraneous chemical entrainers or solvents. This ensures an exceptionally high final product solvent purity while minimizing downstream wastewater generation, reducing energy footprints, and eliminating chemical contamination risks.
Engineering Advantages of Skid-Mounted Modular Architecture
Transitioning a complex azeotropic distillation unit from traditional field construction into a compact, skid-mounted format requires rigorous multi-disciplinary expertise spanning chemical kinetics, stress analysis, thermodynamic modeling, and modular layout optimization. Prefabrication takes place exclusively within controlled, certified manufacturing facilities where stringent non-destructive testing, automated radiographic weld checks, and rigorous hydrostatic pressure standards are enforced without exception. Industry benchmarking across international process sectors indicates that modularizing an entire chemical plant cuts on-site construction labor hours substantially and reduces civil engineering footprint requirements by a wide margin. Furthermore, complex pipe racks, integrated electrical cabling, and intricate instrumentation loops are fully pre-assembled and pre-tested off-site, which drastically mitigates mechanical alignment errors, minimizes on-site welding hazards, and eliminates costly commissioning delays during final field installation.
Operational Excellence, Safety, and Automation
Safety, transparency, and operational continuity serve as non-negotiable pillars in modern chemical manufacturing environments. Pressure swing distillation inherently involves shifting thermal profiles, precise temperature gradients, and fluctuating pressure boundaries that demand robust, fail-safe automation architectures. Modern skid-mounted methylal units are seamlessly integrated with advanced Distributed Control Systems and independent Safety Instrumented Systems, fully complying with rigorous international safety benchmarks such as HAZOP and SIL guidelines. Real-time telemetry sensors continuously track vapor-liquid equilibria, reflux ratios, reboiler duties, and high-speed compressor loads. Based on extensive empirical operational case data, automated closed-loop feedback systems embedded within these modular units significantly reduce human operator intervention errors, ensuring stable, continuous-flow production even when managing fluctuating feedstock purities and seasonal ambient temperature variations.
Commercial Value and Capital Efficiency for Project Owners
Beyond technical ingenuity and operational safety, the primary economic rationale for investing in a skid-mounted methylal plant centers on accelerated time-to-market and an optimized total cost of ownership. Traditional chemical plant fabrication methods frequently lock up substantial corporate capital for years before achieving initial nameplate capacity and revenue generation. In contrast, modular delivery drastically compresses the entire project lifecycle, allowing chemical producers to capture favorable market windows rapidly and achieve a substantially faster return on investment. Furthermore, reduced on-site labor overhead, minimized raw material waste generation during factory fabrication, and inherent modular scalability translate into superior financial resilience. This makes high-tech, capital-intensive chemical manufacturing accessible, low-risk, and commercially viable for growing industrial enterprises seeking sustainable market expansion.
Delivering Turnkey Modular Excellence with SL-TECH
Realizing the full commercial and technical potential of complex, azeotropic chemical processes requires a manufacturing partner equipped with robust global supply chain networks, meticulous quality assurance protocols, and comprehensive end-to-end execution capabilities. SL-TECH stands firmly at the forefront of this modern industrial evolution, delivering fully operational, highly scalable skid-mounted modular plants tailored precisely to exact client specifications—ranging from specialty solvents like high-purity methylal to intricate petrochemical derivatives. Backed by world-class pressure vessel fabrication facilities, advanced automation integration expertise, and rigorous international project management standards, SL-TECH effectively bridges the complex gap between advanced chemical engineering theory and reliable, profitable, and sustainable industrial reality. To maximize future plant reliability, partnering with trusted global experts ensures complete project success from initial concept through final commissioning.
Table of Contents
- Navigating Modern Modular Chemical Engineering
- The Technical Imperative of Methylal and Pressure Swing Distillation
- Engineering Advantages of Skid-Mounted Modular Architecture
- Operational Excellence, Safety, and Automation
- Commercial Value and Capital Efficiency for Project Owners
- Delivering Turnkey Modular Excellence with SL-TECH