
ansi compliant chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Environmentally-Friendly Chemical Industrial Equipment Supply

Environmentally-Friendly Chemical Industrial Equipment Supply

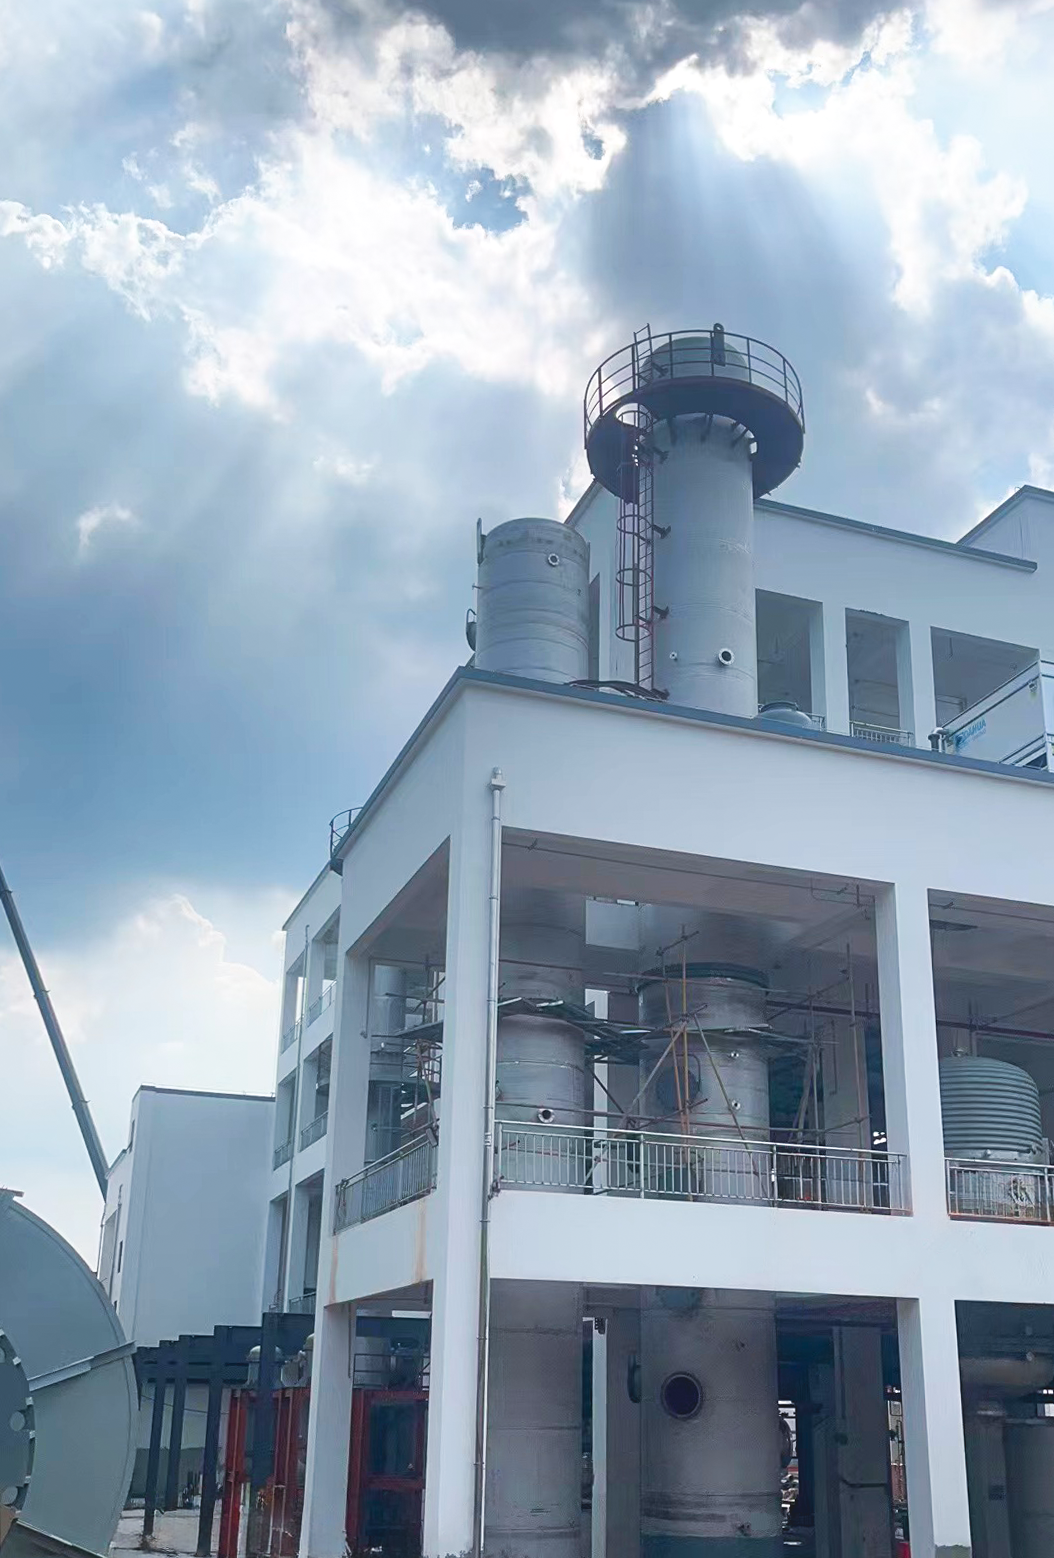
We are committed to providing environmentally-friendly chemical industrial equipment supply. Our equipment is designed to minimize environmental impact during chemical processes. For example, our energy-efficient pumps reduce power consumption, and our skid-mounted systems are built with sustainable materials, contributing to a greener chemical industry.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

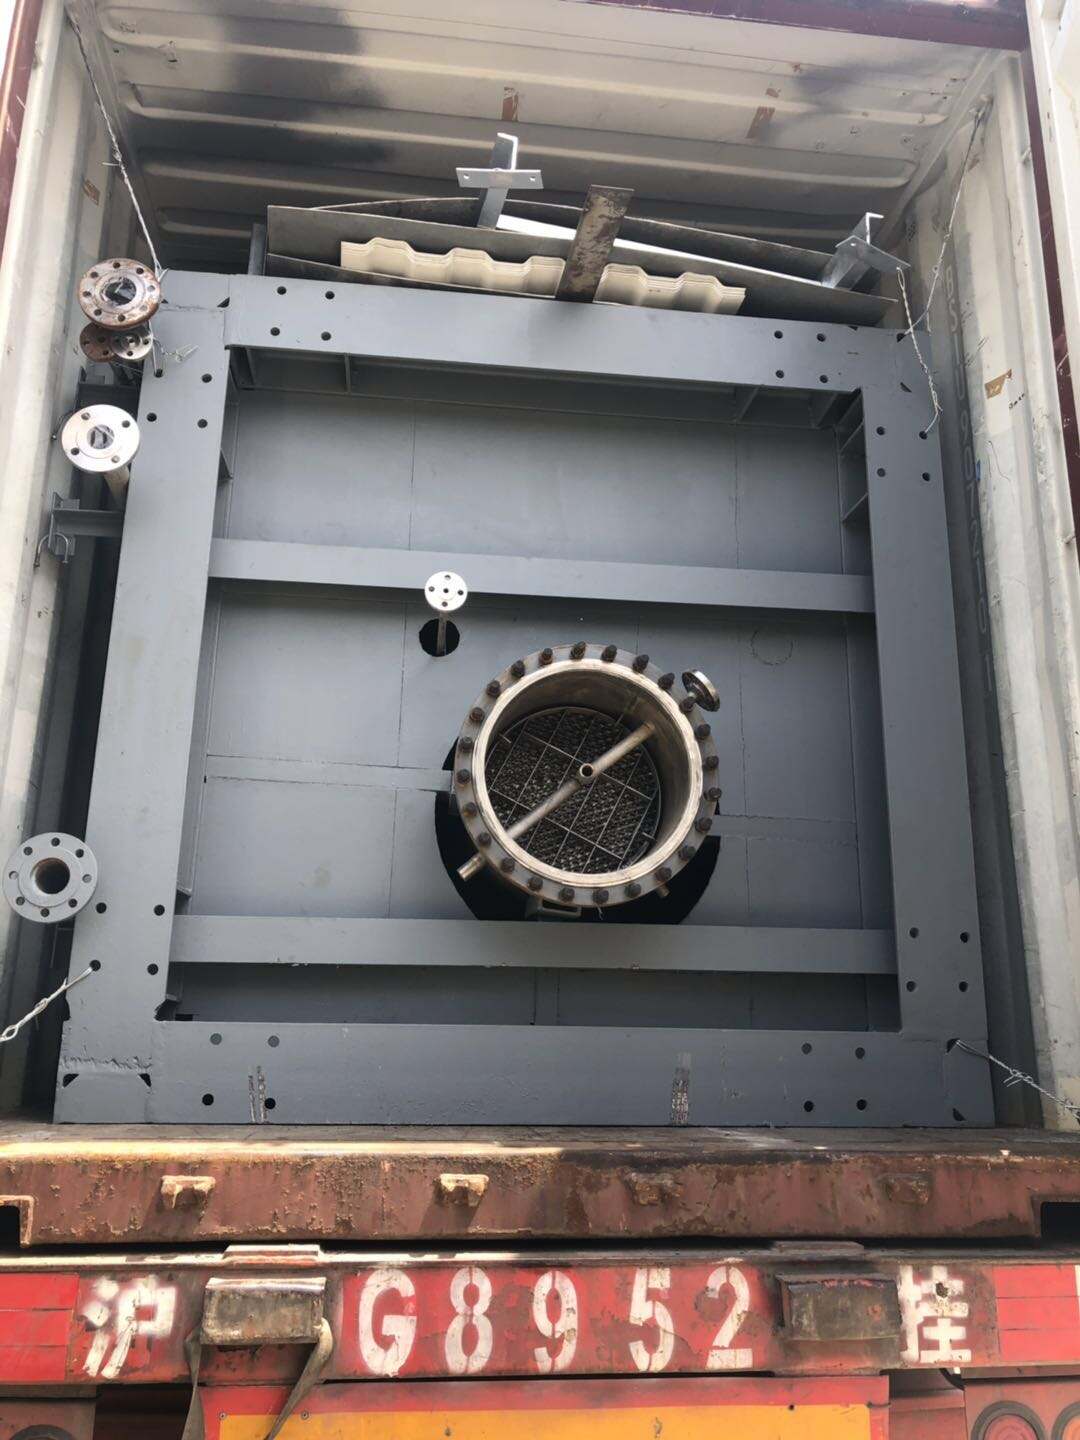
We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

Related products

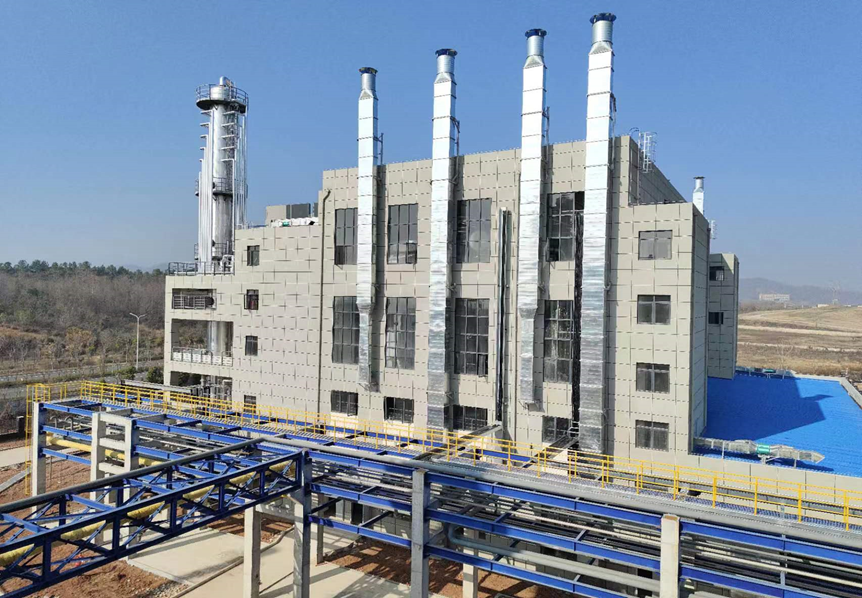
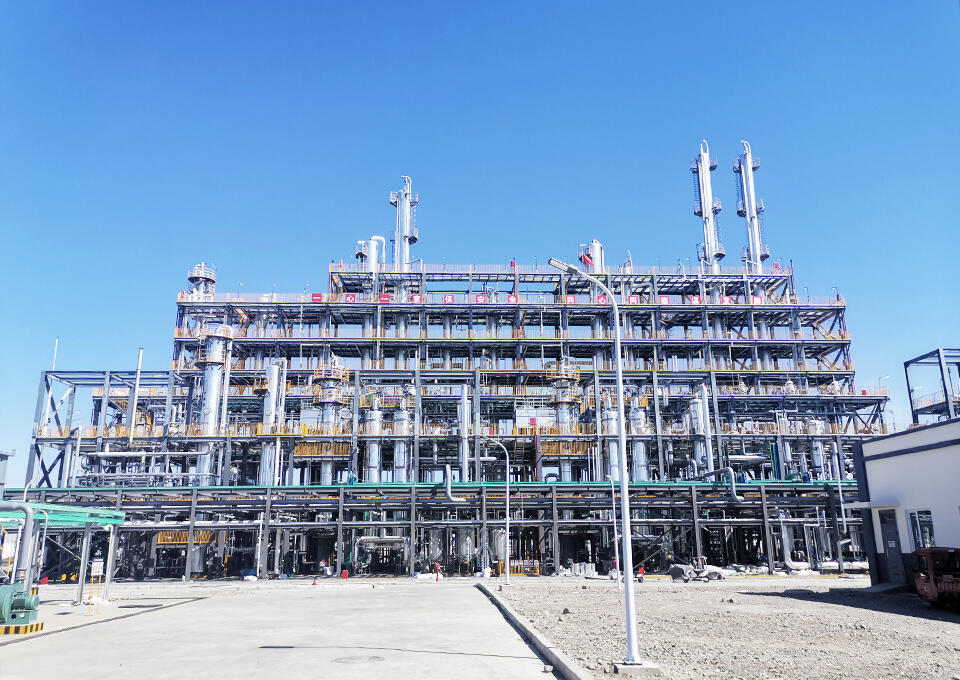
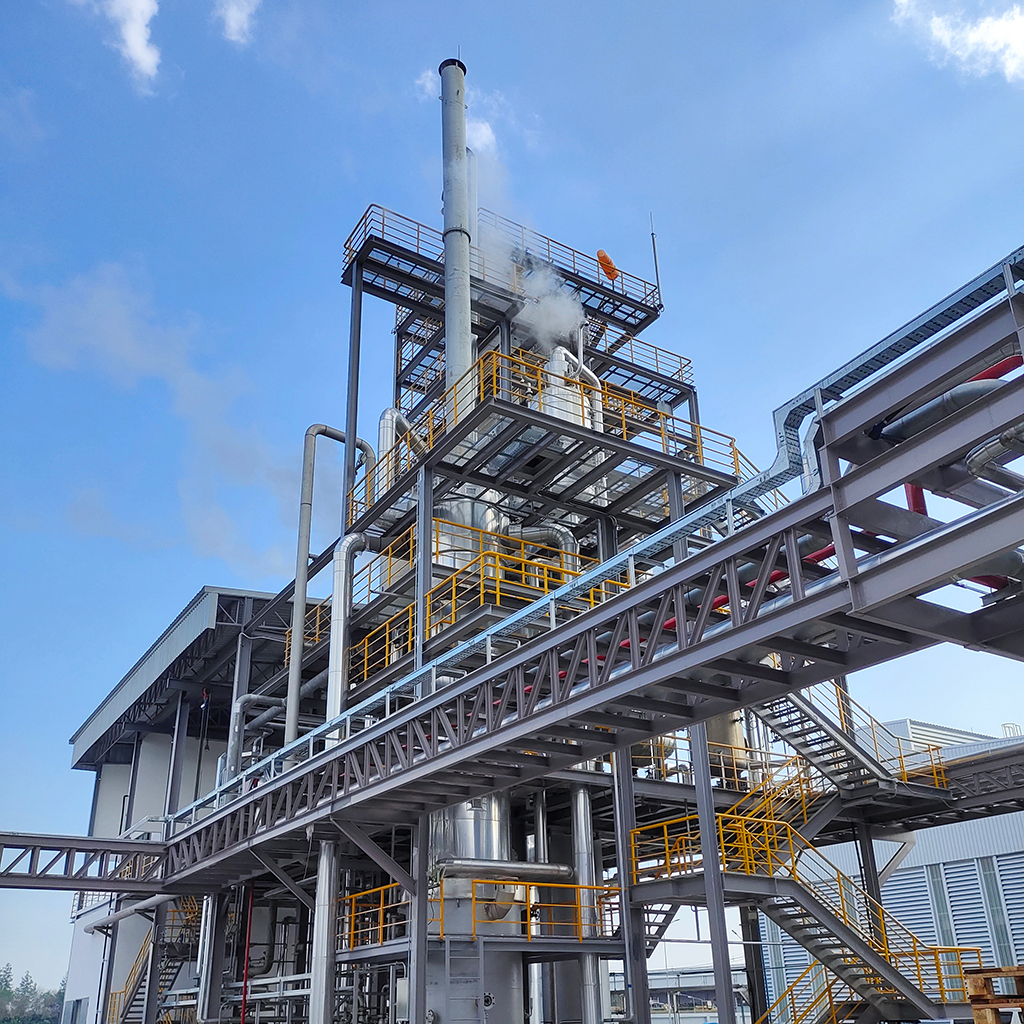
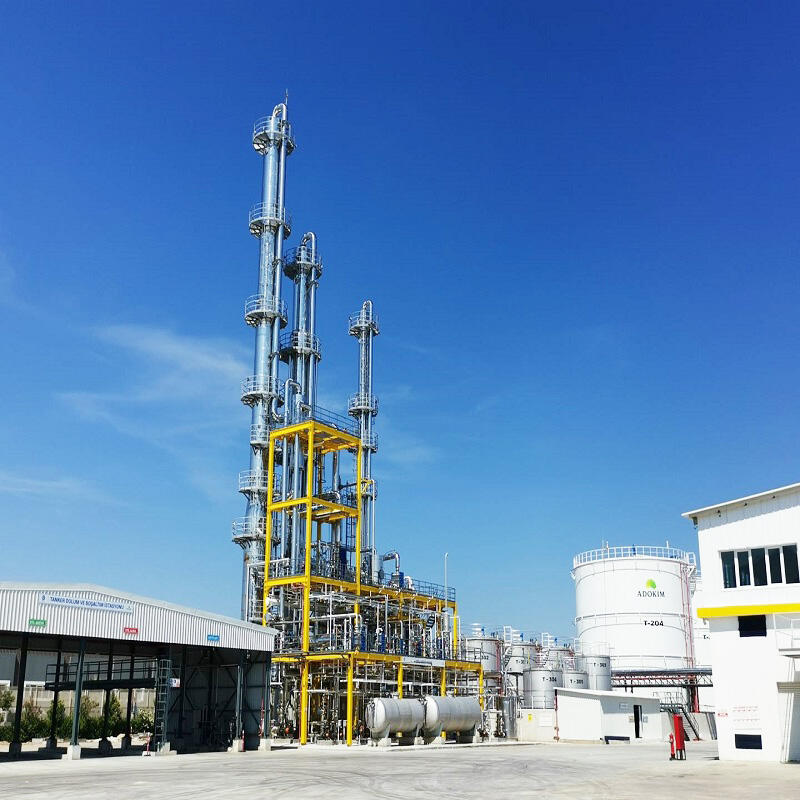
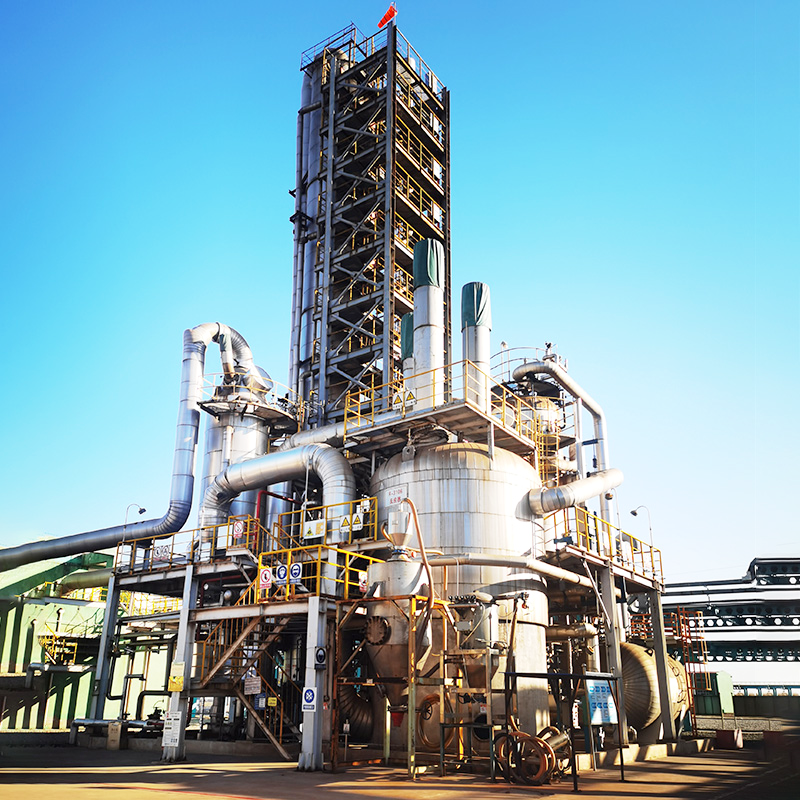
The significance of chemical industrial equipment supply in the chemical manufacturing industry cannot be overstated. Changzhou Sanli Tech International Trade Co., Ltd. is dedicated to providing high-quality equipment that enhances the efficiency and safety of chemical processes. Our product portfolio includes a variety of pumps, such as positive displacement pumps and centrifugal pumps, each designed to handle specific chemical properties and process conditions. For example, our positive displacement pumps, including gear pumps and screw pumps, are ideal for applications requiring precise flow control and gentle handling of viscous and shear-sensitive chemicals. A client in the food and beverage industry needed a pump that could accurately dose high-viscosity food additives without altering their consistency. We provided them with our gear pumps, which offered a reliable and precise solution, enhancing their production efficiency and product quality. Beyond pumps, we offer skid-mounted systems that incorporate the latest technology for improved process control and monitoring. These systems can be equipped with sensors, actuators, and advanced control systems, allowing for real-time data collection and analysis. A client in the chemical processing industry implemented our skid-mounted system with integrated control, which enabled them to optimize their process parameters, reduce waste, and improve product quality. Our chemical industrial equipment supply is supported by a team of engineers who provide expert advice and technical support, ensuring our clients make informed decisions and achieve optimal results.

Frequently Asked Questions

What on - site guidance services does the company offer for chemical plant operation?

For new chemical plants, it helps operators get familiar with equipment operation rules, processes, and safety precautions. For running plants, when production failures or process problems occur, on - site engineers can quickly diagnose and solve them, such as finding the root cause of abnormal tower pressure drops and proposing solutions.
It uses big data analysis to collect, analyze, and mine production data for process optimization, fault prediction, and quality improvement. Artificial intelligence algorithms enable intelligent control of production parameters. IoT technology allows remote monitoring and management of equipment, enabling engineers to check status, receive alarms, and perform operations remotely.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Uses and Safety Precautions of Formaldehyde in Industry

23

Jul

Uses and Safety Precautions of Formaldehyde in Industry

Explore the industrial applications, safety measures, regulatory frameworks, and innovation trends of formaldehyde. Discover its role in resin production, healthcare disinfectants, wood composites, and alternatives like bio-based adhesives and low-VOC resins.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More

Customer Reviews

Sarah Davis

The manufacturing quality of the chemical industrial equipment is outstanding. The equipment is precisely made, and the attention to detail is evident. The non - metallic pumps we purchased have excellent corrosion resistance, which is crucial for our chemical processing.

John Smith

The chemical industrial equipment supplied by this company is of top - notch quality. The materials used are durable and can withstand harsh chemical environments. The pumps, for example, have been running smoothly in our plant for a long time without any major issues. Highly recommended!

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.