
ansi standard chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Innovative Chemical Industrial Equipment Supply for Growth

Innovative Chemical Industrial Equipment Supply for Growth

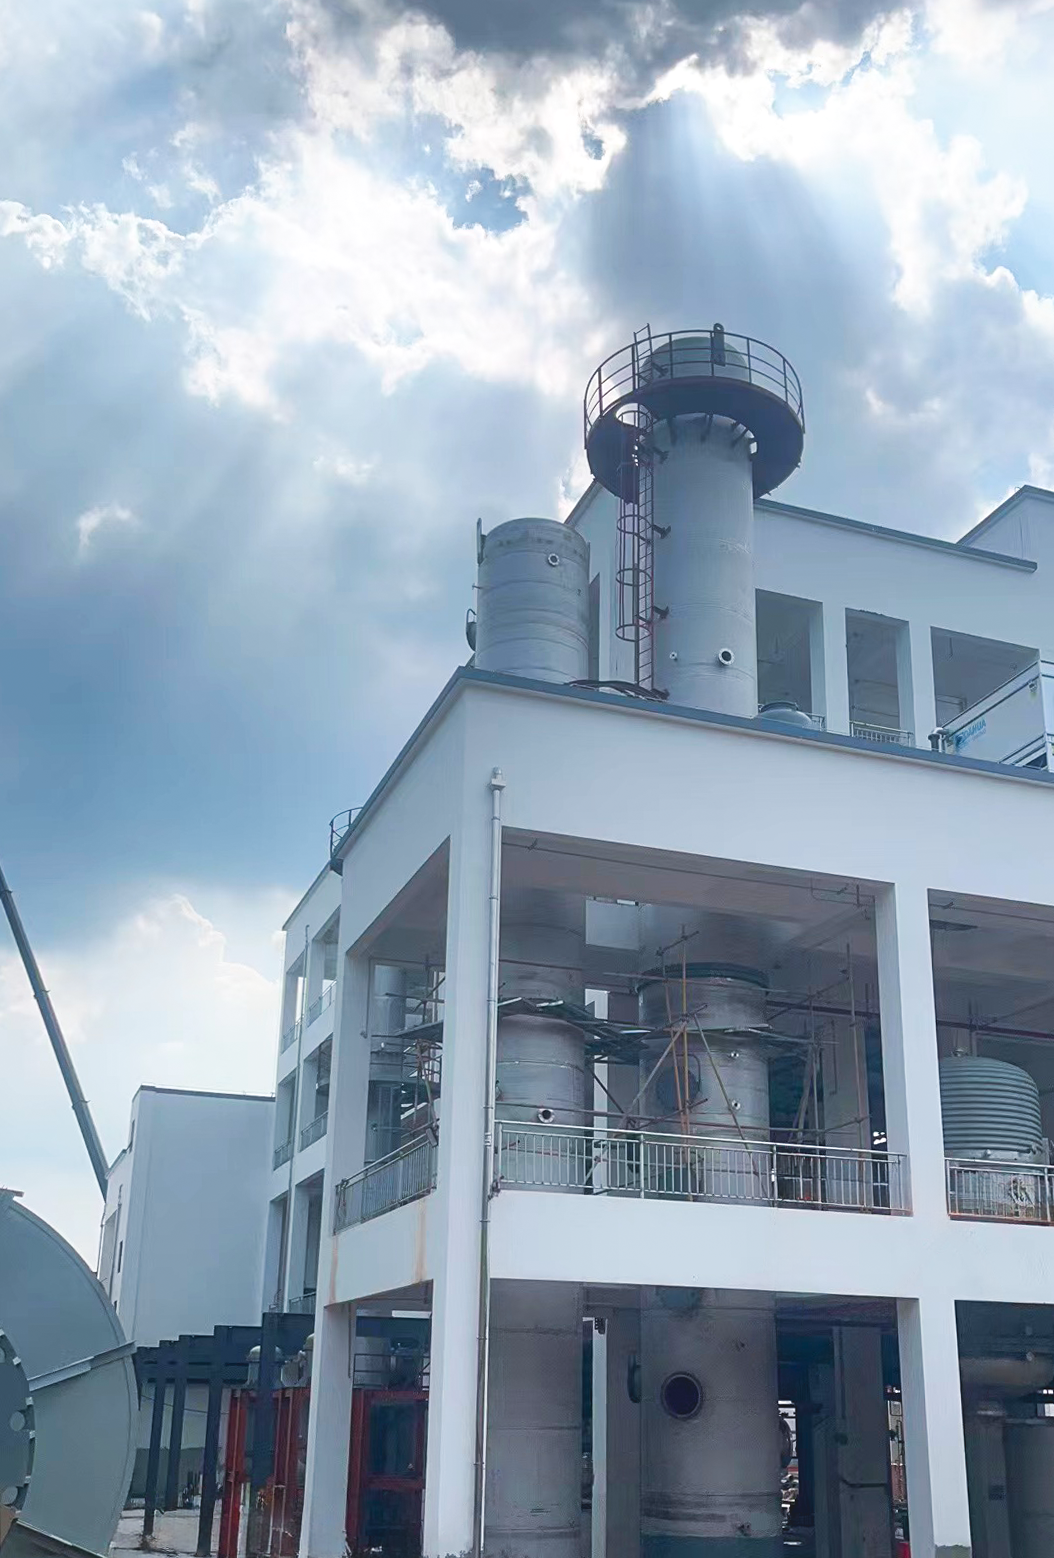
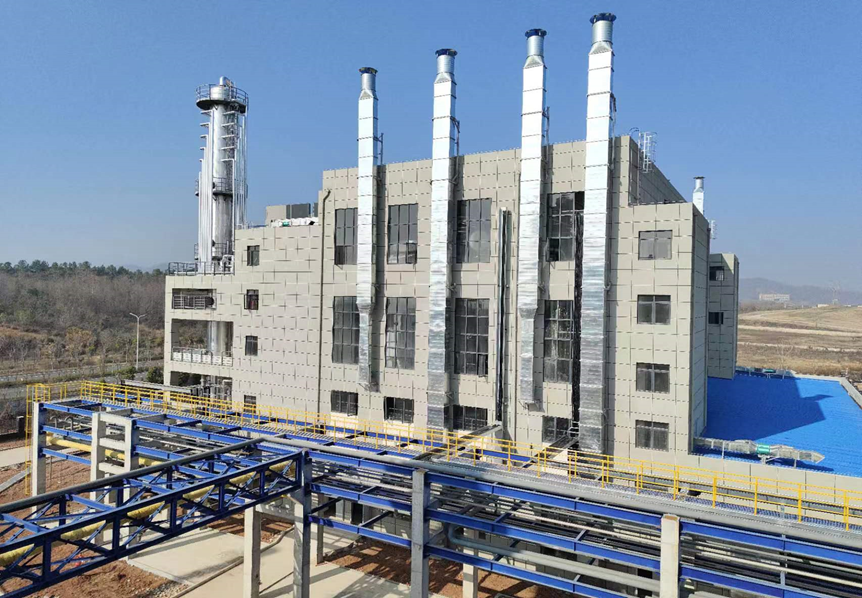
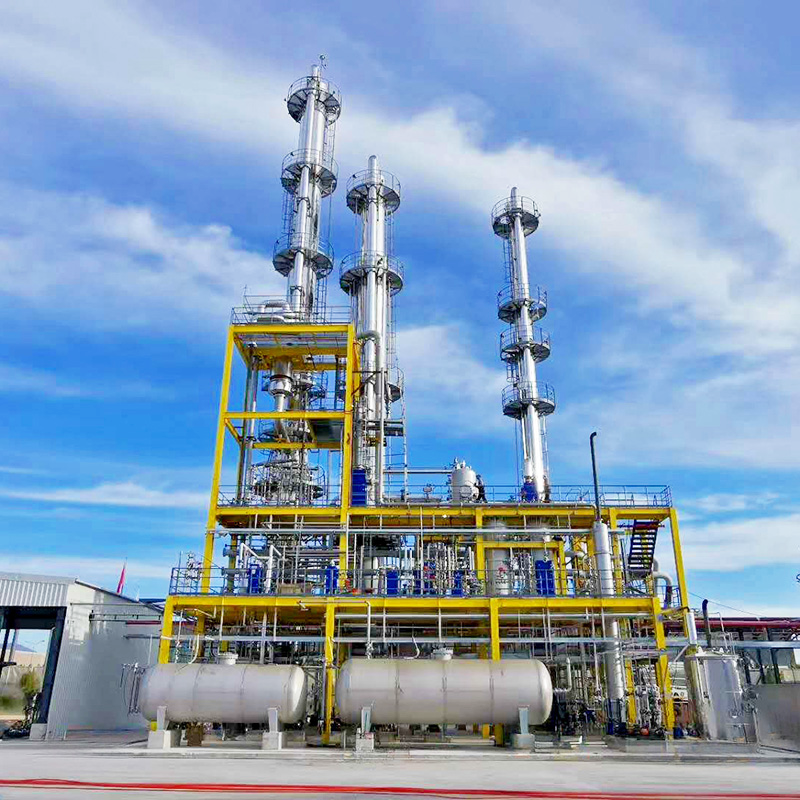
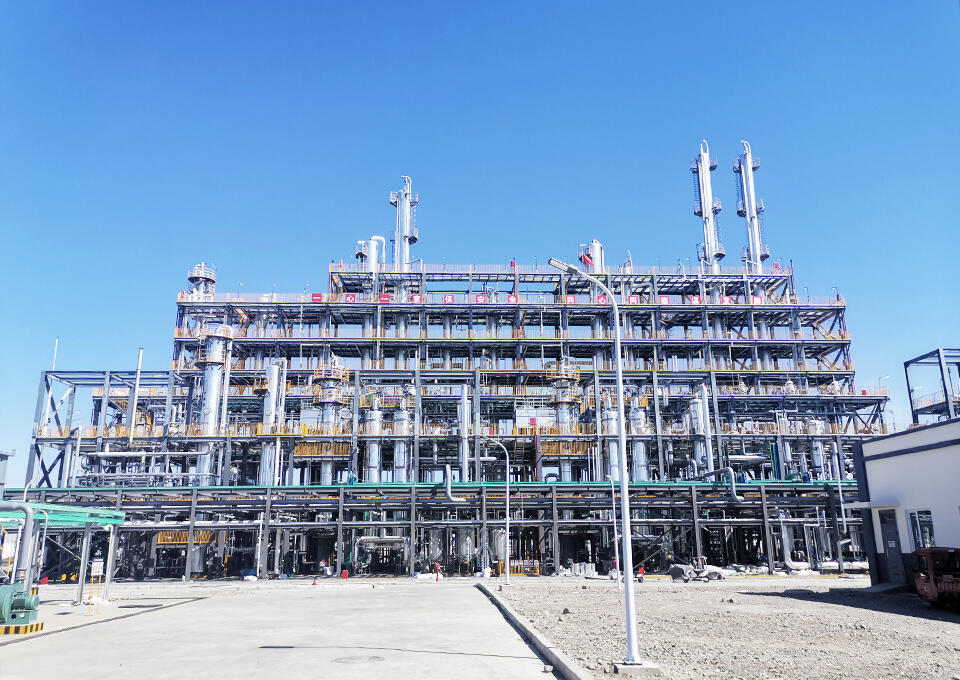
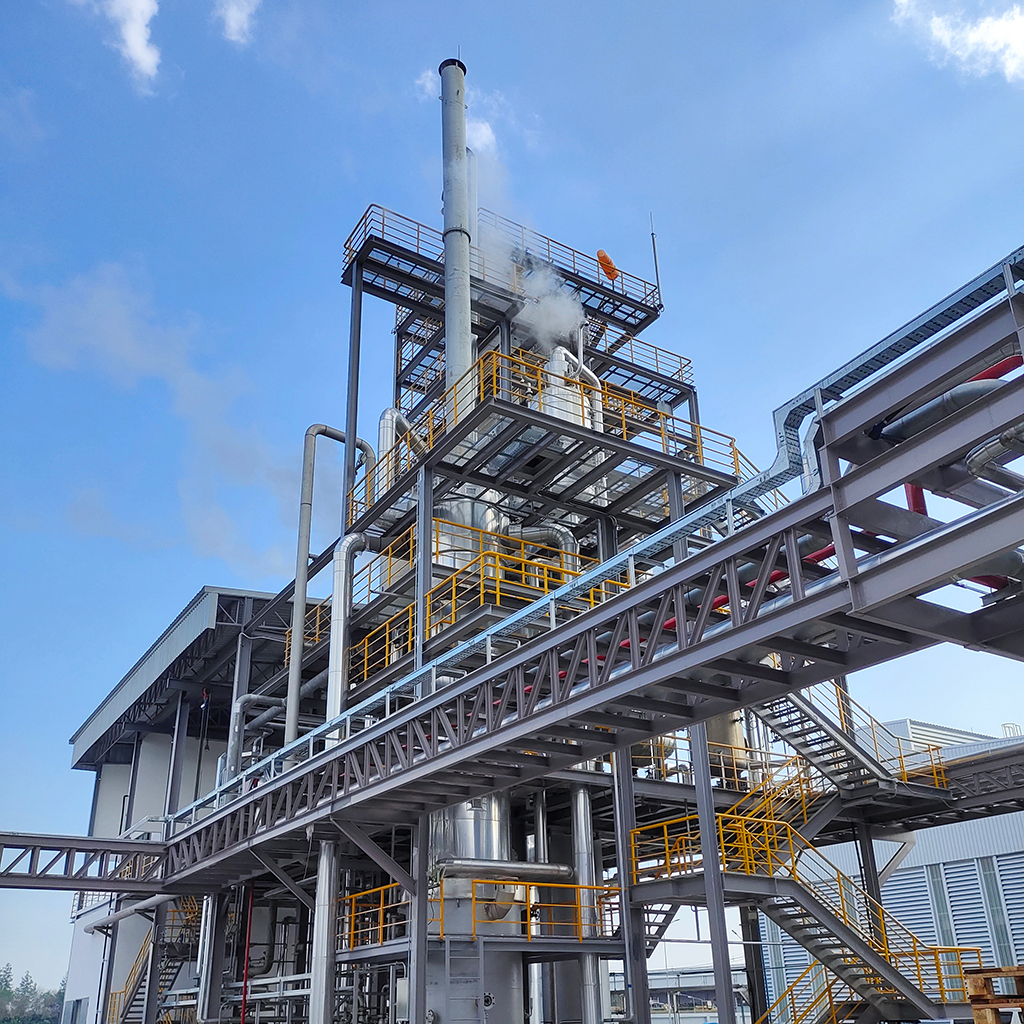
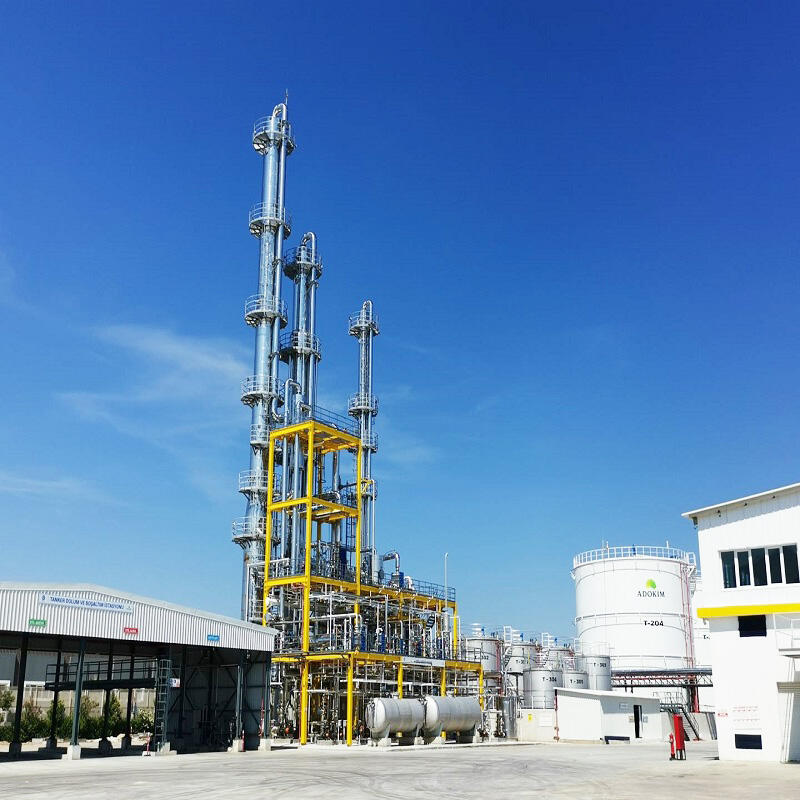
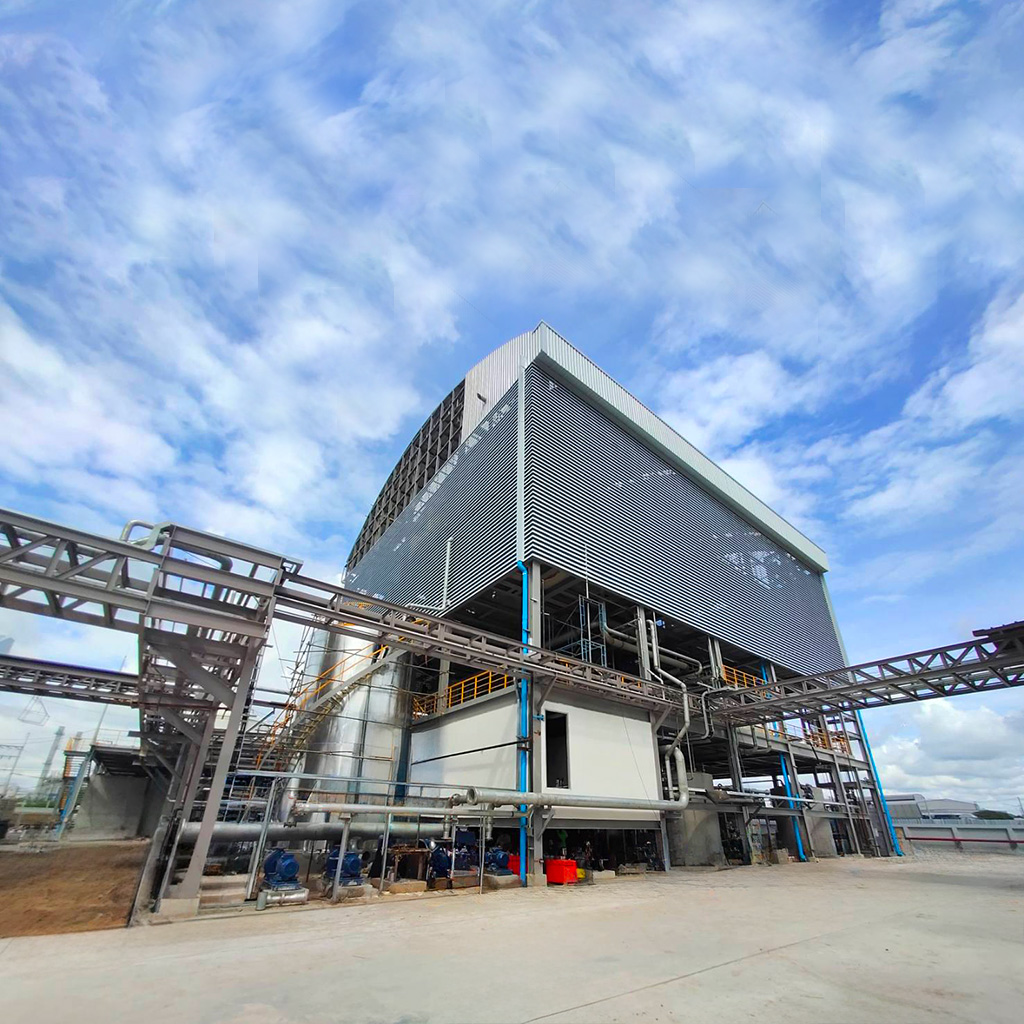
We are at the forefront of innovation in chemical industrial equipment supply. Our products feature innovative designs and technologies that drive growth in chemical production. From new pump models to cutting-edge skid-mounted solutions, we help you stay ahead of the competition and expand your business.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

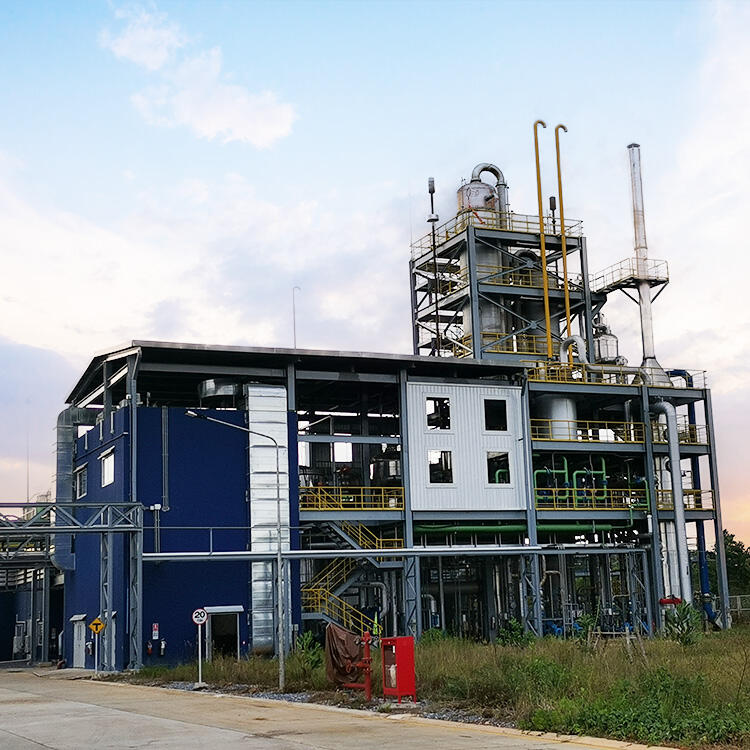
Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

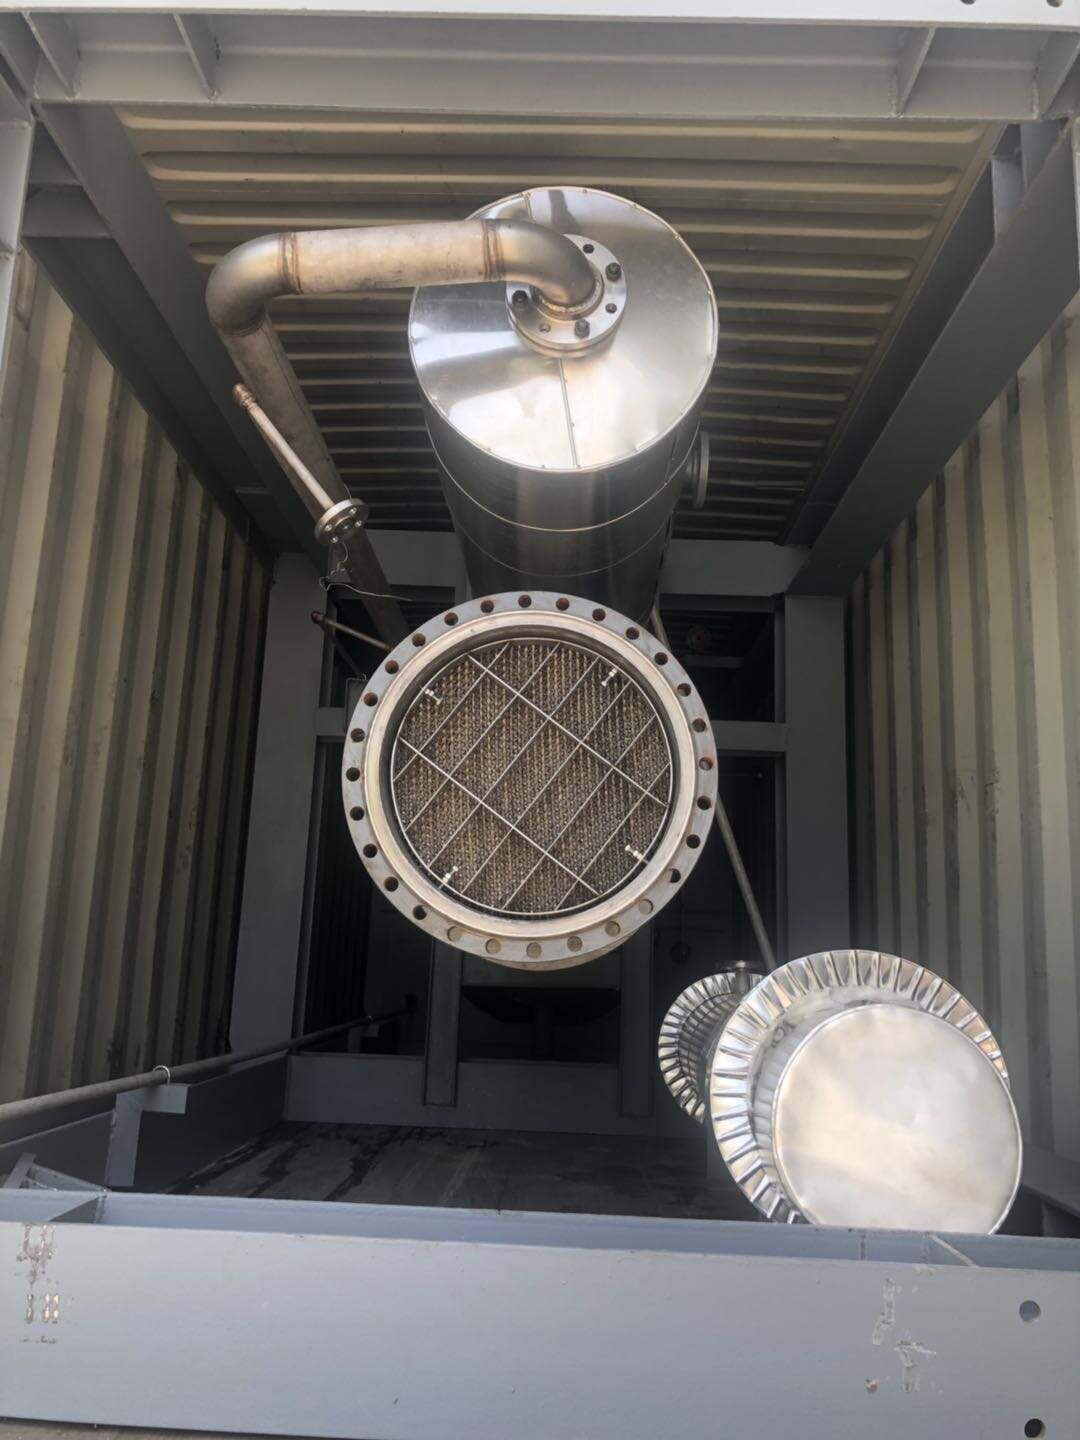
Chemical industrial equipment supply plays a pivotal role in the optimization of chemical manufacturing processes. Changzhou Sanli Tech International Trade Co., Ltd. offers a wide array of equipment that not only meets but exceeds industry standards, ensuring optimal performance and longevity. Our equipment is designed with the end-user in mind, focusing on ease of use, maintenance, and safety. For instance, our range of centrifugal pumps, including vertical and horizontal models, are engineered for high-flow applications, making them ideal for large-scale chemical processing. A client in the water treatment industry required a pump that could handle high volumes of water with minimal energy consumption. We provided them with our energy-efficient centrifugal pumps, which not only met their flow requirements but also reduced their operational costs. In addition to standard pumps, we specialize in custom skid-mounted systems that can be tailored to specific process needs. These systems can include a combination of pumps, valves, and instrumentation, all mounted on a single skid for easy installation and operation. A recent project involved designing a skid-mounted system for a chemical storage and transfer application. The system included a pump, flow meter, and control valve, all pre-assembled and tested, ensuring a seamless integration into the client's existing infrastructure. Our chemical industrial equipment supply is backed by a team of experts who provide comprehensive support, from initial consultation to after-sales service, ensuring our clients achieve the best possible outcomes.
Frequently Asked Questions

What advantages does the company have in the ethylene field?

It has in - depth research and practical experience in ethylene production technologies, including traditional tubular furnace cracking and emerging catalytic cracking. It offers one - stop services from process package design to equipment procurement and installation for ethylene production plant construction. For existing plants, it provides technical renovation services to improve yield and efficiency, and supports downstream product development.
It can provide formaldehyde production process design and supporting equipment for efficient, safe, and stable production. It uses advanced catalyst and reaction condition control technology to improve yield and purity. It also has solutions for tail - gas treatment to meet environmental requirements. The supplied formaldehyde meets the needs of multiple industries like chemicals, building materials, and textiles.
For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
It supplies a wide range of equipment for the chemical market. Pump types include barrel and container pumps, pneumatic diaphragm pumps, eccentric disc pumps, etc. Besides single pumps and fan components, it provides customized skid - mounted equipment for single - point connection and cost - reducing installation, complying with relevant API and ANSI standards.

Related Articles

Analysis On Production Technology And Industrial Chain Of FM

28

Nov

Analysis On Production Technology And Industrial Chain Of FM

View More
Uses and Safety Precautions of Formaldehyde in Industry

23

Jul

Uses and Safety Precautions of Formaldehyde in Industry

Explore the industrial applications, safety measures, regulatory frameworks, and innovation trends of formaldehyde. Discover its role in resin production, healthcare disinfectants, wood composites, and alternatives like bio-based adhesives and low-VOC resins.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Intersection of Chemistry and Engineering in Production Technology

23

Jul

The Intersection of Chemistry and Engineering in Production Technology

Explore the transformative role of chemical engineering in production technology, digital transformation in chemical manufacturing using AI and IoT, sustainable material innovations, and future trends in polymer manufacturing and nanotechnology. Understand the significance of optimizing processes for efficiency and sustainability.
View More

Customer Reviews

Lisa Garcia

The chemical industrial equipment we bought from this company has proven to be very durable. It has been exposed to various chemicals and harsh operating conditions, but it still functions well. This long - lasting performance has reduced our equipment replacement costs.

Jennifer Lee

The delivery of the chemical industrial equipment was extremely fast. We placed an urgent order, and the company managed to ship it within the promised time frame. This quick response helped us avoid production delays and keep our operations running smoothly.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.