
centrifugal vertical chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Cost-Effective Chemical Industrial Equipment Supply Options

Cost-Effective Chemical Industrial Equipment Supply Options

Looking for cost-effective chemical industrial equipment supply? Look no further. We provide a range of affordable yet high-quality products. Our pumps and skid-mounted equipment are designed to offer great value for money, helping you save on initial investment and long-term operating costs in your chemical facility.
Get A Quote

Why choose us?

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

The significance of chemical industrial equipment supply cannot be overstated in the context of modern chemical manufacturing. Changzhou Sanli Tech International Trade Co., Ltd. is dedicated to providing high-quality equipment that enhances the efficiency and safety of chemical processes. Our product portfolio includes a variety of pumps, such as air-operated double diaphragm pumps and magnetic drive pumps, each designed to handle specific chemical properties and process conditions. For example, our air-operated double diaphragm pumps are ideal for applications requiring explosion-proof and self-priming capabilities, making them suitable for hazardous chemical handling. A client in the petrochemical industry needed a pump that could safely transfer flammable liquids without the risk of sparking. We supplied them with our air-operated double diaphragm pumps, which provided a safe and reliable solution, ensuring the safety of their operations. Beyond pumps, we offer skid-mounted systems that integrate multiple components into a single, compact unit, reducing installation time and costs. These systems can be customized to include various pumps, valves, and control systems, all designed to work seamlessly together. A recent project involved supplying a skid-mounted system for a chemical dosing application. The system included a metering pump, flow meter, and control panel, allowing the client to accurately dose chemicals and monitor the process in real-time. Our chemical industrial equipment supply is supported by a team of engineers who provide expert advice and technical support, ensuring our clients make informed decisions and achieve optimal results.
Frequently Asked Questions

What personnel training courses does the company provide for chemical plants?

For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
For new chemical plants, it helps operators get familiar with equipment operation rules, processes, and safety precautions. For running plants, when production failures or process problems occur, on - site engineers can quickly diagnose and solve them, such as finding the root cause of abnormal tower pressure drops and proposing solutions.
It supplies a wide range of equipment for the chemical market. Pump types include barrel and container pumps, pneumatic diaphragm pumps, eccentric disc pumps, etc. Besides single pumps and fan components, it provides customized skid - mounted equipment for single - point connection and cost - reducing installation, complying with relevant API and ANSI standards.
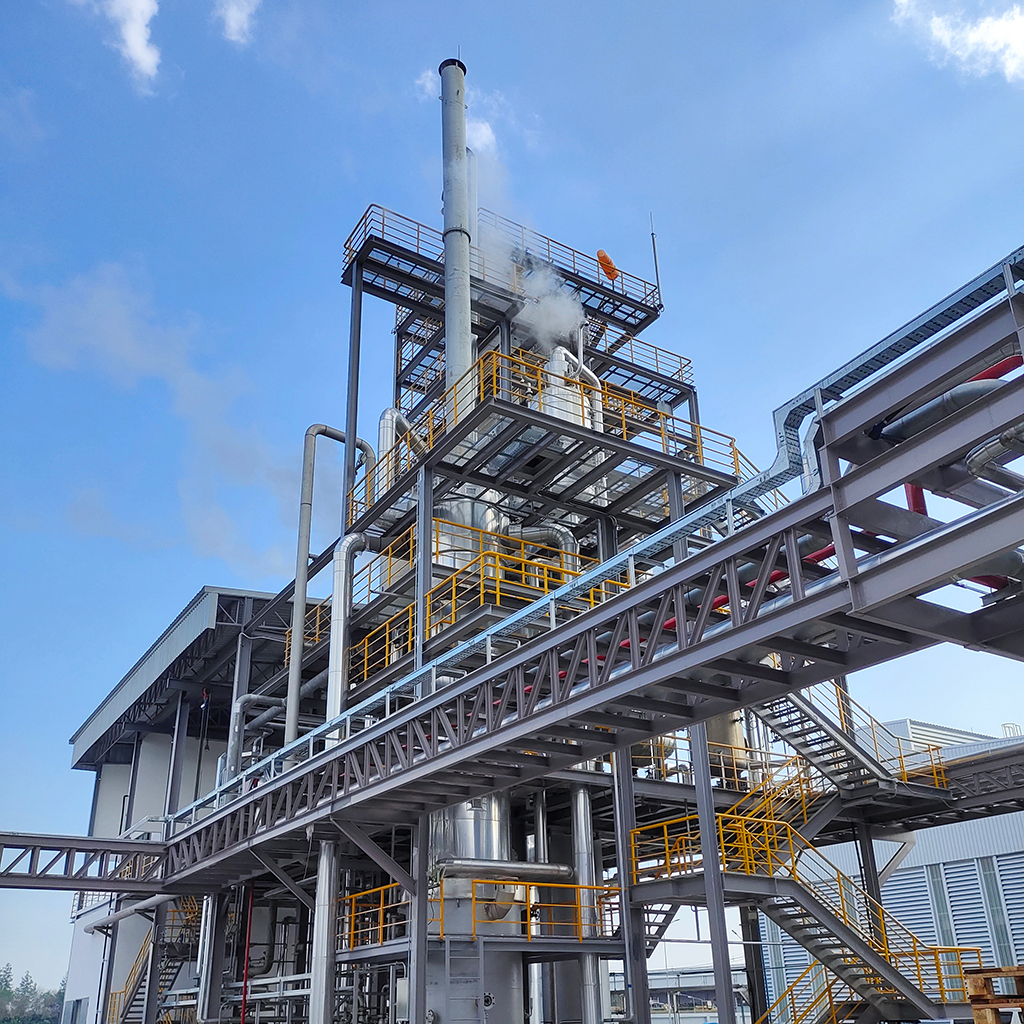
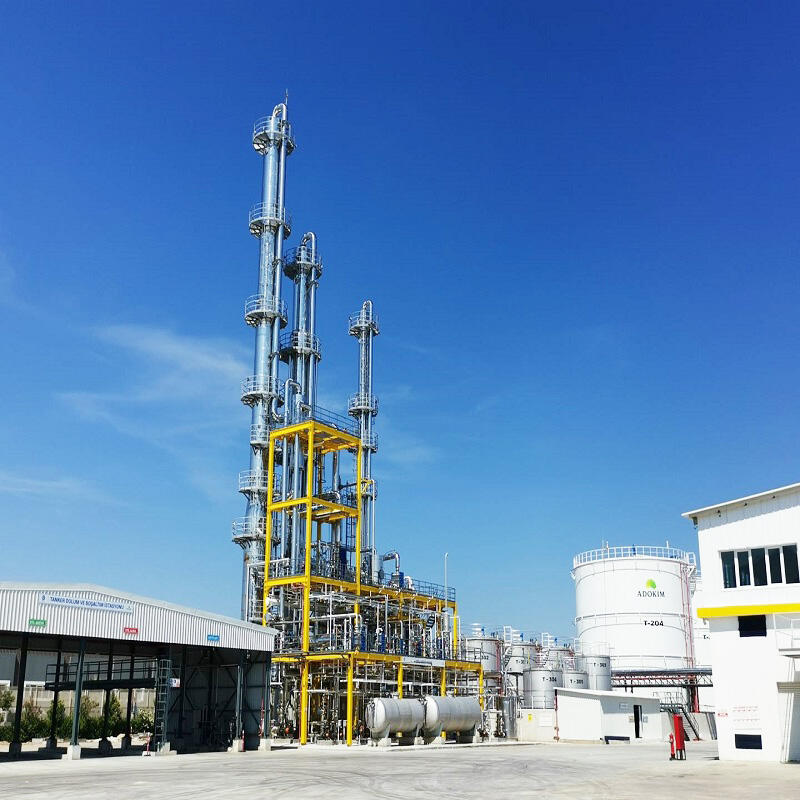
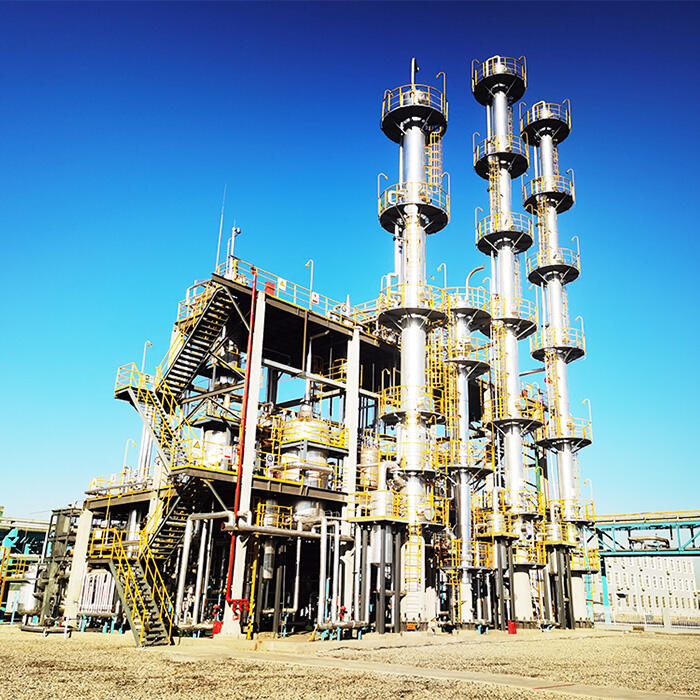
The company provides various types of towers and internals with rich materials including special alloys, ceramics, graphite, plastics, and stainless steel. For liquid distributors, there are Liquid Orifice Distributors, Liquid Trough Distributors, Liquid Ladder Distributors, and Liquid Spray Nozzle Distributors. It also offers gas distributors like Gas Distributor Spargers, packing supports, bed limiters, and mist eliminators such as Mesh Mist Eliminators and Chevron / Vane Type Mist Eliminators.

Related Articles

Outburst Of Demand On Carbon Fiber

03

Dec

Outburst Of Demand On Carbon Fiber

View More
Uses and Safety Precautions of Formaldehyde in Industry

23

Jul

Uses and Safety Precautions of Formaldehyde in Industry

Explore the industrial applications, safety measures, regulatory frameworks, and innovation trends of formaldehyde. Discover its role in resin production, healthcare disinfectants, wood composites, and alternatives like bio-based adhesives and low-VOC resins.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More

Customer Reviews

David Miller

Along with the equipment, the company provides excellent technical support. Their engineers are knowledgeable and can quickly solve any problems we encounter during installation or operation. They also offer valuable advice on equipment selection and usage.

Sarah Davis

The manufacturing quality of the chemical industrial equipment is outstanding. The equipment is precisely made, and the attention to detail is evident. The non - metallic pumps we purchased have excellent corrosion resistance, which is crucial for our chemical processing.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.