
chemical industrial container pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
High-Capacity Chemical Industrial Equipment Supply for Large-Scale Plants

High-Capacity Chemical Industrial Equipment Supply for Large-Scale Plants

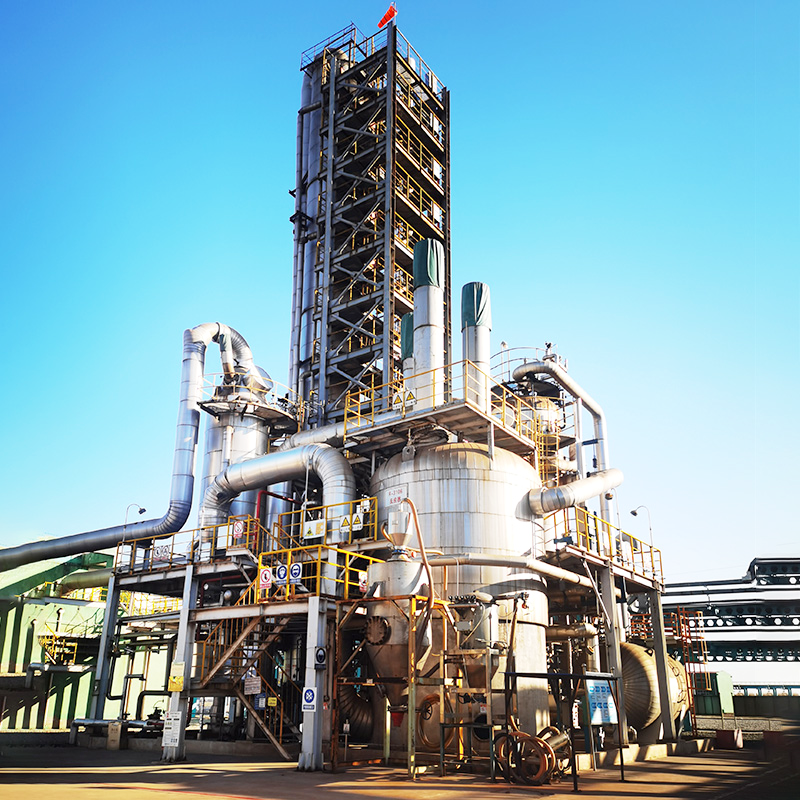
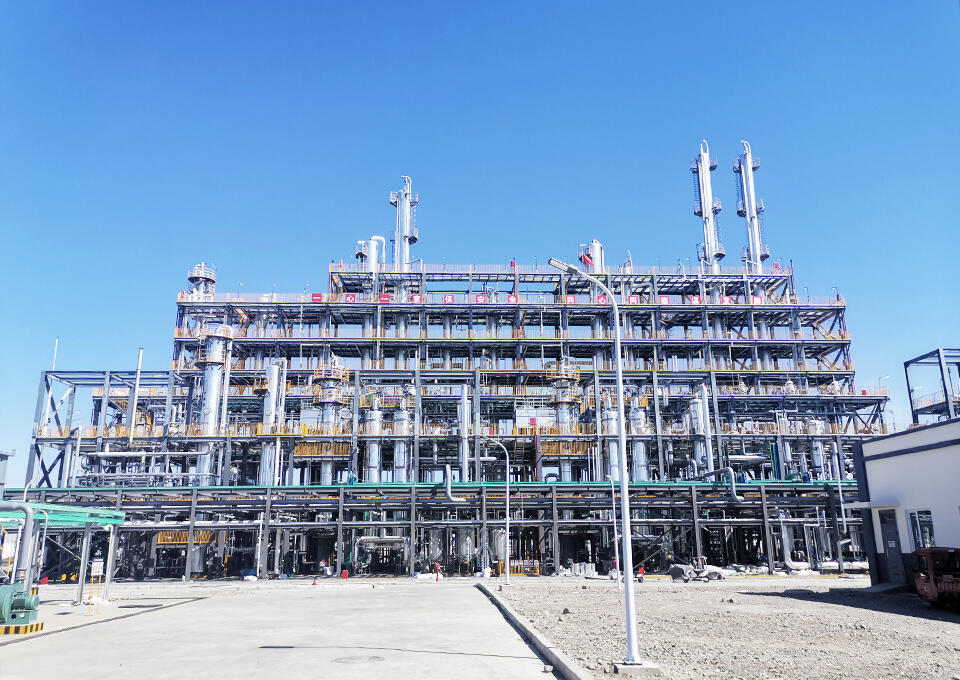
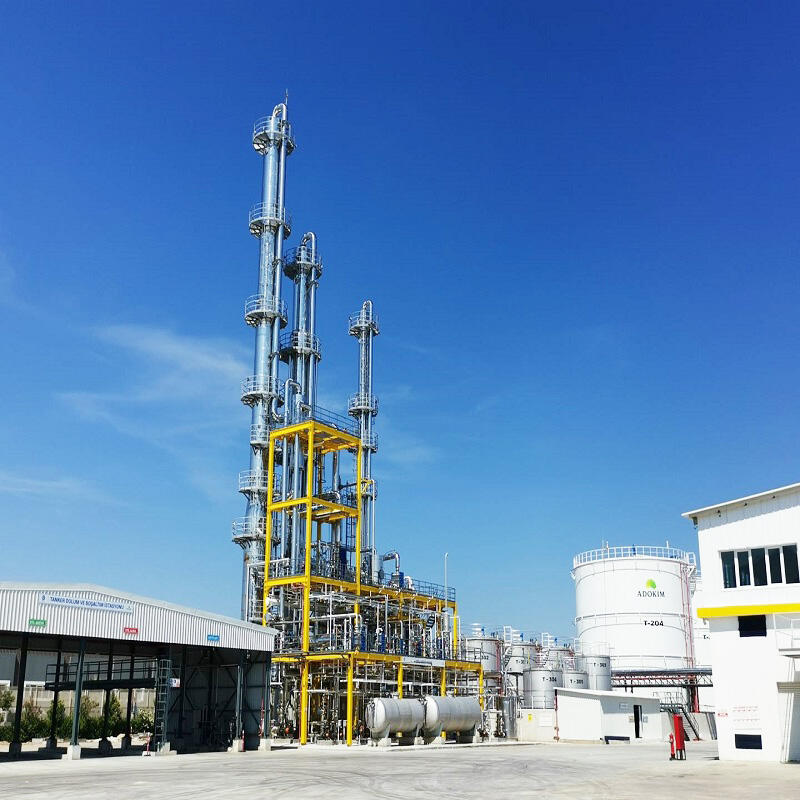
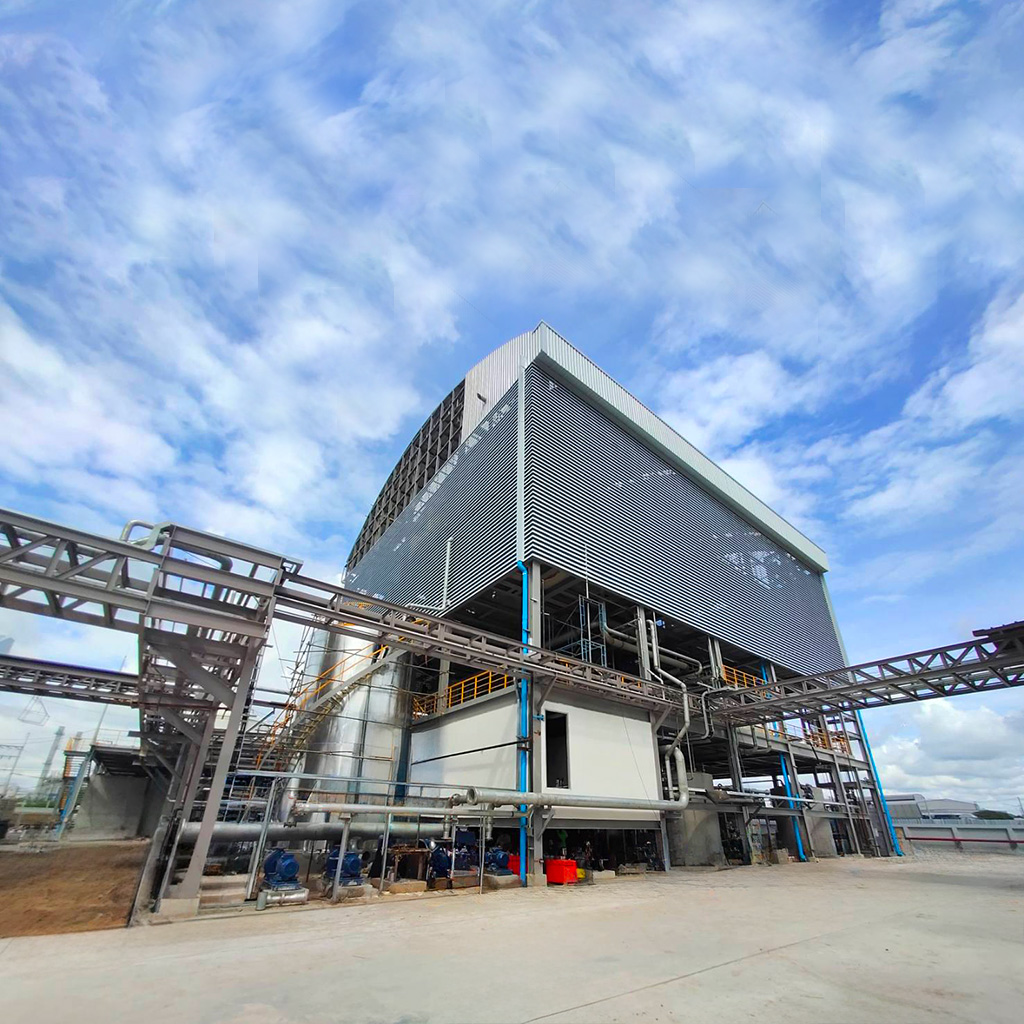
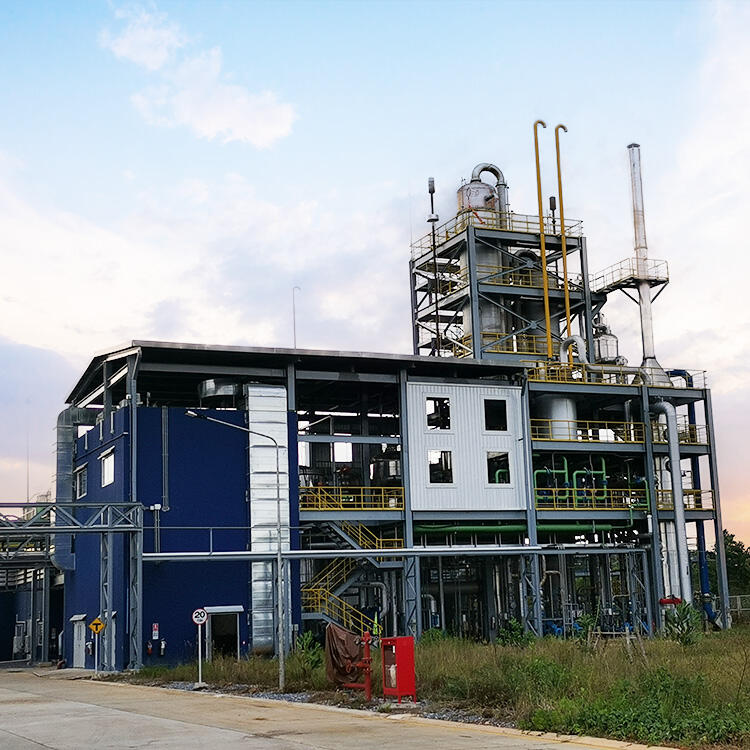
For large-scale chemical plants, we provide high-capacity chemical industrial equipment supply. Our pumps and skid-mounted systems are capable of handling high volumes of chemicals, ensuring uninterrupted production. With our robust equipment, you can meet your production targets and scale up your operations efficiently.
Get A Quote

Why choose us?

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

Chemical industrial equipment supply is a vital component in the success of chemical manufacturing operations. Changzhou Sanli Tech International Trade Co., Ltd. specializes in providing a comprehensive range of industrial equipment that meets the rigorous demands of the chemical sector. Our equipment is crafted from top-tier materials, ensuring durability and resistance to various chemicals, including corrosive substances, solvents, and high-viscosity fluids. For instance, our range of centrifugal pumps, both vertical and horizontal, are engineered to handle high-flow applications, making them ideal for large-scale chemical processing. A client in the water treatment industry required a pump that could handle high volumes of water with minimal energy consumption. We provided them with our energy-efficient centrifugal pumps, which not only met their flow requirements but also reduced their operational costs. In addition to standard pumps, we offer custom skid-mounted systems that can be tailored to specific process needs. These systems integrate multiple components, such as pumps, valves, and instrumentation, into a single, compact unit, reducing installation time and costs. A recent project involved designing a skid-mounted system for a chemical blending and storage application. The system included multiple pumps, a mixing tank, and an automated control system, allowing the client to blend and store chemicals efficiently and safely. Our chemical industrial equipment supply is backed by a team of experts who provide comprehensive support, ensuring our clients achieve the best possible outcomes.
Frequently Asked Questions

What advantages does the company have in the ethylene field?

It has in - depth research and practical experience in ethylene production technologies, including traditional tubular furnace cracking and emerging catalytic cracking. It offers one - stop services from process package design to equipment procurement and installation for ethylene production plant construction. For existing plants, it provides technical renovation services to improve yield and efficiency, and supports downstream product development.
It uses big data analysis to collect, analyze, and mine production data for process optimization, fault prediction, and quality improvement. Artificial intelligence algorithms enable intelligent control of production parameters. IoT technology allows remote monitoring and management of equipment, enabling engineers to check status, receive alarms, and perform operations remotely.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Analysis On Production Technology And Industrial Chain Of FM

28

Nov

Analysis On Production Technology And Industrial Chain Of FM

View More
Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

Amanda Anderson

We have complete trust in this company as a chemical industrial equipment supplier. They have a good reputation in the industry, and their products have consistently performed well. We plan to continue our long - term cooperation with them.

Emily Johnson

We've been sourcing chemical industrial equipment from this company for years. Their products always meet our strict standards. The custom - made skid - mounted equipment has simplified our installation process and reduced costs. Their after - sales service is also excellent.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.