
chemical industrial equipment supply for coating production|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Precision-Engineered Chemical Industrial Equipment Supply

Precision-Engineered Chemical Industrial Equipment Supply

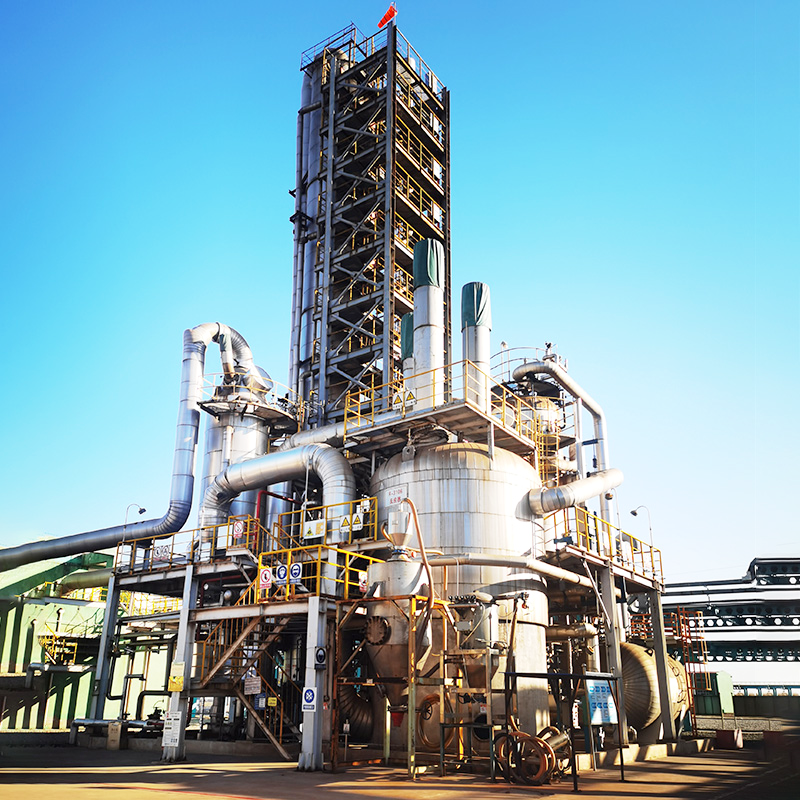
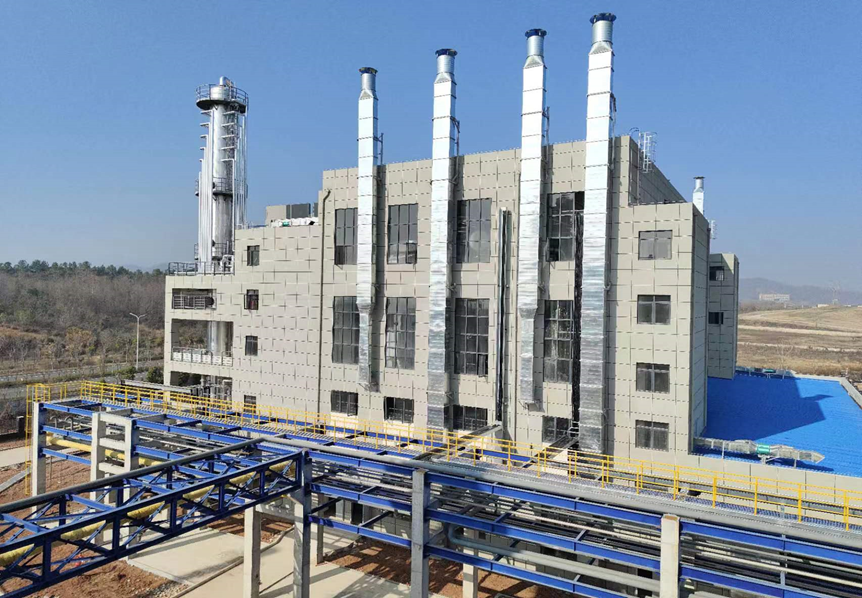
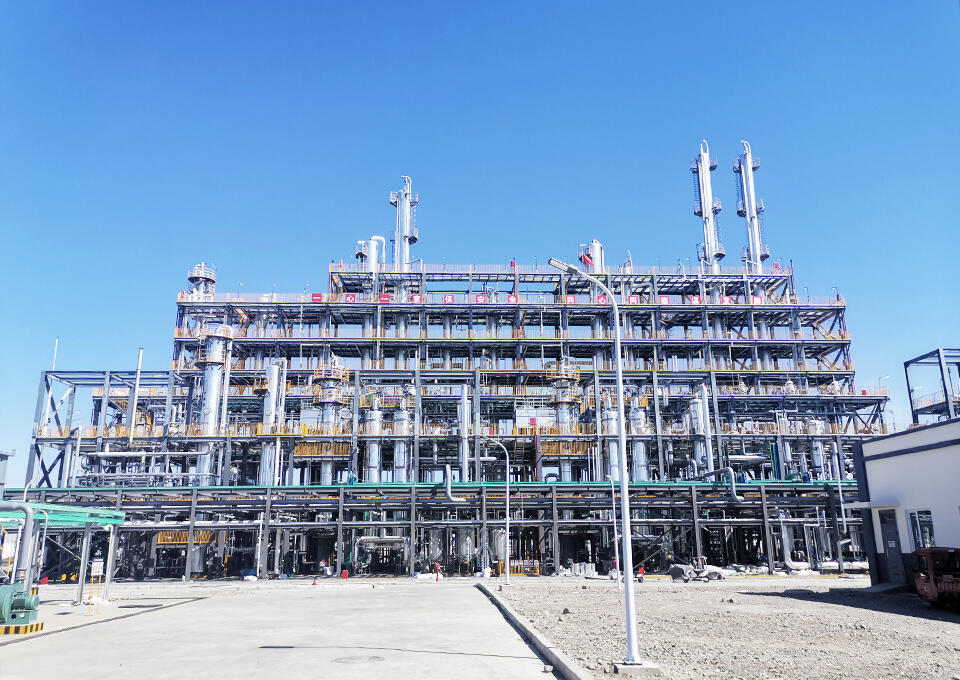
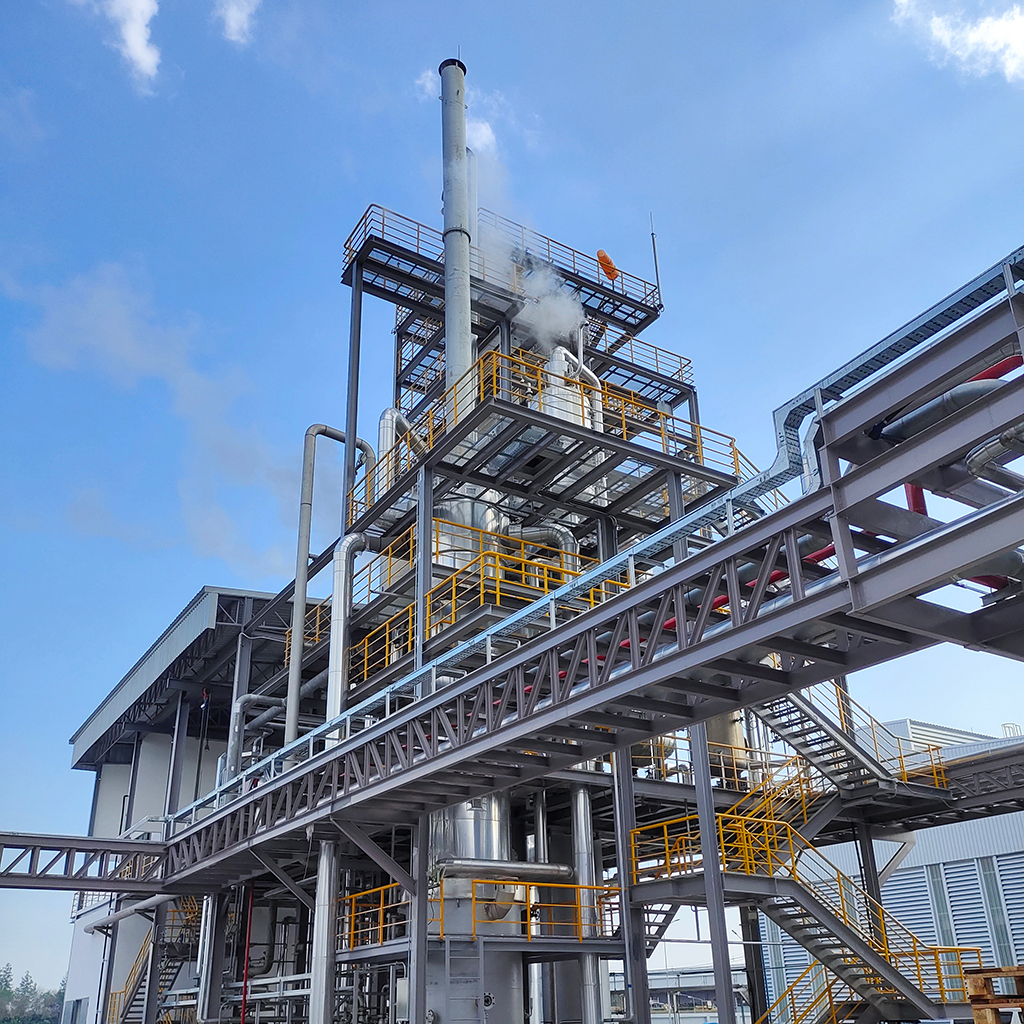
We take precision engineering seriously in chemical industrial equipment supply. Our products, from pumps to skid-mounted assemblies, are meticulously designed and manufactured to exact specifications. This precision ensures optimal performance, reliability, and compatibility with your existing chemical production systems.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

Related products

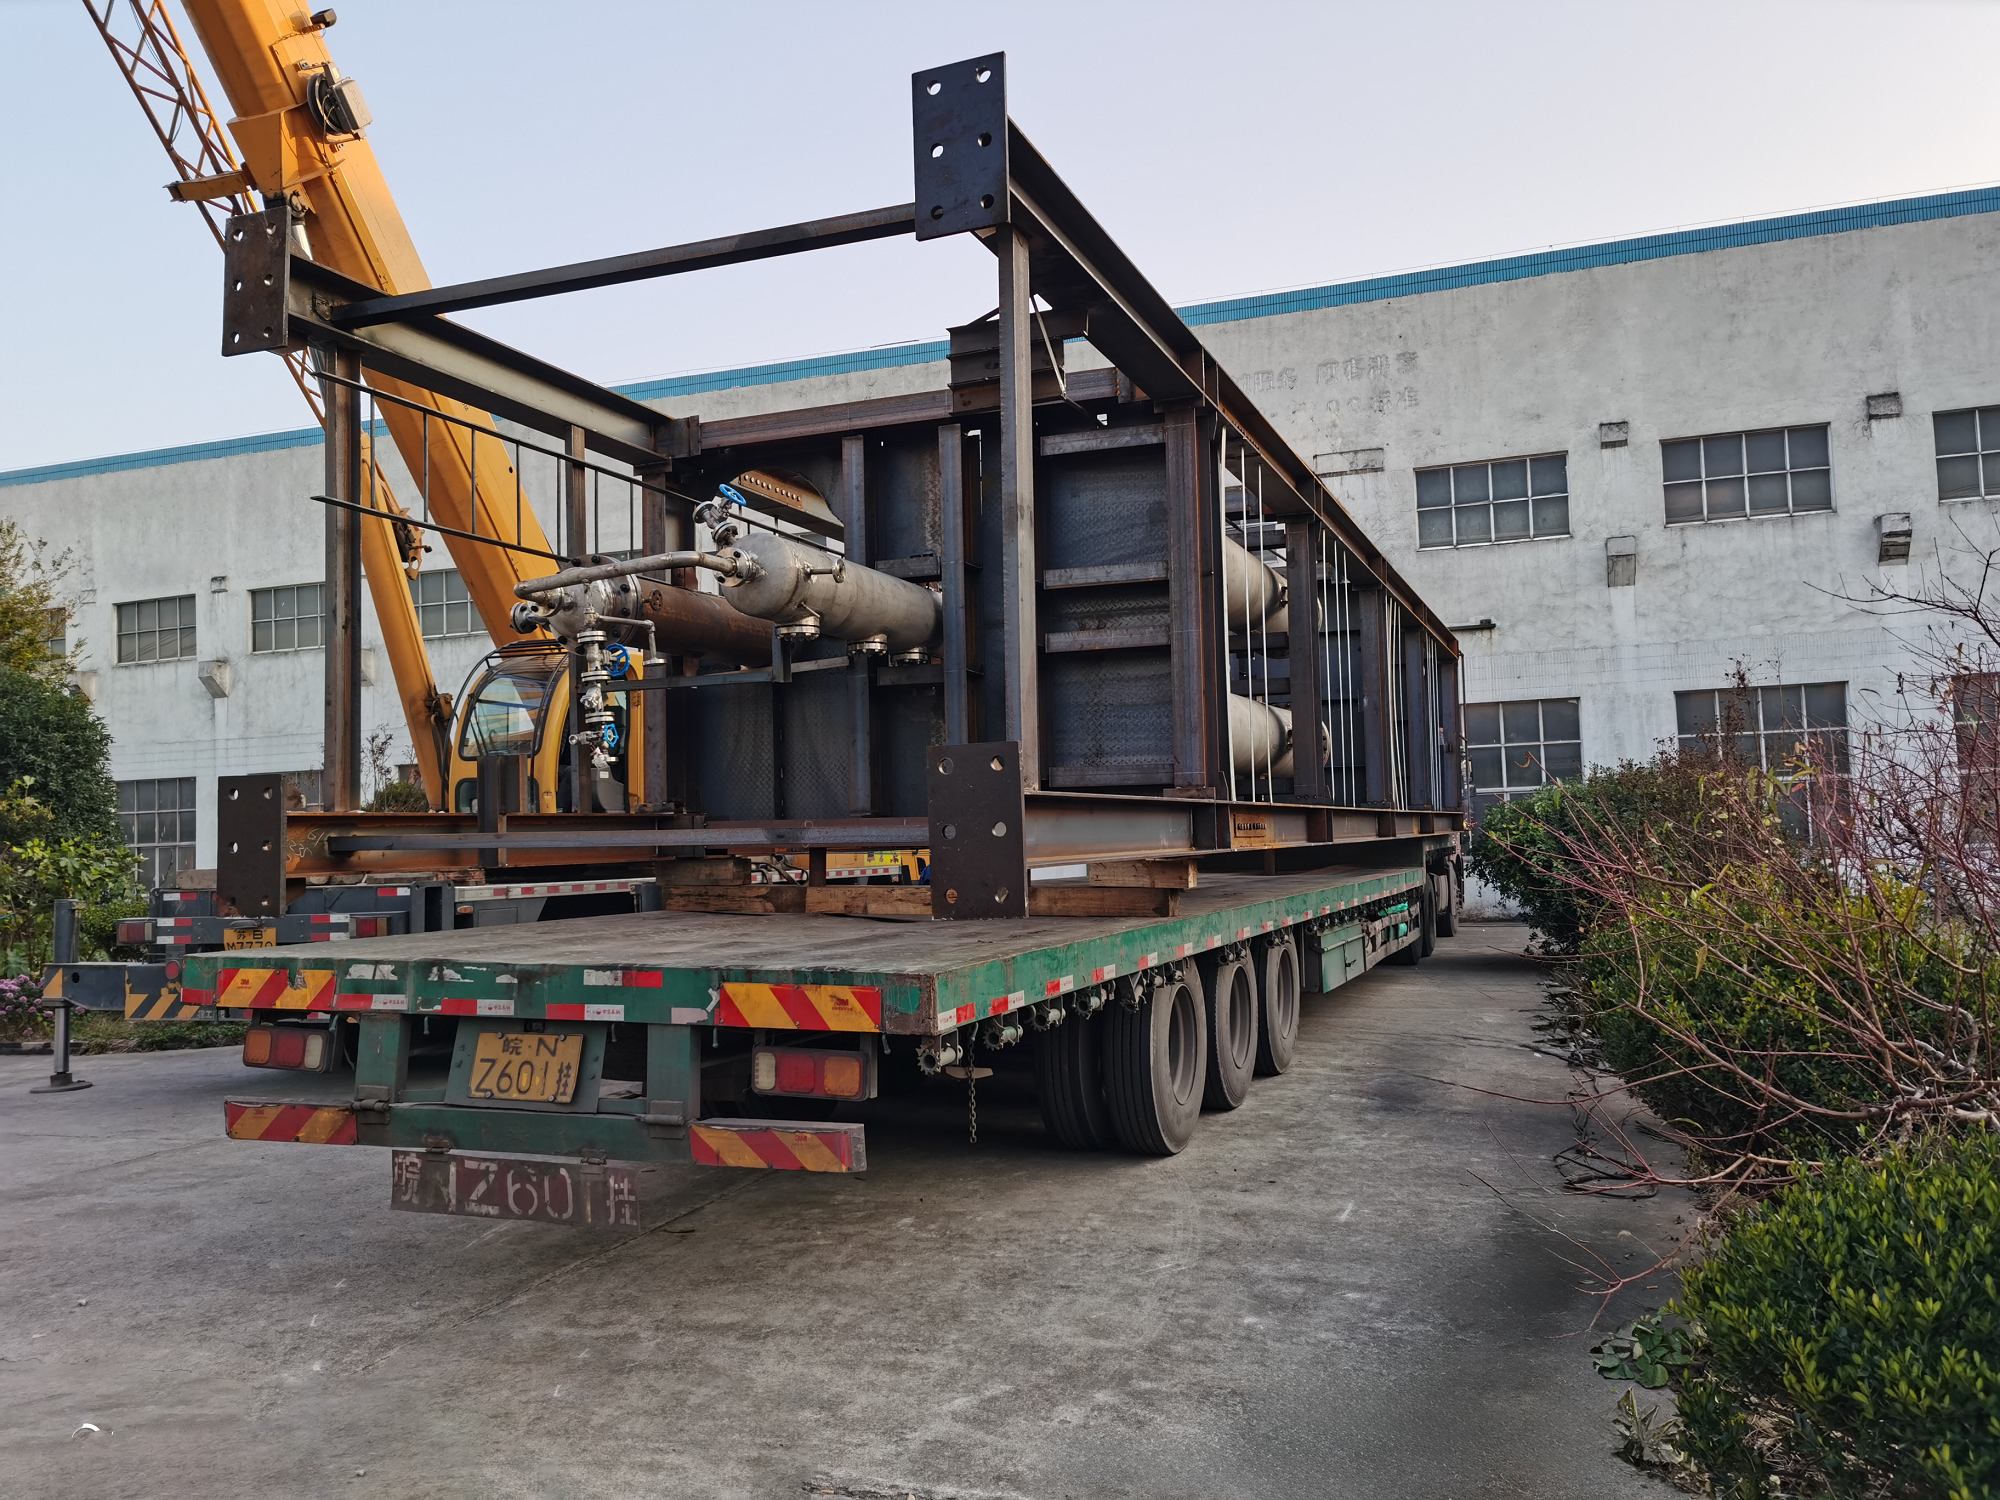
The field of chemical industrial equipment supply is constantly evolving, driven by the need for more efficient and sustainable chemical processes. Changzhou Sanli Tech International Trade Co., Ltd. is at the forefront of this evolution, offering innovative equipment that enhances the performance and environmental footprint of chemical manufacturing. Our product range includes a variety of pumps, such as canned motor pumps and vertical inline pumps, which are designed for applications requiring high efficiency and low maintenance. For example, our canned motor pumps are hermetically sealed, eliminating the need for mechanical seals and reducing the risk of leaks, making them ideal for handling hazardous chemicals. A client in the chemical processing industry needed a pump that could safely transfer corrosive chemicals without the risk of environmental contamination. We supplied them with our canned motor pumps, which provided a safe and reliable solution, ensuring the protection of their personnel and the environment. In addition to pumps, we offer skid-mounted systems that integrate multiple components into a single, compact unit, reducing installation time and costs. These systems can be customized to include various pumps, valves, and control systems, all designed to work seamlessly together. A recent project involved supplying a skid-mounted system for a chemical storage and transfer application. The system included a pump, flow meter, and control valve, all pre-assembled and tested, ensuring a seamless integration into the client's existing infrastructure. Our chemical industrial equipment supply is supported by a commitment to sustainability and customer satisfaction, ensuring our clients receive the best possible products and support.
Frequently Asked Questions

What personnel training courses does the company provide for chemical plants?

For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.
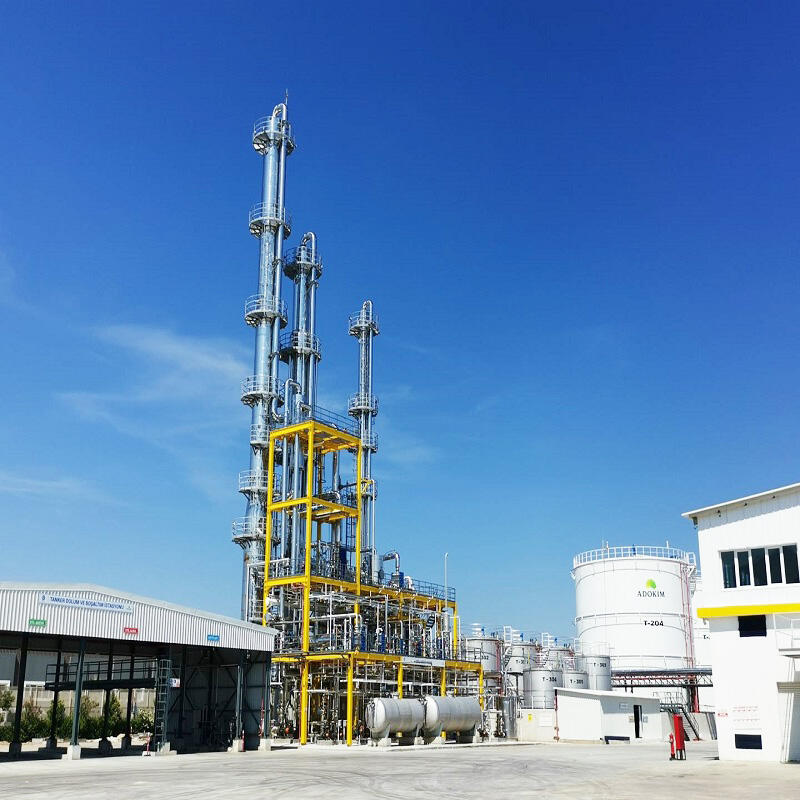
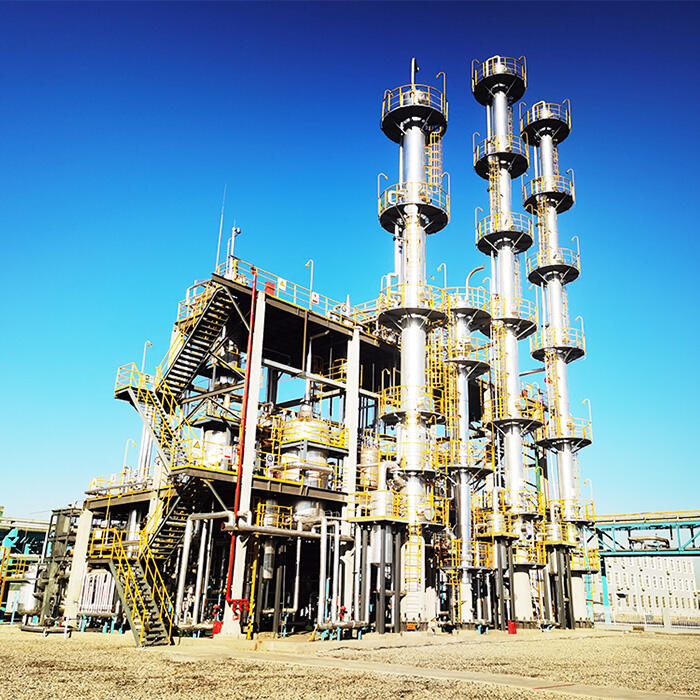
The company provides various types of towers and internals with rich materials including special alloys, ceramics, graphite, plastics, and stainless steel. For liquid distributors, there are Liquid Orifice Distributors, Liquid Trough Distributors, Liquid Ladder Distributors, and Liquid Spray Nozzle Distributors. It also offers gas distributors like Gas Distributor Spargers, packing supports, bed limiters, and mist eliminators such as Mesh Mist Eliminators and Chevron / Vane Type Mist Eliminators.

Related Articles

Outburst Of Demand On Carbon Fiber

03

Dec

Outburst Of Demand On Carbon Fiber

View More
Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More

Customer Reviews

Lisa Garcia

The chemical industrial equipment we bought from this company has proven to be very durable. It has been exposed to various chemicals and harsh operating conditions, but it still functions well. This long - lasting performance has reduced our equipment replacement costs.

David Miller

Along with the equipment, the company provides excellent technical support. Their engineers are knowledgeable and can quickly solve any problems we encounter during installation or operation. They also offer valuable advice on equipment selection and usage.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.