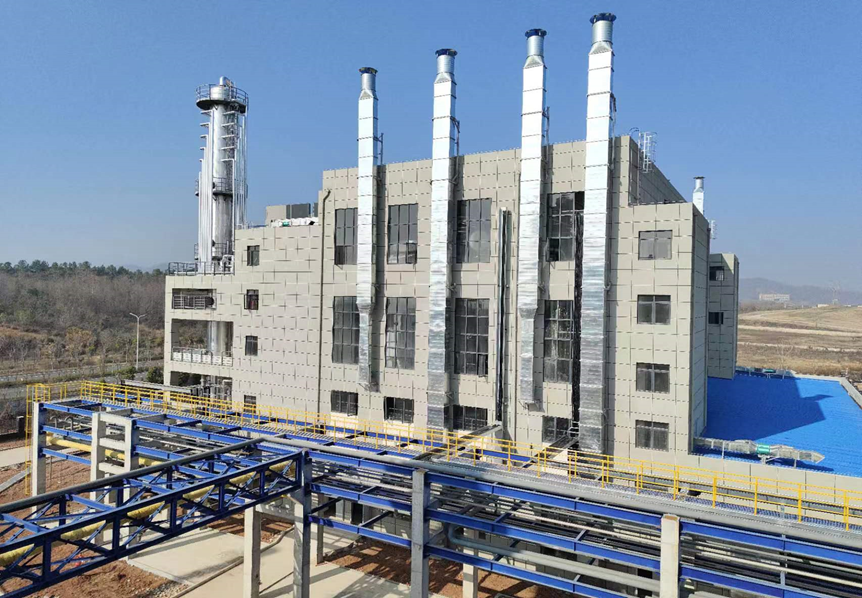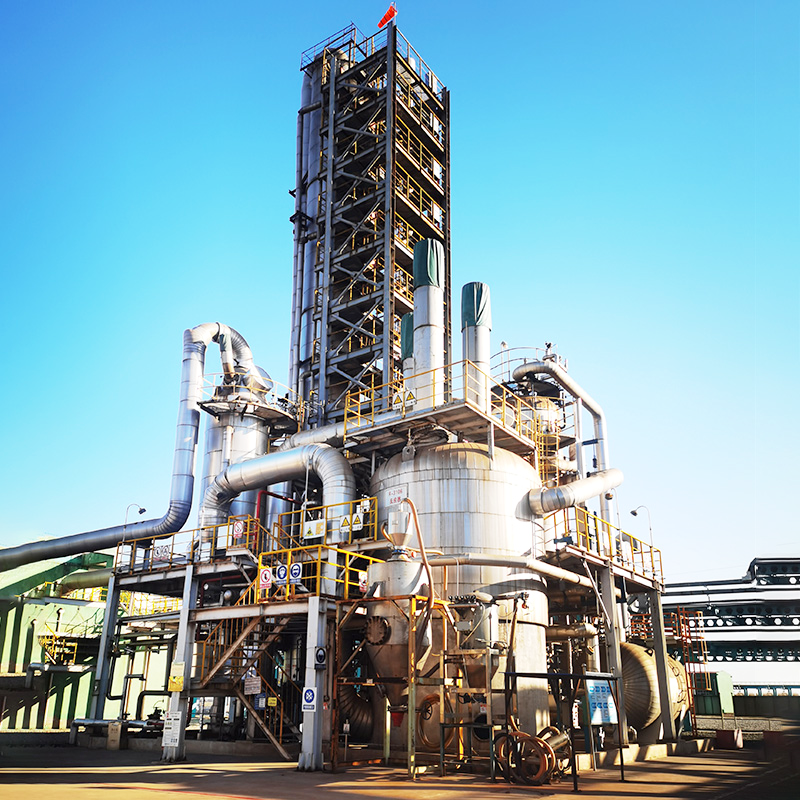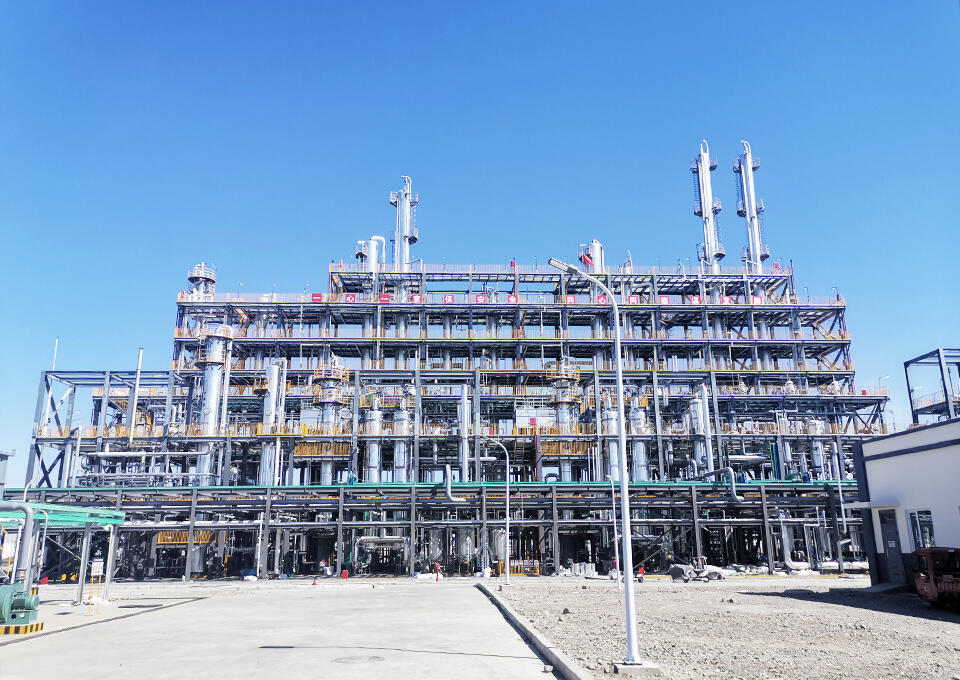

chemical industrial equipment supply with easy installation|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Cost-Effective Chemical Industrial Equipment Supply Options

Cost-Effective Chemical Industrial Equipment Supply Options

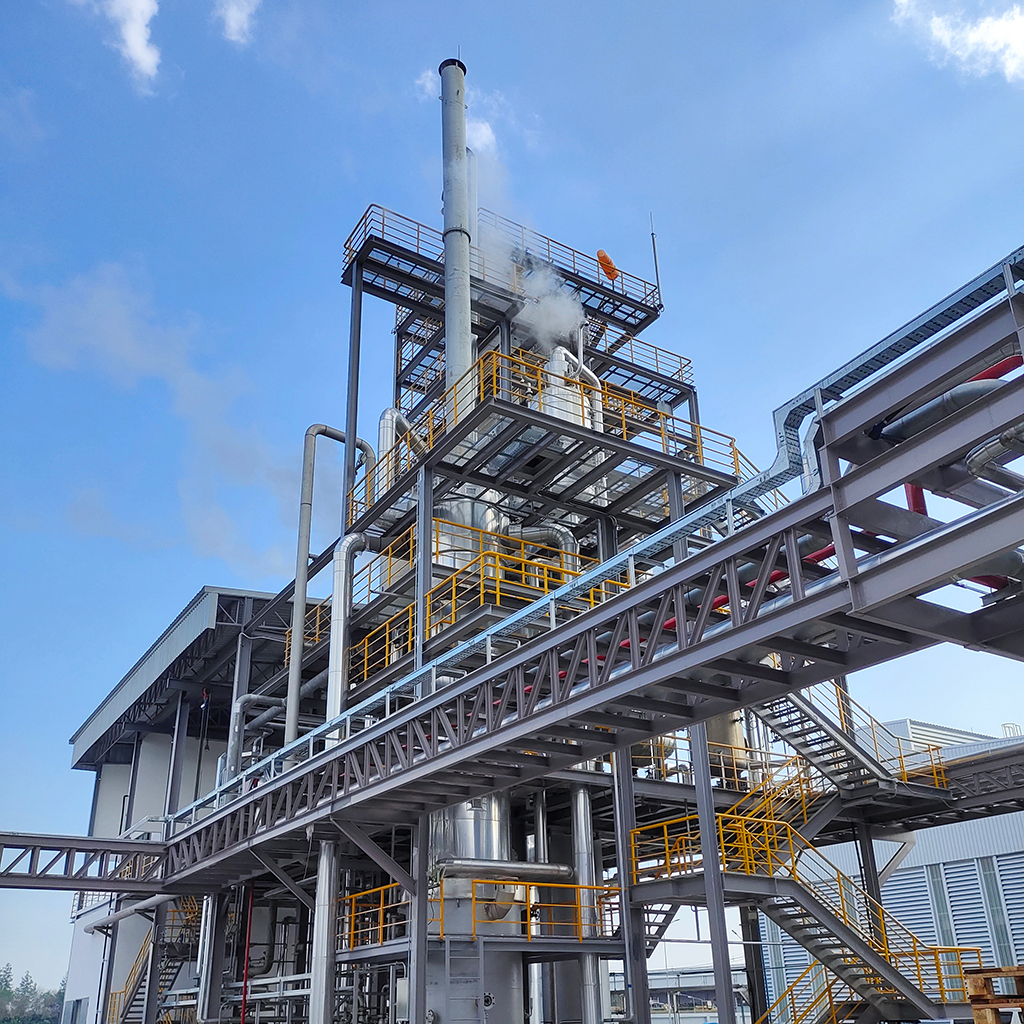
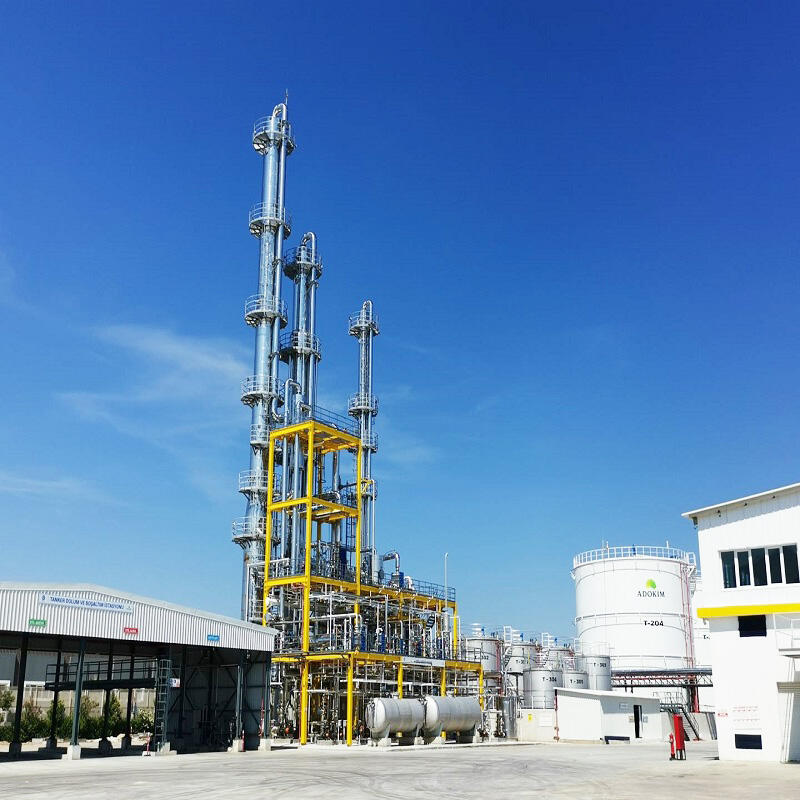
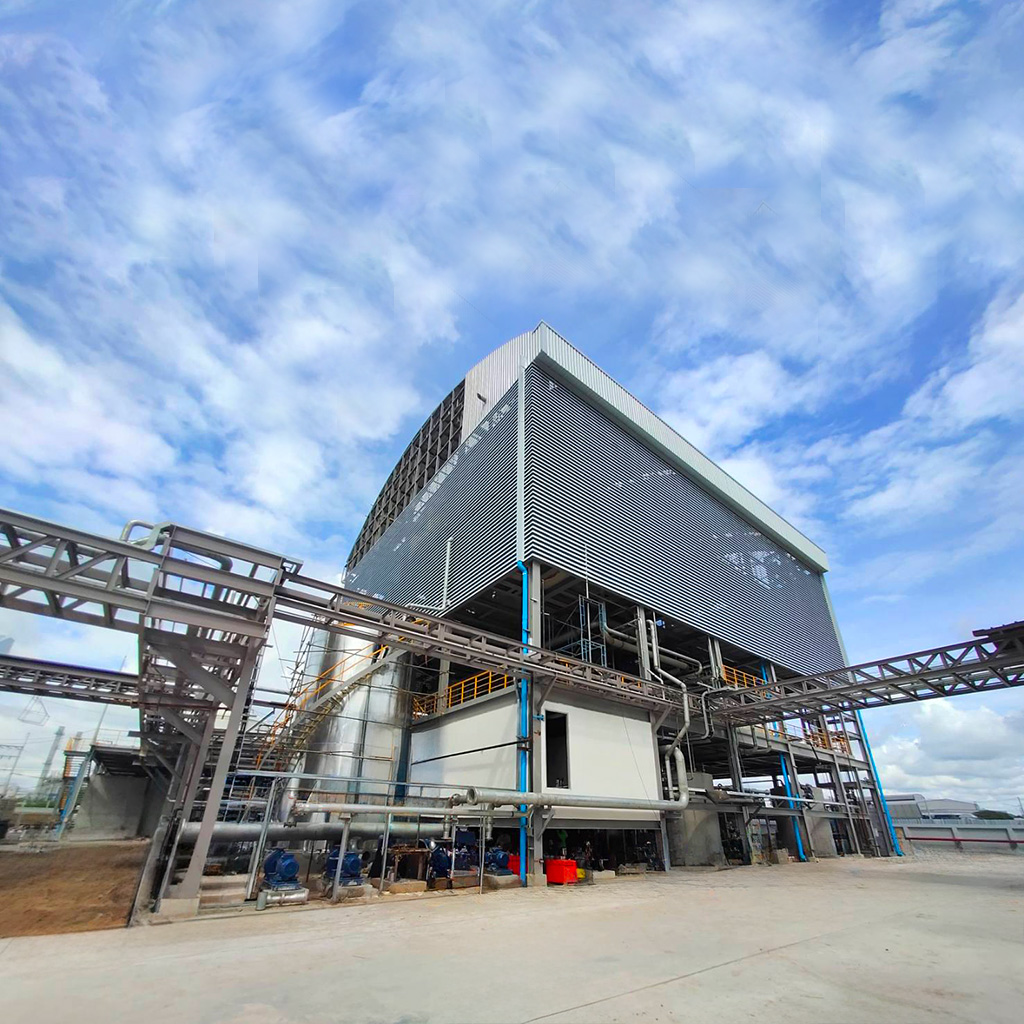
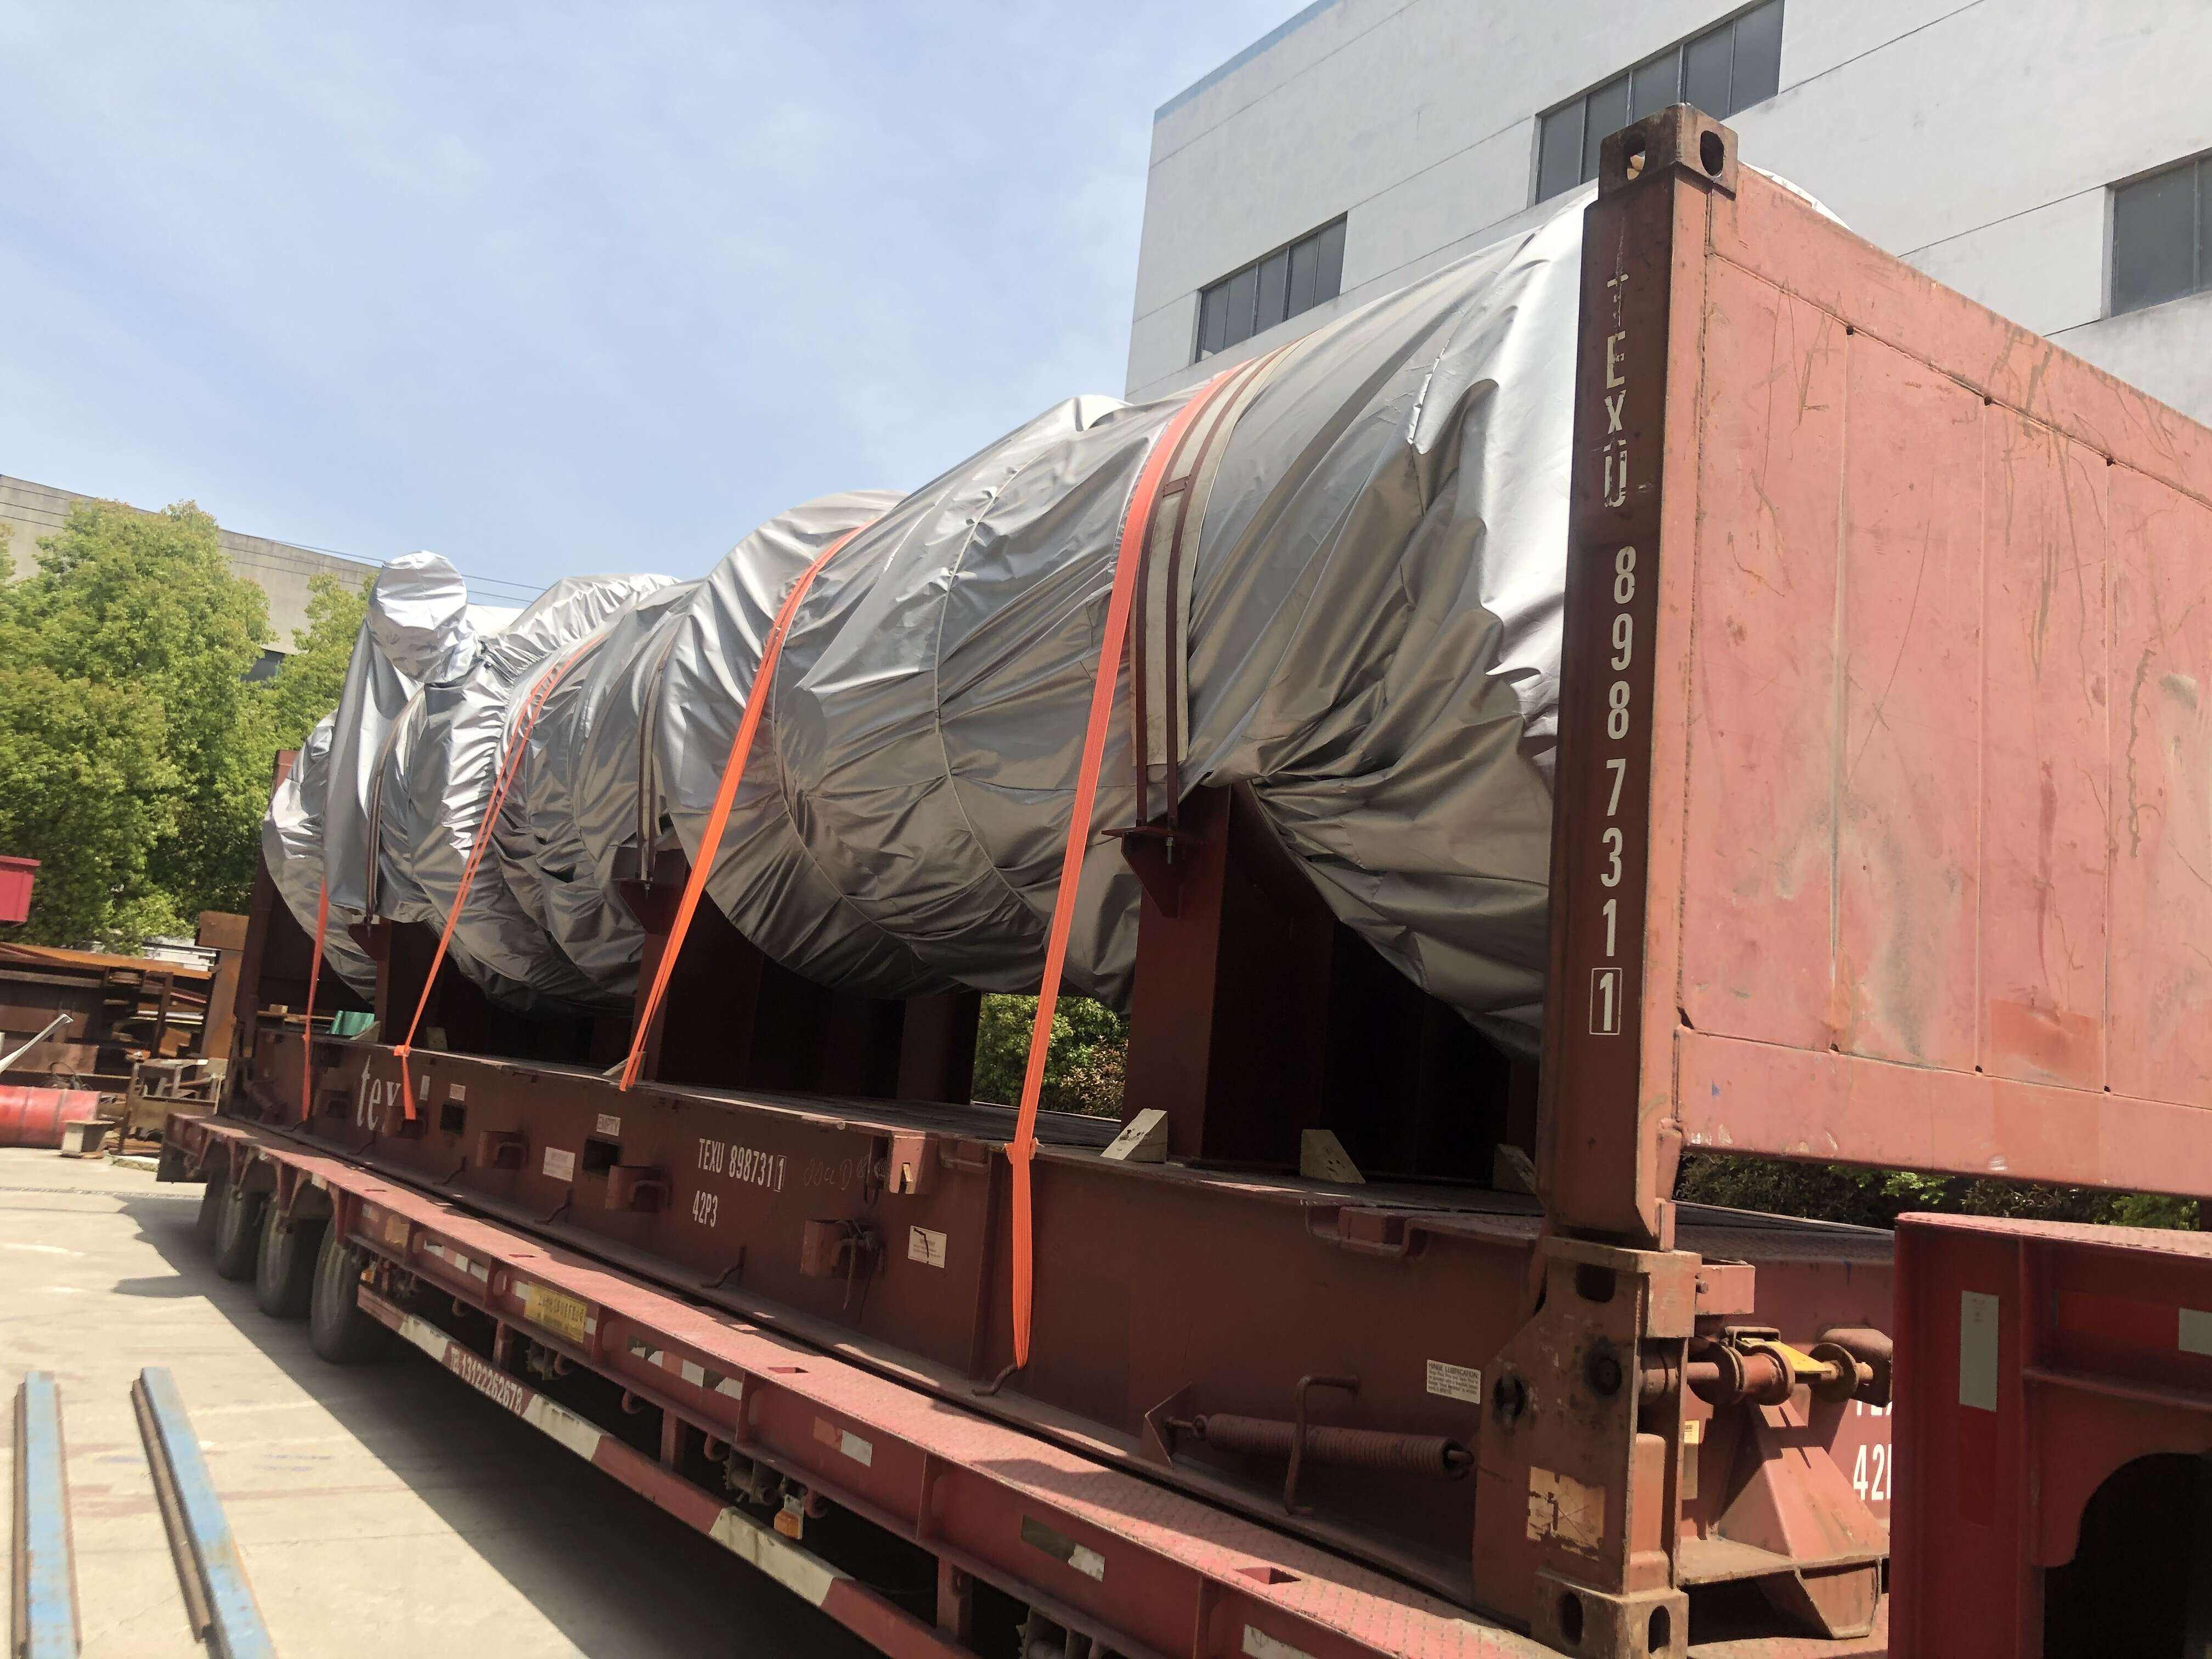
Looking for cost-effective chemical industrial equipment supply? Look no further. We provide a range of affordable yet high-quality products. Our pumps and skid-mounted equipment are designed to offer great value for money, helping you save on initial investment and long-term operating costs in your chemical facility.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

The field of chemical industrial equipment supply is constantly evolving, driven by the need for more efficient and sustainable chemical processes. Changzhou Sanli Tech International Trade Co., Ltd. is at the forefront of this evolution, offering innovative equipment that enhances the performance and environmental footprint of chemical manufacturing. Our product range includes a variety of pumps, such as canned motor pumps and vertical inline pumps, which are designed for applications requiring high efficiency and low maintenance. For example, our canned motor pumps are hermetically sealed, eliminating the need for mechanical seals and reducing the risk of leaks, making them ideal for handling hazardous chemicals. A client in the chemical processing industry needed a pump that could safely transfer corrosive chemicals without the risk of environmental contamination. We supplied them with our canned motor pumps, which provided a safe and reliable solution, ensuring the protection of their personnel and the environment. In addition to pumps, we offer skid-mounted systems that integrate multiple components into a single, compact unit, reducing installation time and costs. These systems can be customized to include various pumps, valves, and control systems, all designed to work seamlessly together. A recent project involved supplying a skid-mounted system for a chemical storage and transfer application. The system included a pump, flow meter, and control valve, all pre-assembled and tested, ensuring a seamless integration into the client's existing infrastructure. Our chemical industrial equipment supply is supported by a commitment to sustainability and customer satisfaction, ensuring our clients receive the best possible products and support.
Frequently Asked Questions

What advantages does the company have in the ethylene field?

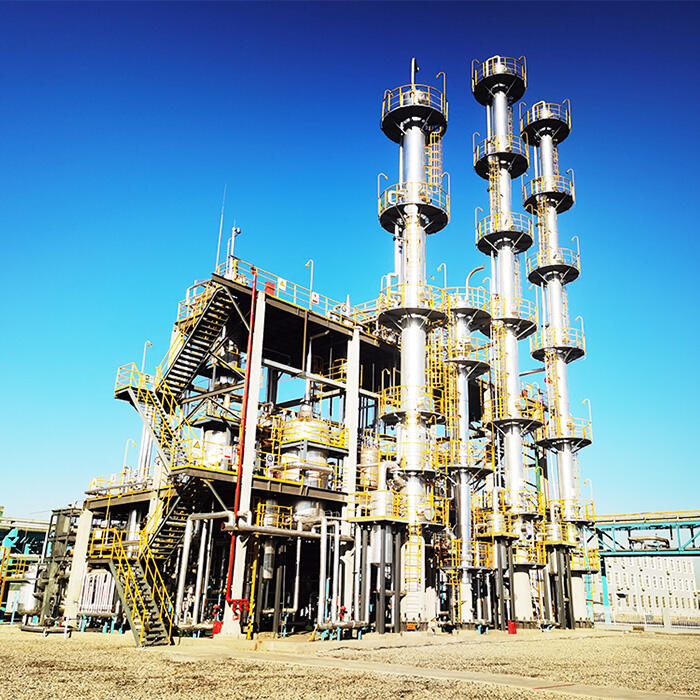
It has in - depth research and practical experience in ethylene production technologies, including traditional tubular furnace cracking and emerging catalytic cracking. It offers one - stop services from process package design to equipment procurement and installation for ethylene production plant construction. For existing plants, it provides technical renovation services to improve yield and efficiency, and supports downstream product development.
For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Outburst Of Demand On Carbon Fiber

03

Dec

Outburst Of Demand On Carbon Fiber

View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
The Role of Polymers in the Development of High - tech Industries

23

Jul

The Role of Polymers in the Development of High - tech Industries

Discover how polymer innovations are revolutionizing high-tech sectors, transforming manufacturing, sustainability, and technology applications. Explore the uses of photopolymers, high-performance polymers in aerospace, polyethylene glycol in drug delivery, and cutting-edge recycling methods for a greener future.
View More

Customer Reviews

Lisa Garcia

The chemical industrial equipment we bought from this company has proven to be very durable. It has been exposed to various chemicals and harsh operating conditions, but it still functions well. This long - lasting performance has reduced our equipment replacement costs.

John Smith

The chemical industrial equipment supplied by this company is of top - notch quality. The materials used are durable and can withstand harsh chemical environments. The pumps, for example, have been running smoothly in our plant for a long time without any major issues. Highly recommended!

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.