
non metallic chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Flexible Chemical Industrial Equipment Supply for Changing Needs

Flexible Chemical Industrial Equipment Supply for Changing Needs

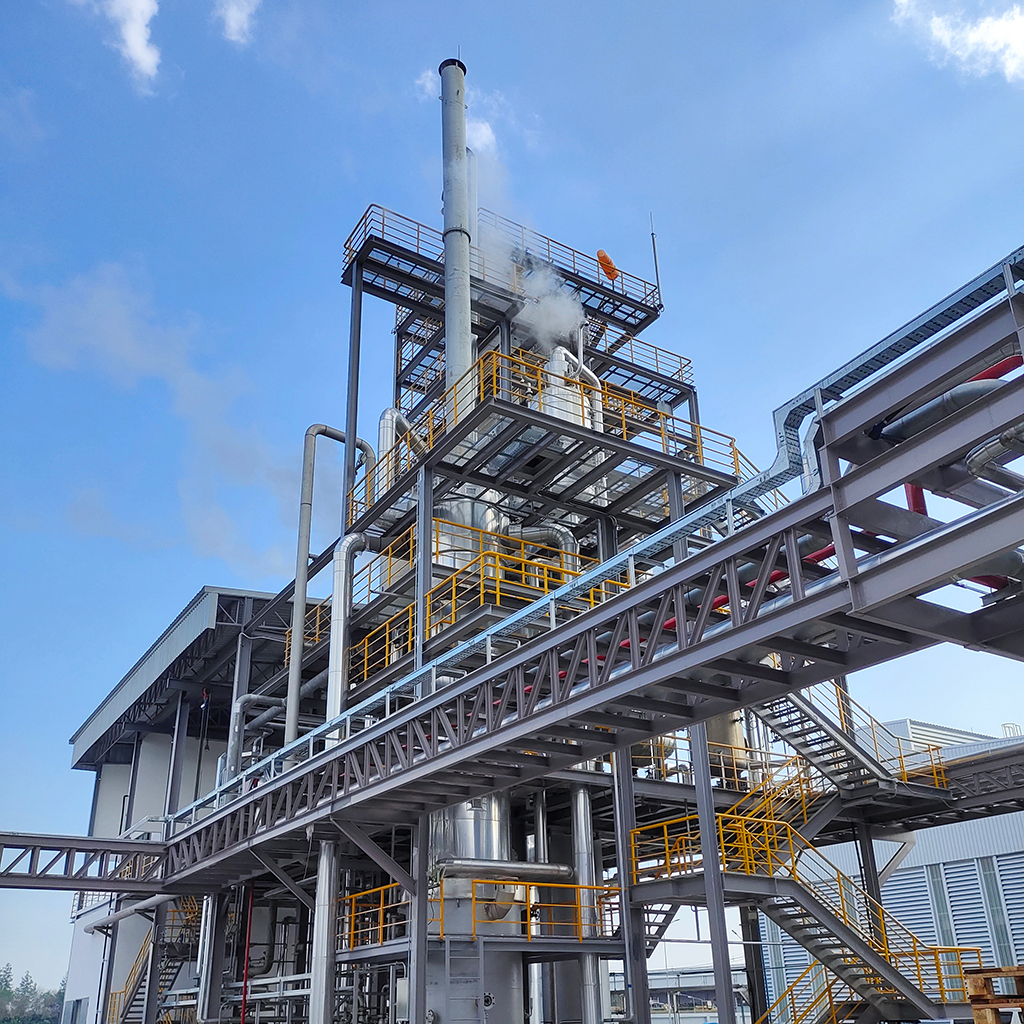
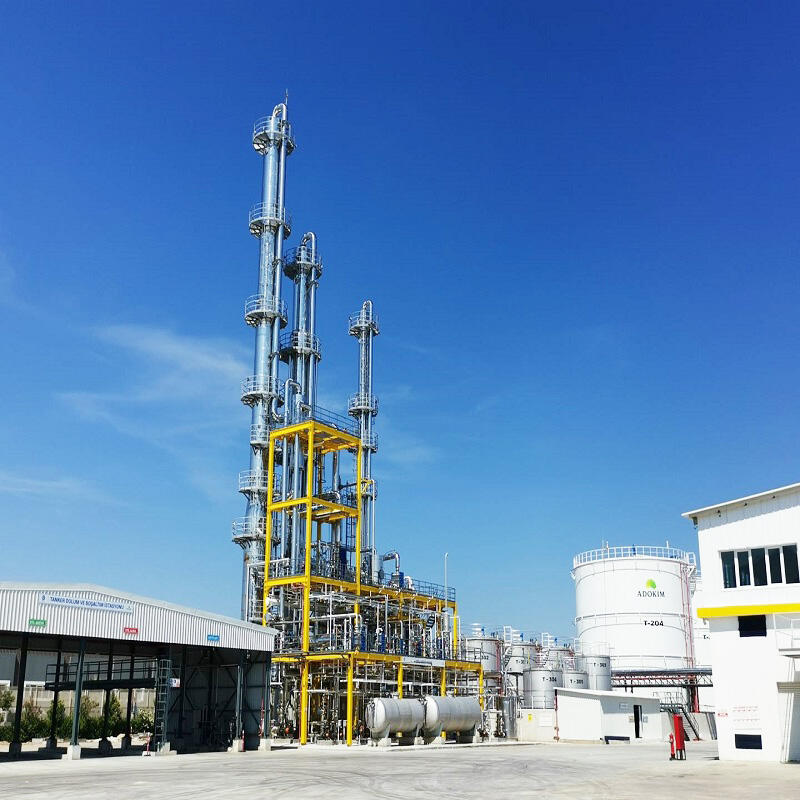
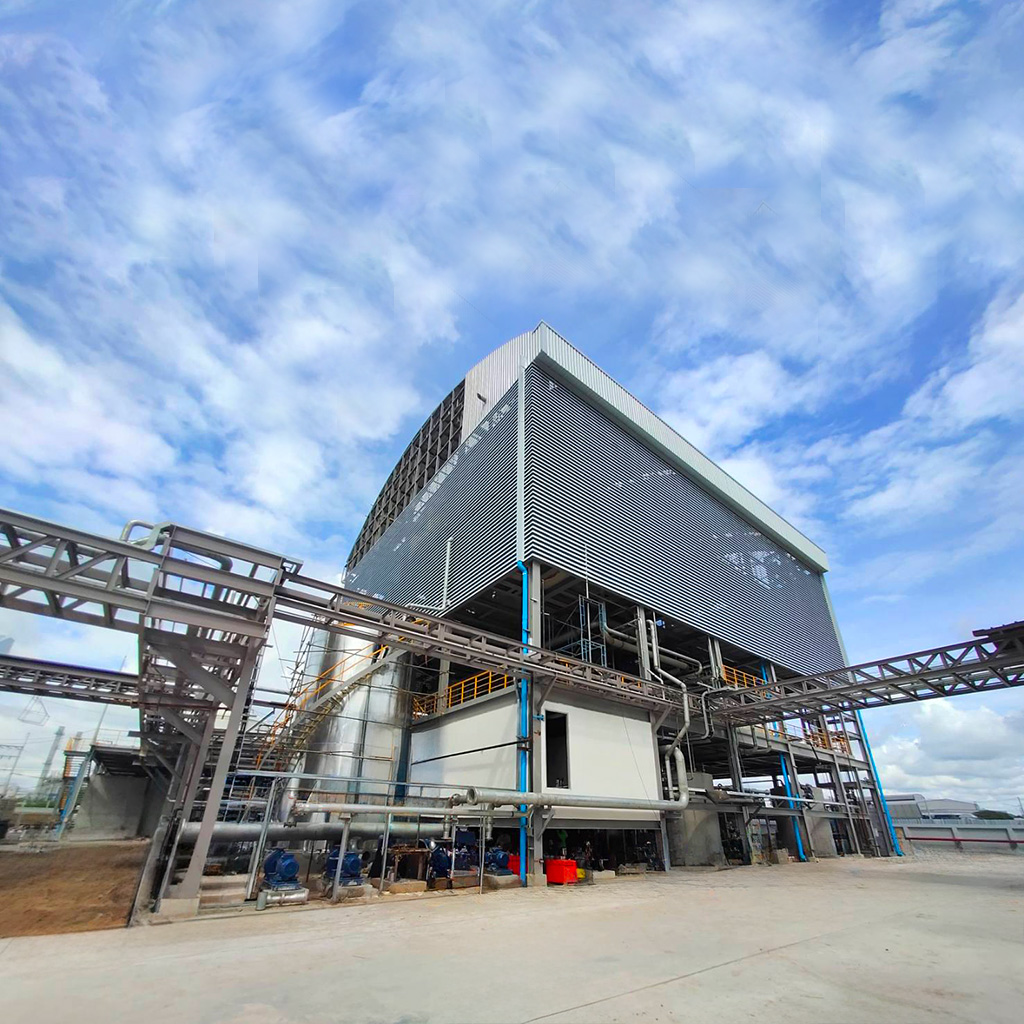
We offer flexible chemical industrial equipment supply to meet your changing needs. As your chemical production requirements evolve, we can quickly adapt and provide the right equipment. Whether you need to upgrade your pumps or expand your skid-mounted system, we are here to support you every step of the way.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

The field of chemical industrial equipment supply is characterized by a constant drive for innovation and efficiency. Changzhou Sanli Tech International Trade Co., Ltd. is at the forefront of this movement, offering cutting-edge equipment that enhances the performance and reliability of chemical processes. Our product range includes advanced pumps like peristaltic pumps and lobe pumps, which are designed for applications requiring gentle handling of chemicals or precise flow control. For example, our peristaltic pumps are widely used in the pharmaceutical industry for transferring sensitive chemicals without contamination, thanks to their tube-based design that eliminates the need for seals or valves. A pharmaceutical client recently needed a pump for their drug formulation process, where cross-contamination was a major concern. We supplied them with our peristaltic pumps, which provided a sterile and reliable solution, ensuring the integrity of their products. In addition to pumps, we also offer skid-mounted equipment that incorporates the latest technology for improved process control and monitoring. These skids can be equipped with sensors, actuators, and advanced control systems, allowing for real-time data collection and analysis. A client in the chemical processing industry implemented our skid-mounted system with integrated control, which enabled them to optimize their process parameters, reduce waste, and improve product quality. Our commitment to innovation and customer-centric approach ensures that our chemical industrial equipment supply meets the evolving needs of the industry, driving efficiency and productivity.
Frequently Asked Questions

What advantages does the company have in the ethylene field?

It has in - depth research and practical experience in ethylene production technologies, including traditional tubular furnace cracking and emerging catalytic cracking. It offers one - stop services from process package design to equipment procurement and installation for ethylene production plant construction. For existing plants, it provides technical renovation services to improve yield and efficiency, and supports downstream product development.
It can provide formaldehyde production process design and supporting equipment for efficient, safe, and stable production. It uses advanced catalyst and reaction condition control technology to improve yield and purity. It also has solutions for tail - gas treatment to meet environmental requirements. The supplied formaldehyde meets the needs of multiple industries like chemicals, building materials, and textiles.
It supplies a wide range of equipment for the chemical market. Pump types include barrel and container pumps, pneumatic diaphragm pumps, eccentric disc pumps, etc. Besides single pumps and fan components, it provides customized skid - mounted equipment for single - point connection and cost - reducing installation, complying with relevant API and ANSI standards.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Outburst Of Demand On Carbon Fiber

03

Dec

Outburst Of Demand On Carbon Fiber

View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
The Intersection of Chemistry and Engineering in Production Technology

23

Jul

The Intersection of Chemistry and Engineering in Production Technology

Explore the transformative role of chemical engineering in production technology, digital transformation in chemical manufacturing using AI and IoT, sustainable material innovations, and future trends in polymer manufacturing and nanotechnology. Understand the significance of optimizing processes for efficiency and sustainability.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

William Martinez

The design of the chemical industrial equipment makes it easy to maintain. The components are accessible, and the maintenance procedures are straightforward. This has saved us a lot of time and labor costs in the long run. We're very satisfied with the equipment.

Michael Brown

This company offers an extensive range of chemical industrial equipment. Whether it's pumps of different types or other related devices, we can find what we need here. The variety allows us to choose the most suitable equipment for our specific production requirements.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.