
peristaltic chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Cost-Effective Chemical Industrial Equipment Supply Options

Cost-Effective Chemical Industrial Equipment Supply Options

Looking for cost-effective chemical industrial equipment supply? Look no further. We provide a range of affordable yet high-quality products. Our pumps and skid-mounted equipment are designed to offer great value for money, helping you save on initial investment and long-term operating costs in your chemical facility.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

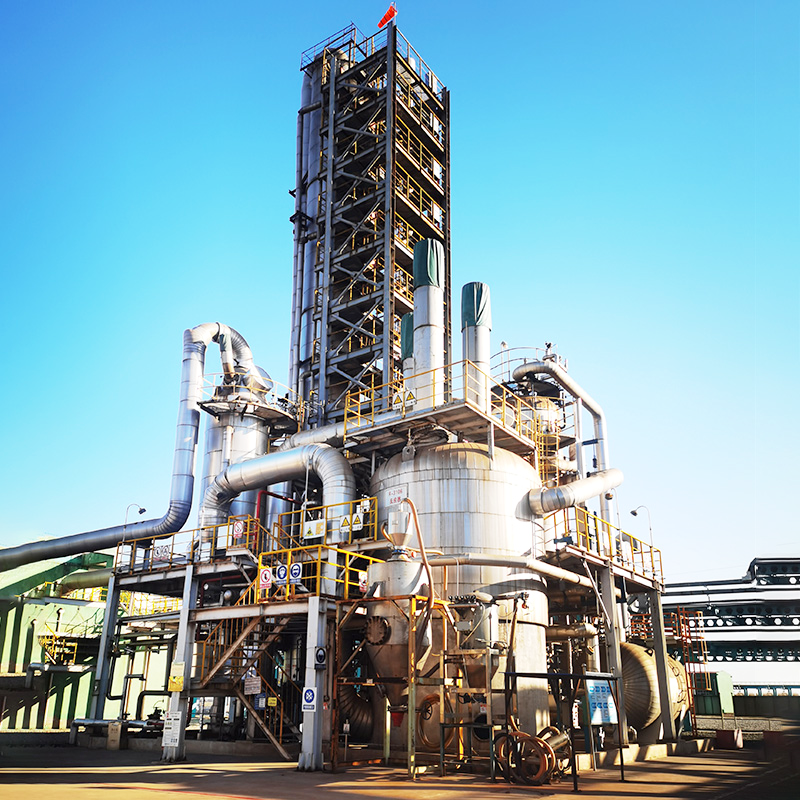
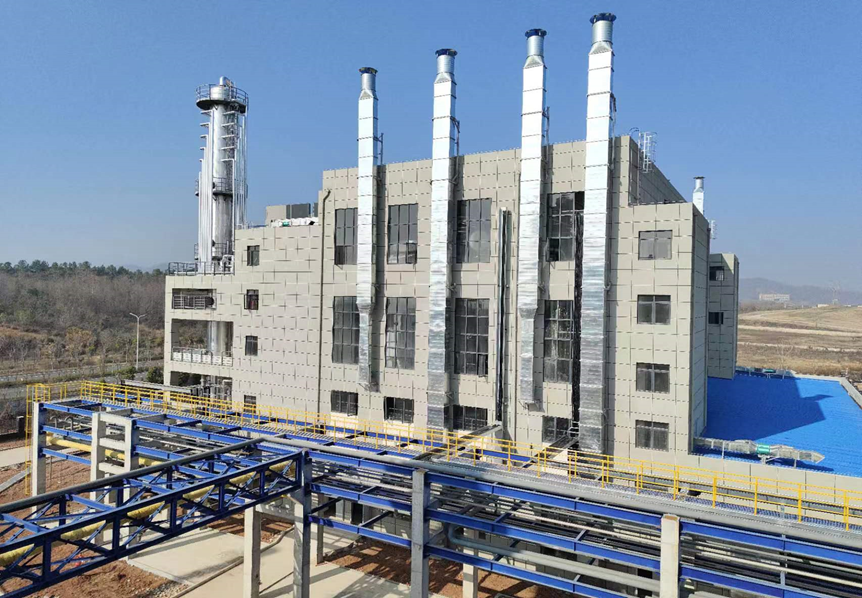
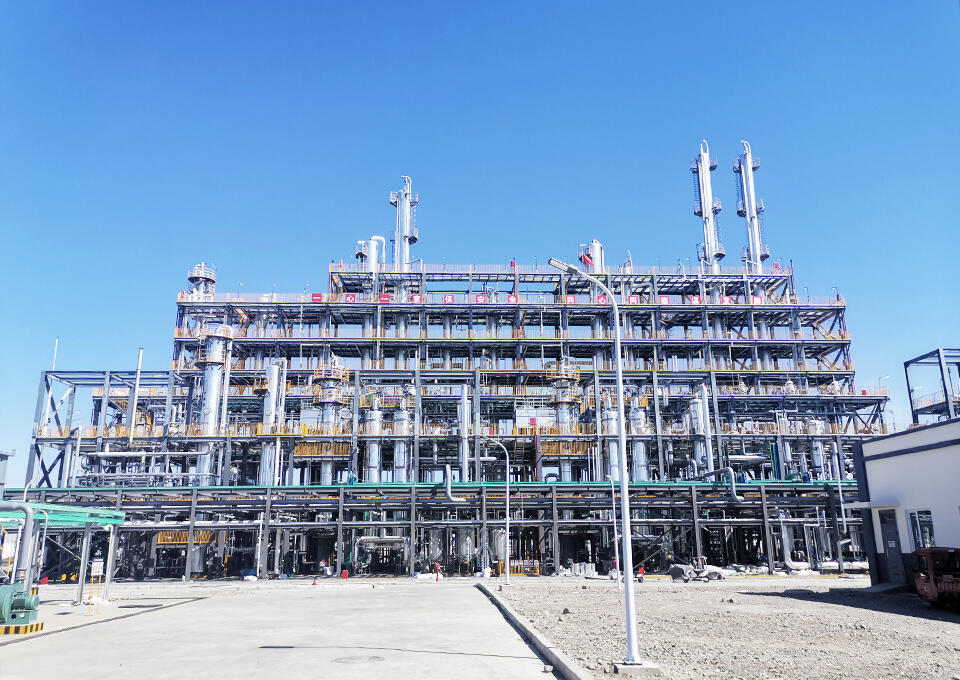
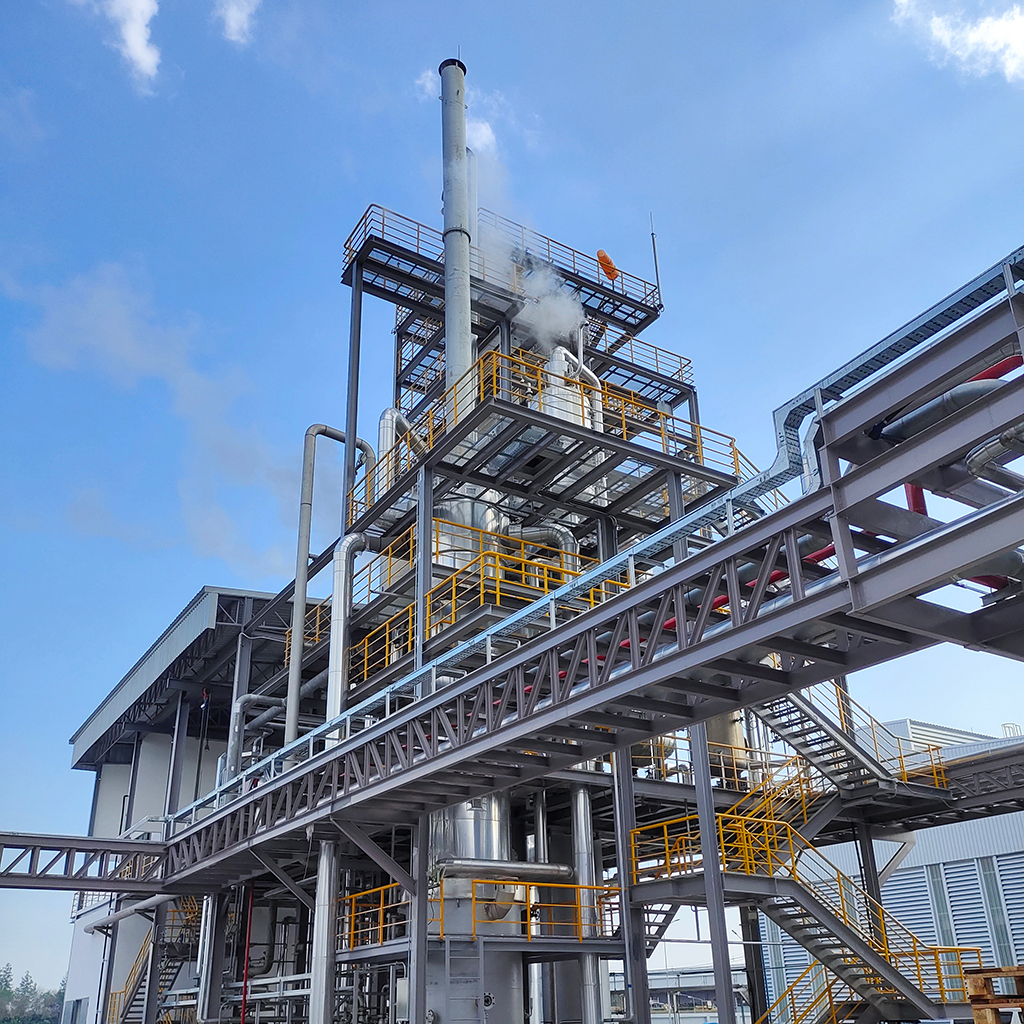
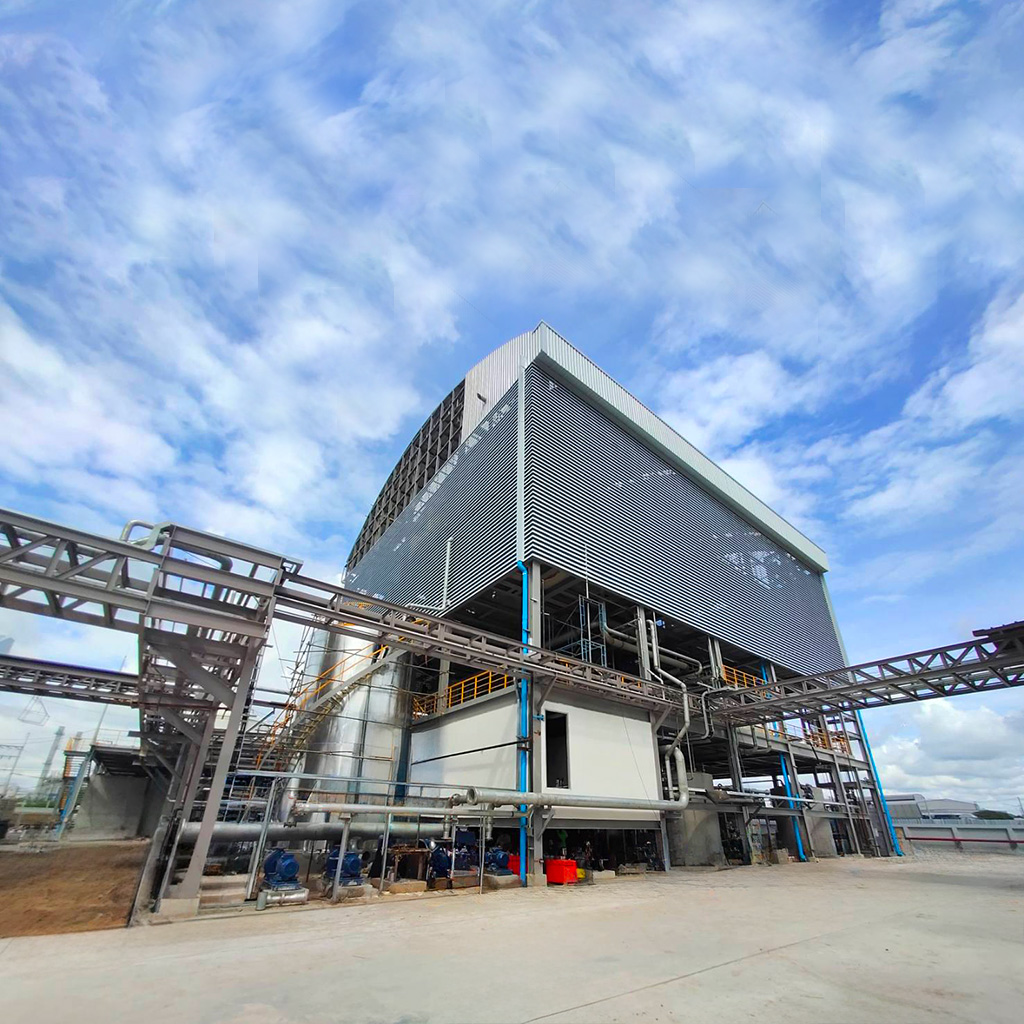
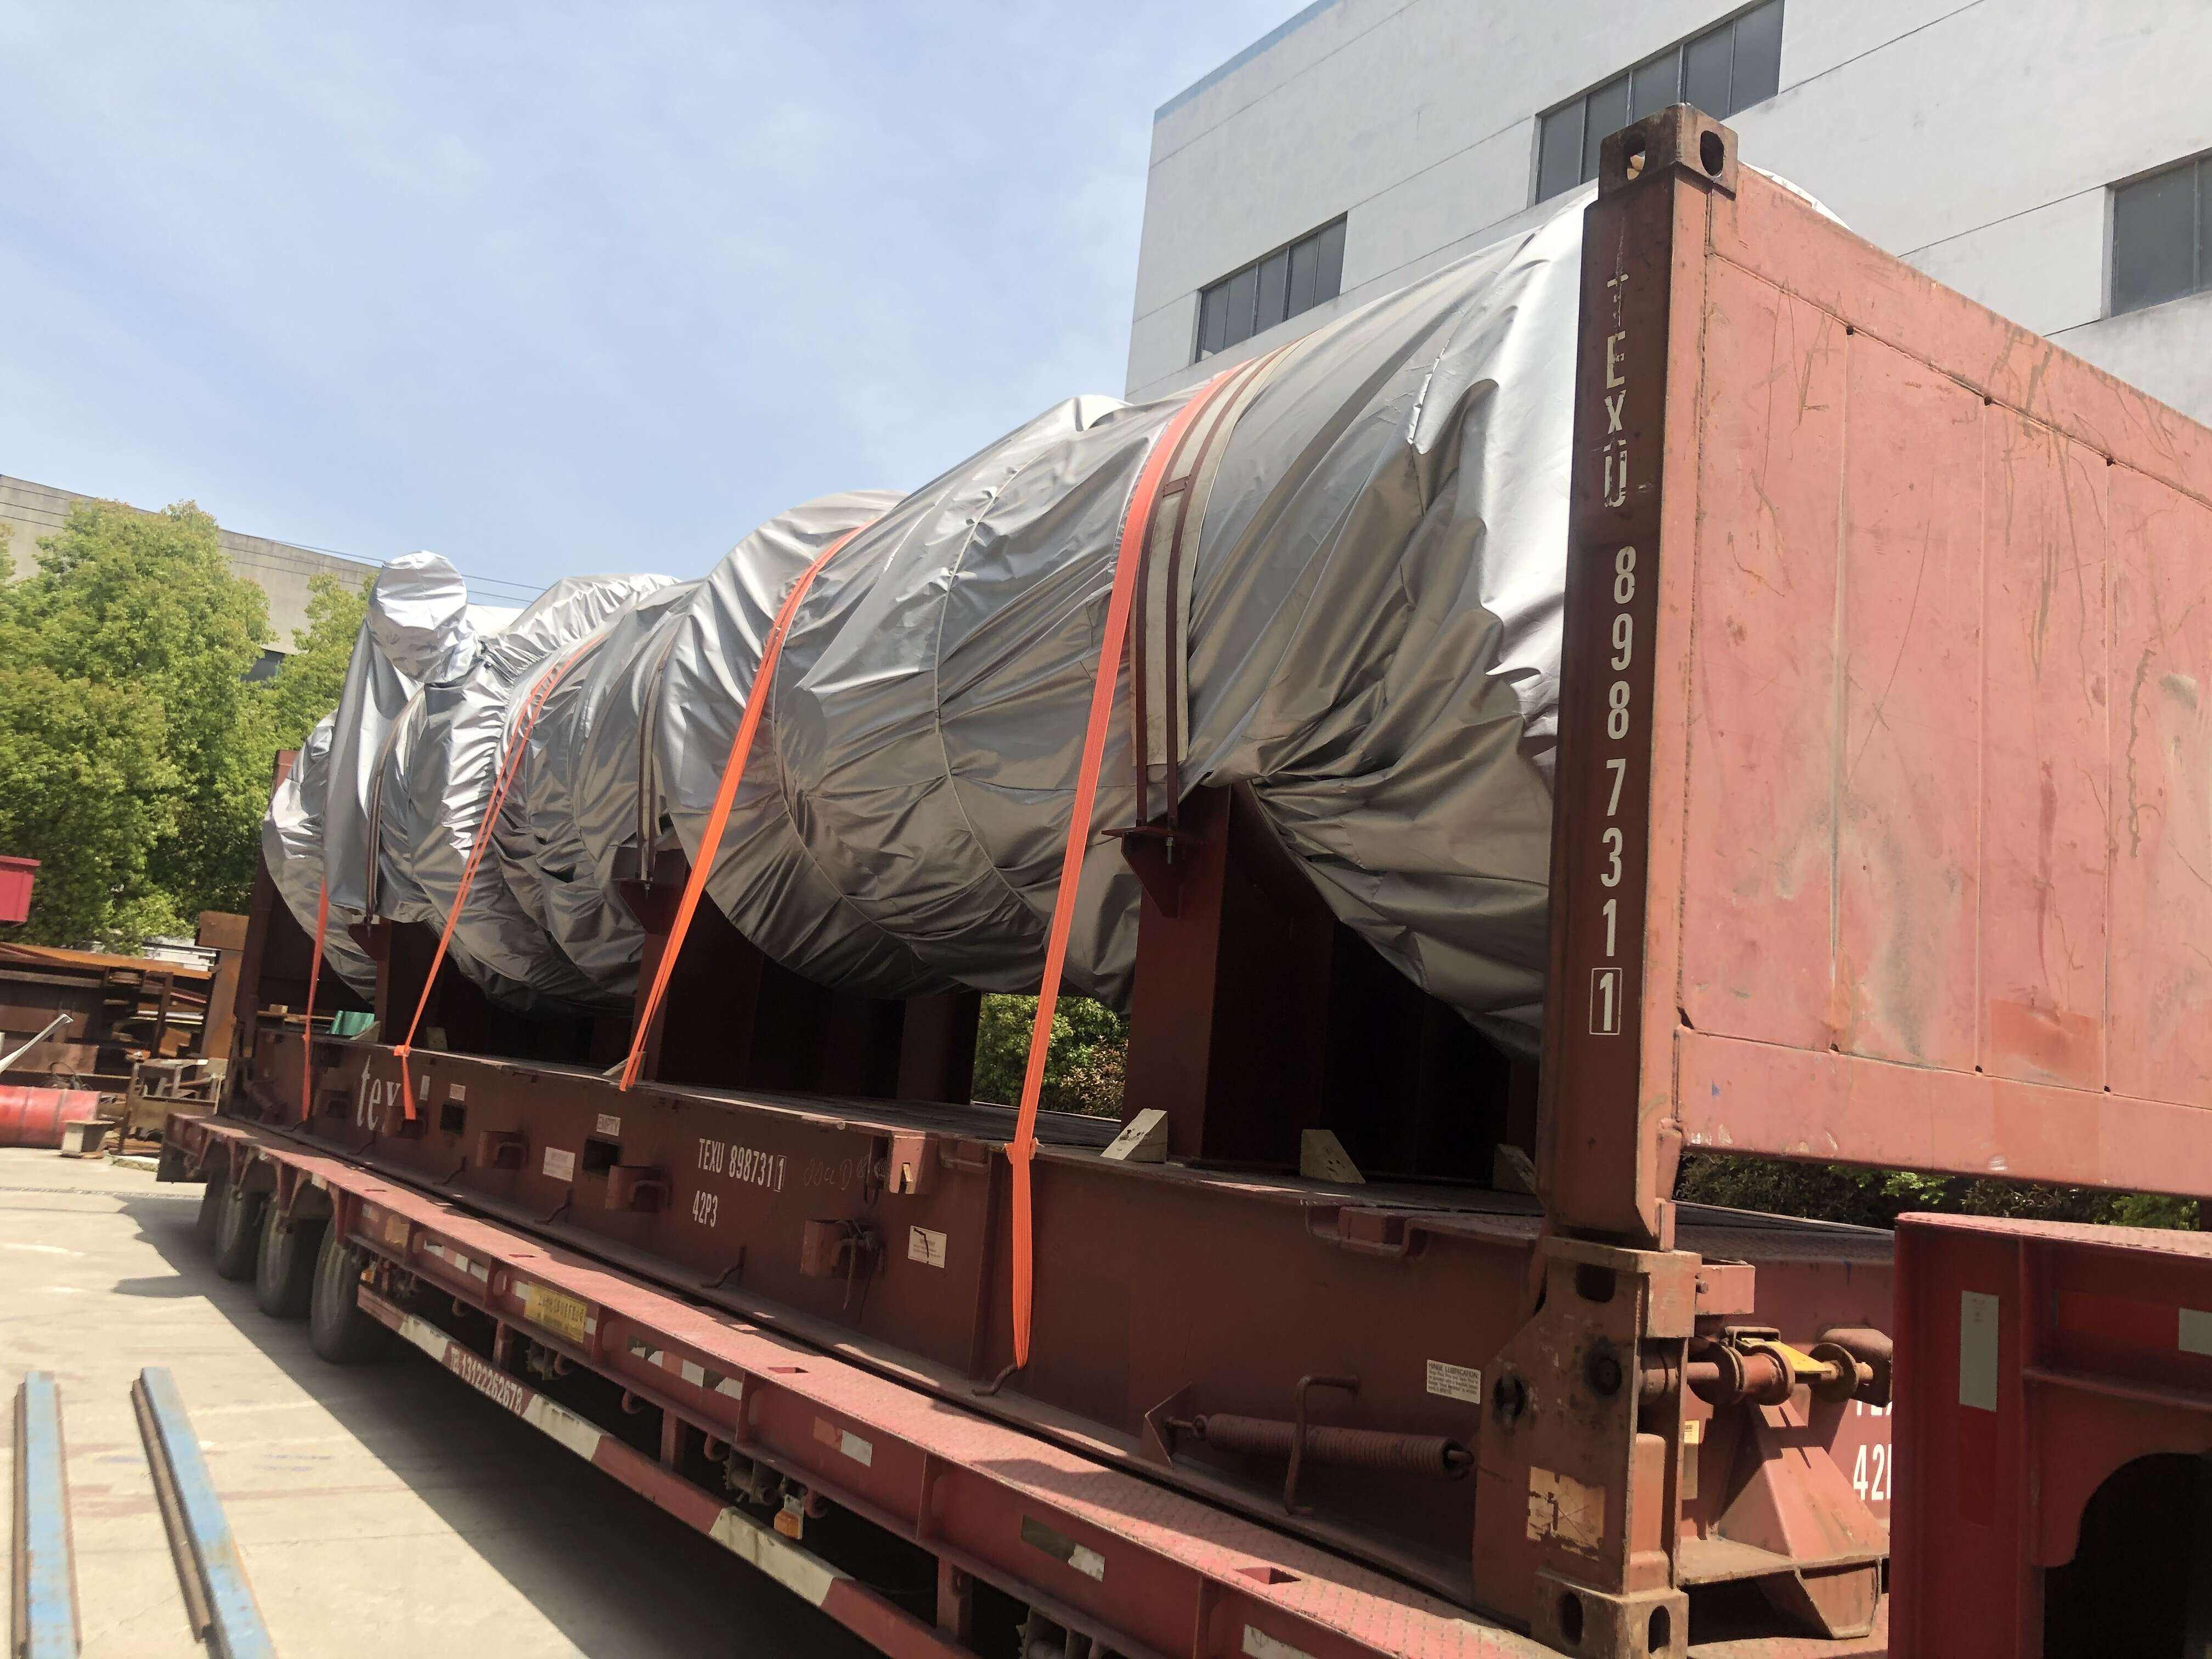
Chemical industrial equipment supply is a vital component in the success of chemical manufacturing operations. Changzhou Sanli Tech International Trade Co., Ltd. specializes in providing a comprehensive range of industrial equipment that meets the rigorous demands of the chemical sector. Our equipment is crafted from top-tier materials, ensuring durability and resistance to various chemicals, including corrosive substances, solvents, and high-viscosity fluids. For instance, our range of centrifugal pumps, both vertical and horizontal, are engineered to handle high-flow applications, making them ideal for large-scale chemical processing. A client in the water treatment industry required a pump that could handle high volumes of water with minimal energy consumption. We provided them with our energy-efficient centrifugal pumps, which not only met their flow requirements but also reduced their operational costs. In addition to standard pumps, we offer custom skid-mounted systems that can be tailored to specific process needs. These systems integrate multiple components, such as pumps, valves, and instrumentation, into a single, compact unit, reducing installation time and costs. A recent project involved designing a skid-mounted system for a chemical blending and storage application. The system included multiple pumps, a mixing tank, and an automated control system, allowing the client to blend and store chemicals efficiently and safely. Our chemical industrial equipment supply is backed by a team of experts who provide comprehensive support, ensuring our clients achieve the best possible outcomes.
Frequently Asked Questions

What services does the company provide in the formaldehyde field?

It can provide formaldehyde production process design and supporting equipment for efficient, safe, and stable production. It uses advanced catalyst and reaction condition control technology to improve yield and purity. It also has solutions for tail - gas treatment to meet environmental requirements. The supplied formaldehyde meets the needs of multiple industries like chemicals, building materials, and textiles.
For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.
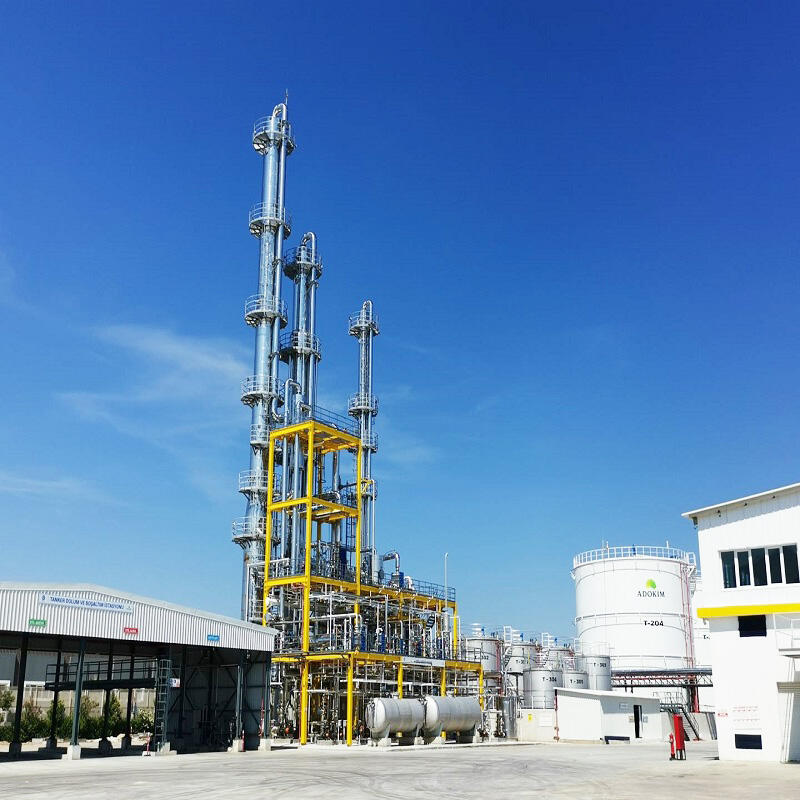
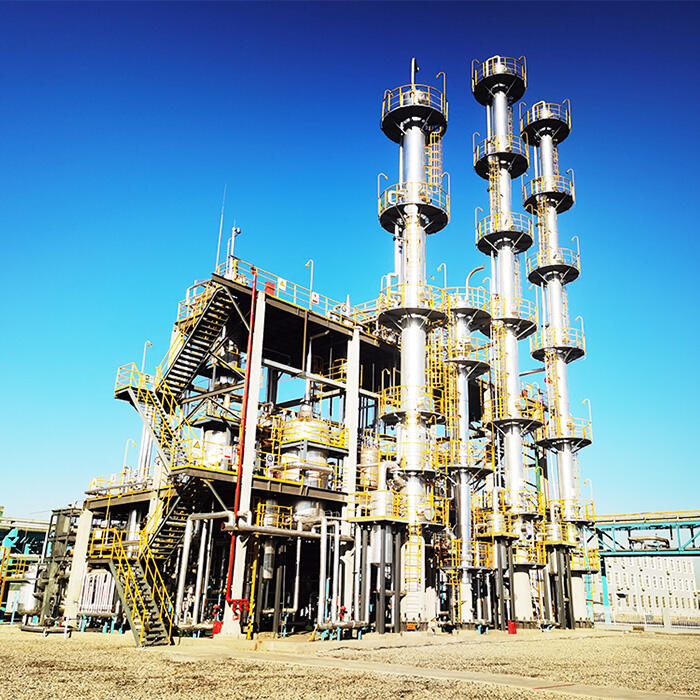
The company provides various types of towers and internals with rich materials including special alloys, ceramics, graphite, plastics, and stainless steel. For liquid distributors, there are Liquid Orifice Distributors, Liquid Trough Distributors, Liquid Ladder Distributors, and Liquid Spray Nozzle Distributors. It also offers gas distributors like Gas Distributor Spargers, packing supports, bed limiters, and mist eliminators such as Mesh Mist Eliminators and Chevron / Vane Type Mist Eliminators.

Related Articles

Outburst Of Demand On Carbon Fiber

03

Dec

Outburst Of Demand On Carbon Fiber

View More
Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

David Miller

Along with the equipment, the company provides excellent technical support. Their engineers are knowledgeable and can quickly solve any problems we encounter during installation or operation. They also offer valuable advice on equipment selection and usage.

Emily Johnson

We've been sourcing chemical industrial equipment from this company for years. Their products always meet our strict standards. The custom - made skid - mounted equipment has simplified our installation process and reduced costs. Their after - sales service is also excellent.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.