
pneumatic diaphragm chemical industrial pump supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
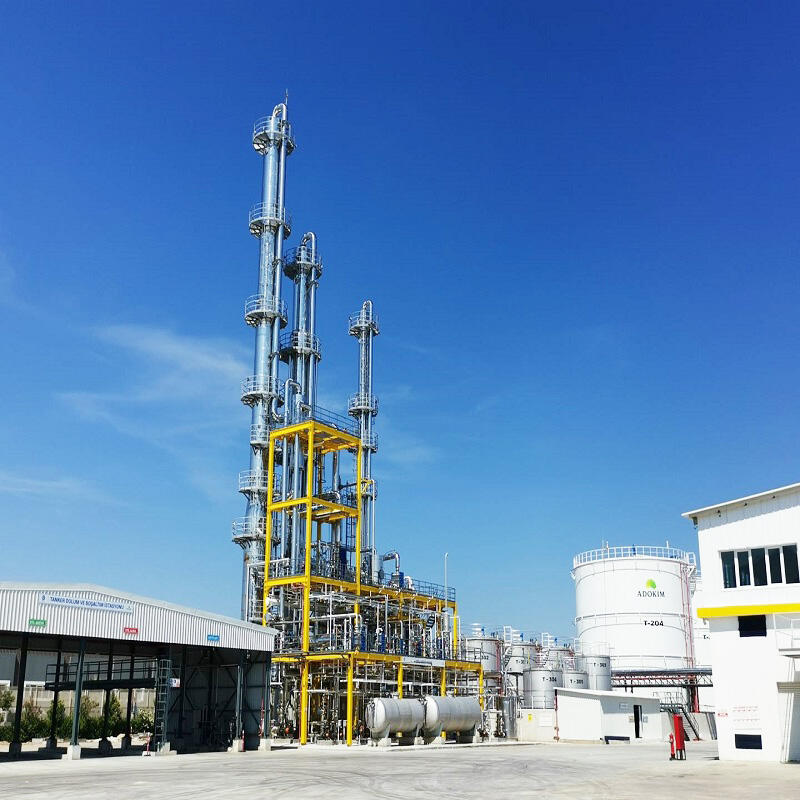
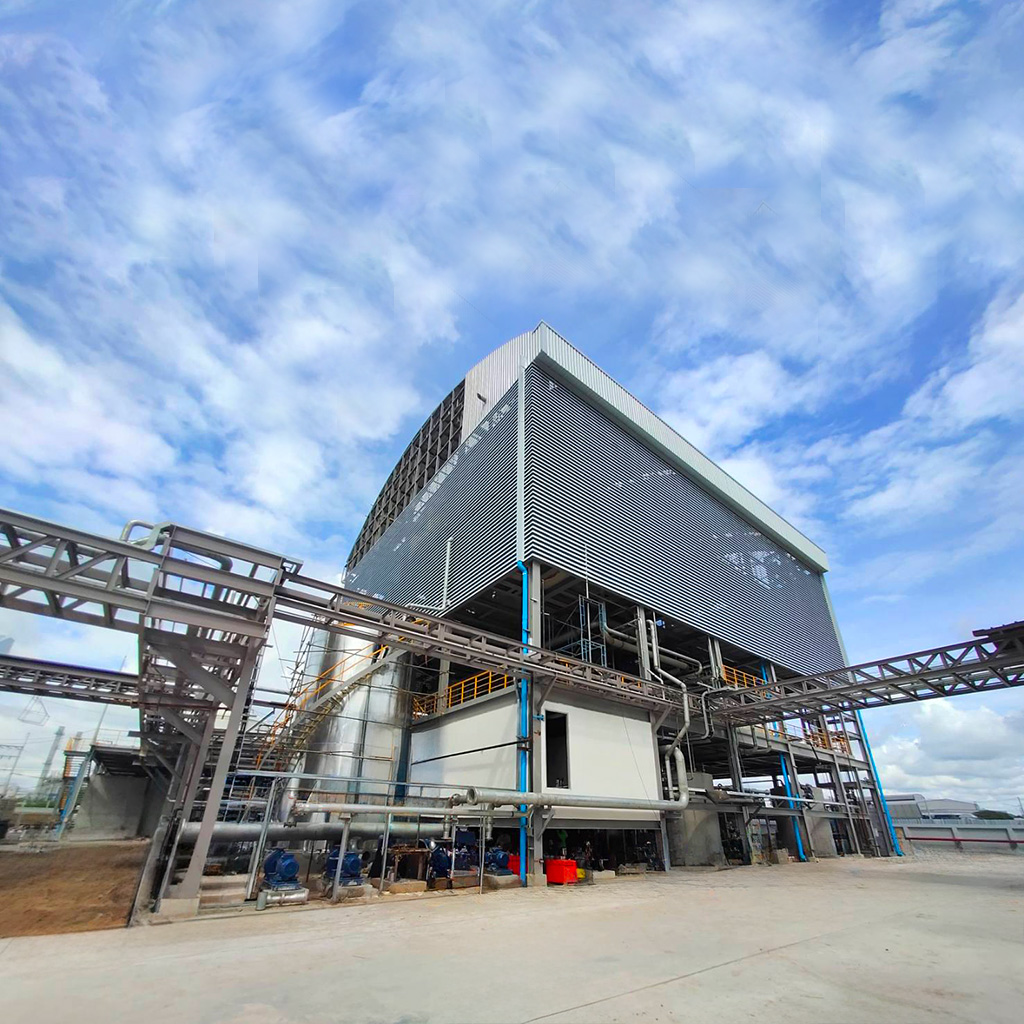
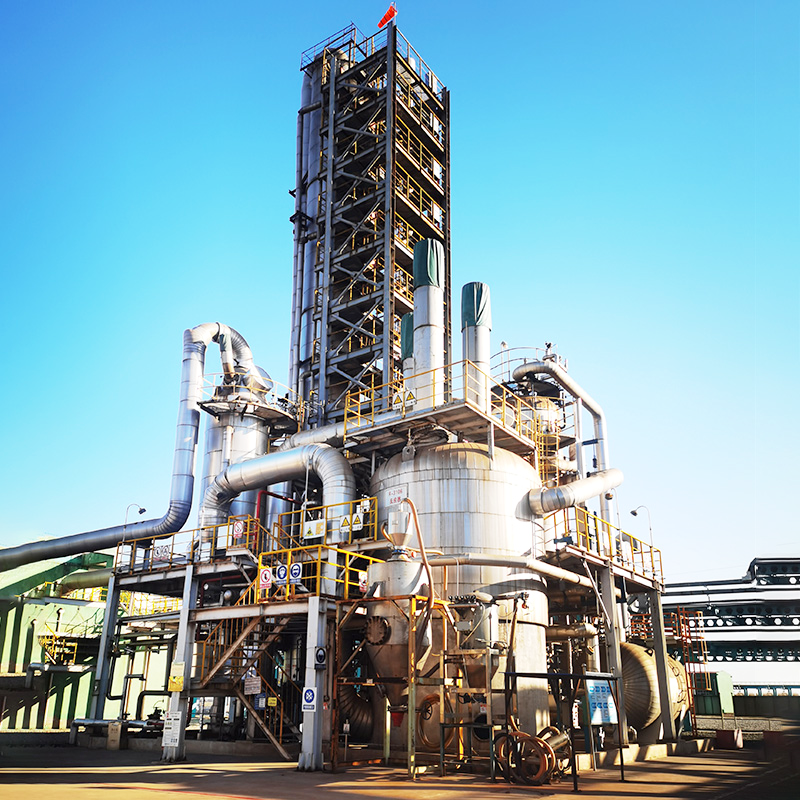
End-to-End Chemical Industrial Equipment Supply Services

End-to-End Chemical Industrial Equipment Supply Services

We offer end-to-end chemical industrial equipment supply services. From initial consultation and equipment selection to installation, commissioning, and after-sales support, we are with you throughout the entire process. Our comprehensive services ensure a seamless experience and maximum uptime for your chemical equipment.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

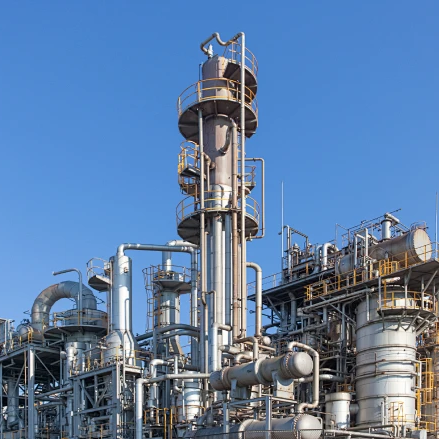
We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

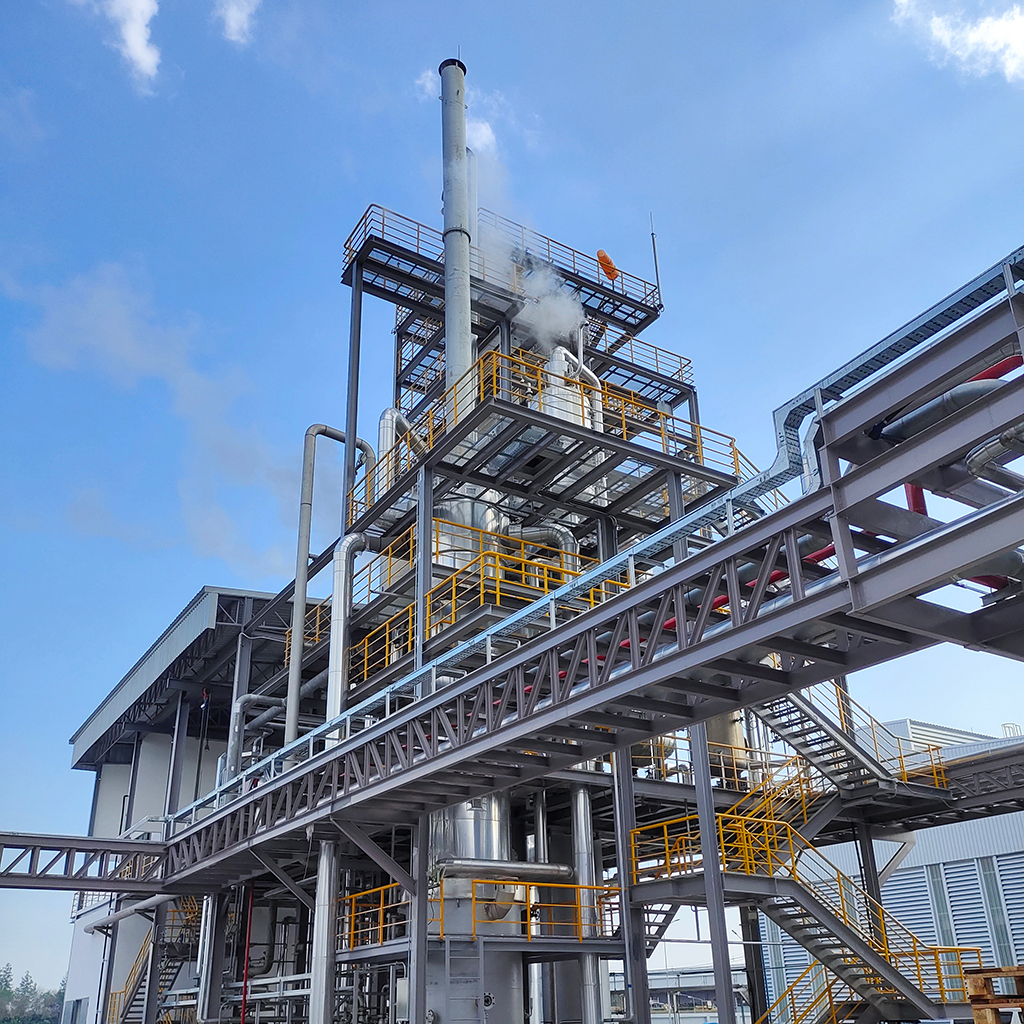
Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

All - round Services from On - site Guidance to Personnel Training

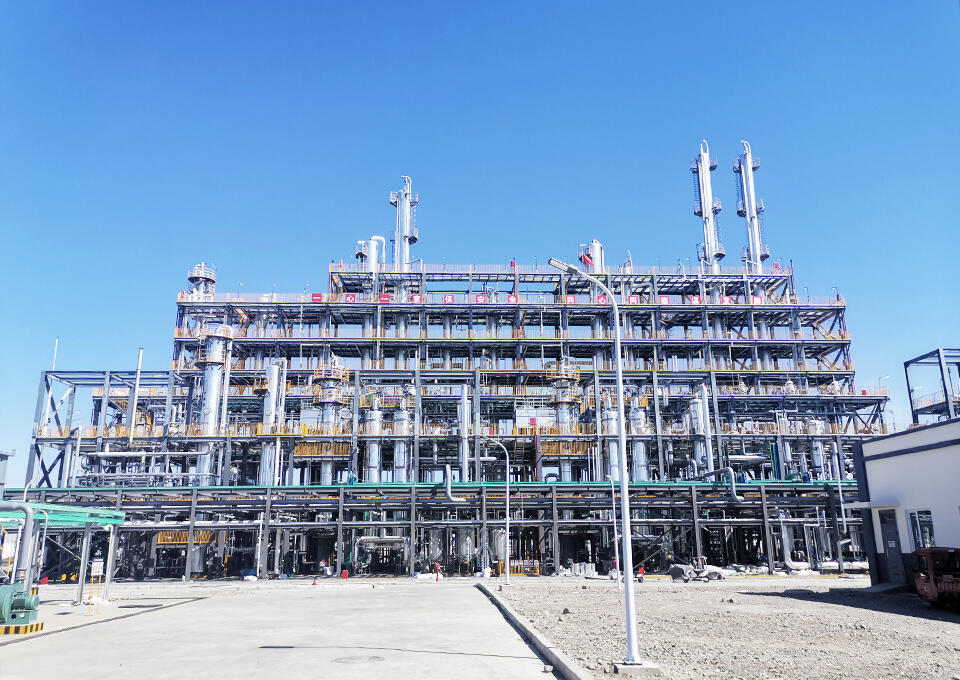
We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

The field of chemical industrial equipment supply is constantly evolving, driven by the need for more efficient and sustainable chemical processes. Changzhou Sanli Tech International Trade Co., Ltd. is at the forefront of this evolution, offering innovative equipment that enhances the performance and environmental footprint of chemical manufacturing. Our product range includes a variety of pumps, such as canned motor pumps and vertical inline pumps, which are designed for applications requiring high efficiency and low maintenance. For example, our canned motor pumps are hermetically sealed, eliminating the need for mechanical seals and reducing the risk of leaks, making them ideal for handling hazardous chemicals. A client in the chemical processing industry needed a pump that could safely transfer corrosive chemicals without the risk of environmental contamination. We supplied them with our canned motor pumps, which provided a safe and reliable solution, ensuring the protection of their personnel and the environment. In addition to pumps, we offer skid-mounted systems that integrate multiple components into a single, compact unit, reducing installation time and costs. These systems can be customized to include various pumps, valves, and control systems, all designed to work seamlessly together. A recent project involved supplying a skid-mounted system for a chemical dosing application. The system included a metering pump, flow meter, and control panel, allowing the client to accurately dose chemicals and monitor the process in real-time. Our chemical industrial equipment supply is supported by a commitment to sustainability and customer satisfaction, ensuring our clients receive the best possible products and support.

Frequently Asked Questions

What services does the company provide in the formaldehyde field?

It can provide formaldehyde production process design and supporting equipment for efficient, safe, and stable production. It uses advanced catalyst and reaction condition control technology to improve yield and purity. It also has solutions for tail - gas treatment to meet environmental requirements. The supplied formaldehyde meets the needs of multiple industries like chemicals, building materials, and textiles.
For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
For new chemical plants, it helps operators get familiar with equipment operation rules, processes, and safety precautions. For running plants, when production failures or process problems occur, on - site engineers can quickly diagnose and solve them, such as finding the root cause of abnormal tower pressure drops and proposing solutions.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Uses and Safety Precautions of Formaldehyde in Industry

23

Jul

Uses and Safety Precautions of Formaldehyde in Industry

Explore the industrial applications, safety measures, regulatory frameworks, and innovation trends of formaldehyde. Discover its role in resin production, healthcare disinfectants, wood composites, and alternatives like bio-based adhesives and low-VOC resins.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

Lisa Garcia

The chemical industrial equipment we bought from this company has proven to be very durable. It has been exposed to various chemicals and harsh operating conditions, but it still functions well. This long - lasting performance has reduced our equipment replacement costs.

John Smith

The chemical industrial equipment supplied by this company is of top - notch quality. The materials used are durable and can withstand harsh chemical environments. The pumps, for example, have been running smoothly in our plant for a long time without any major issues. Highly recommended!

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.