
solvent resistant chemical industrial equipment supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Advanced Chemical Industrial Equipment Supply for Modern Plants

Advanced Chemical Industrial Equipment Supply for Modern Plants

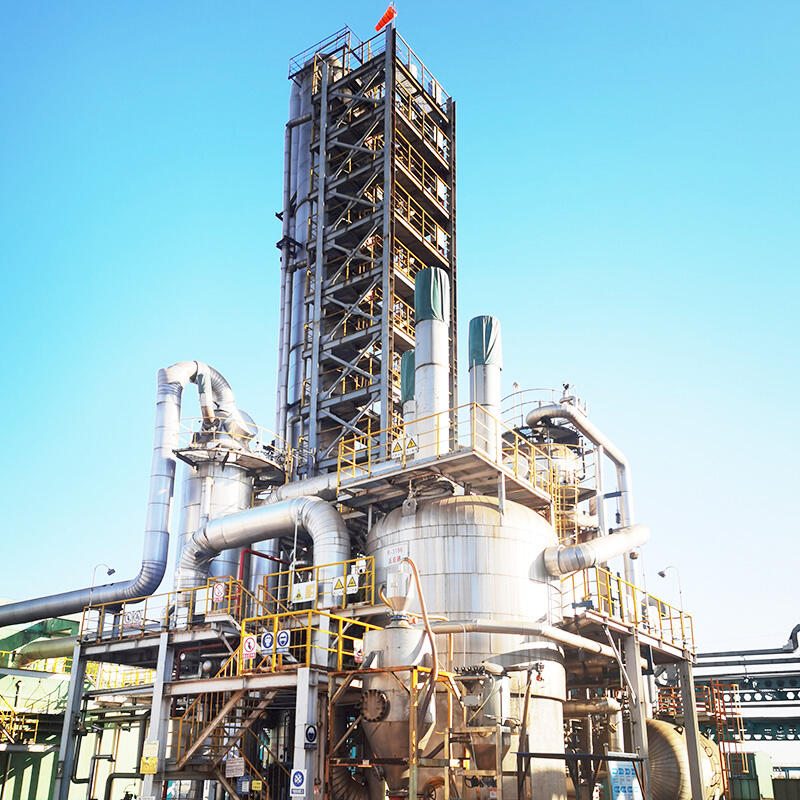
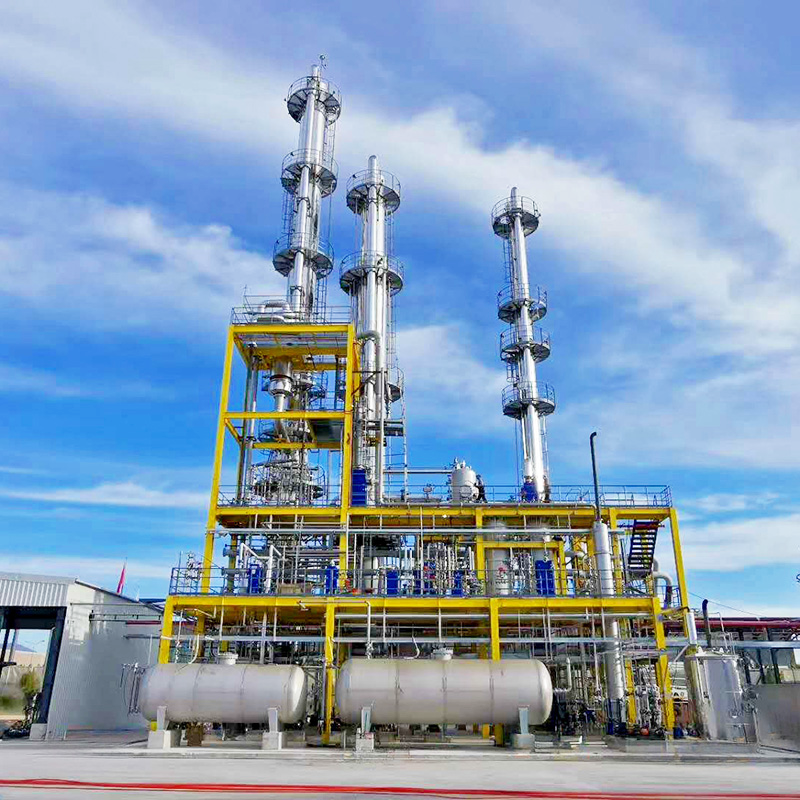
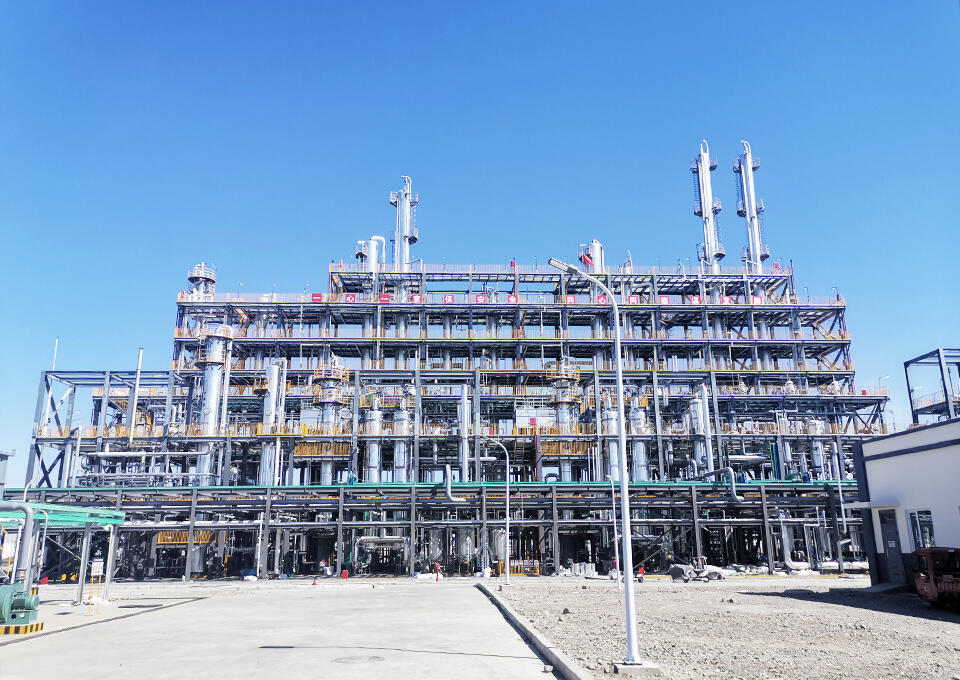
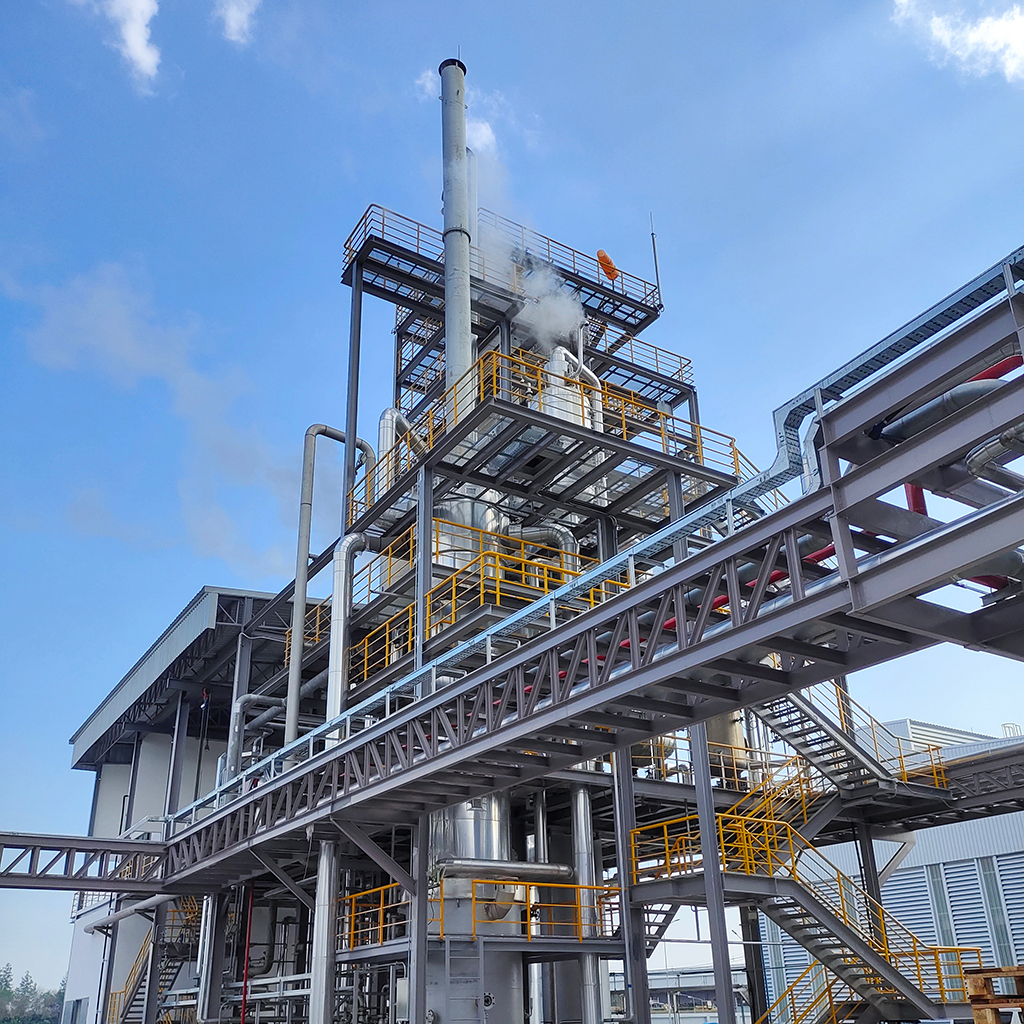
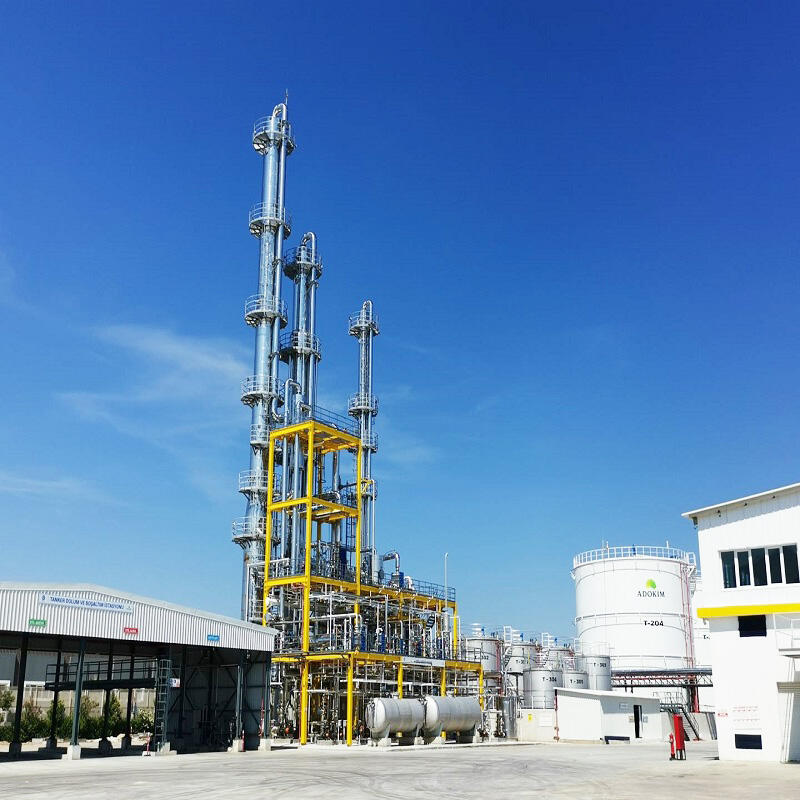
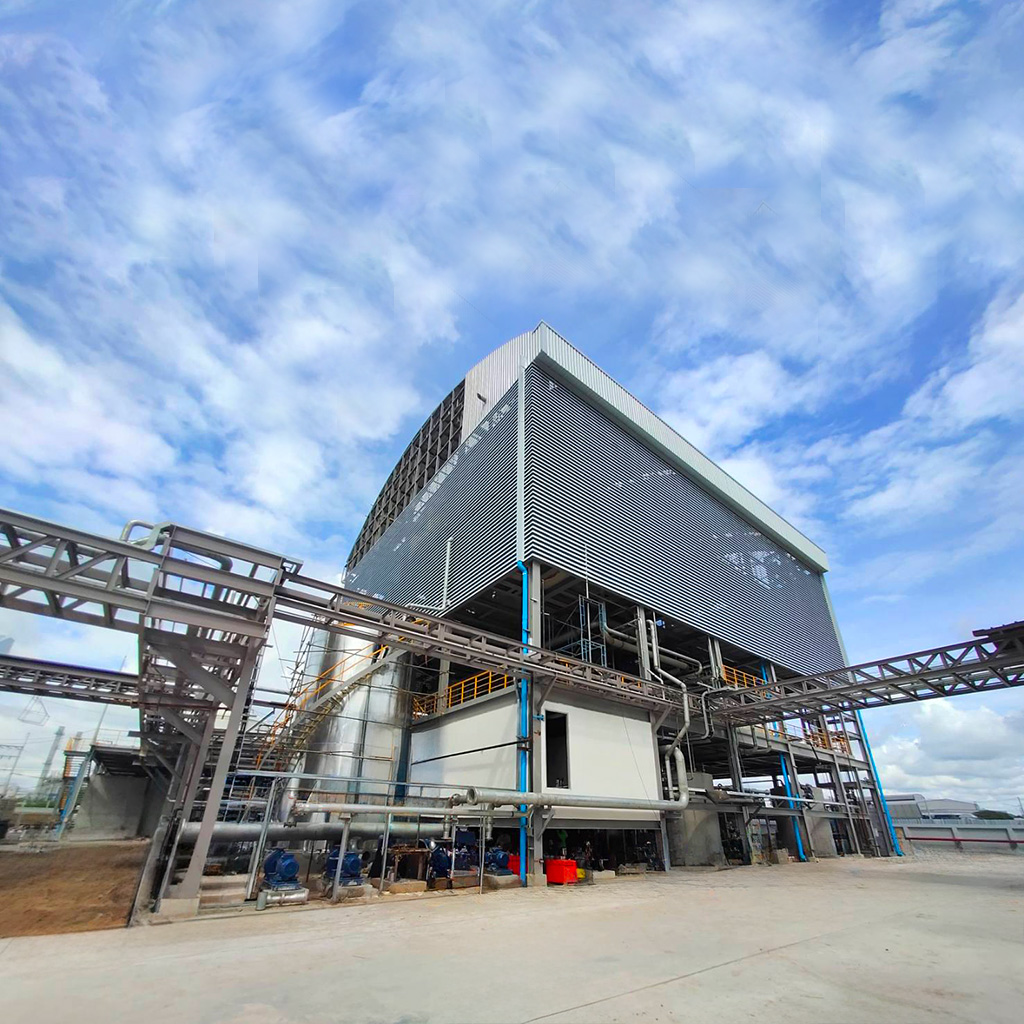
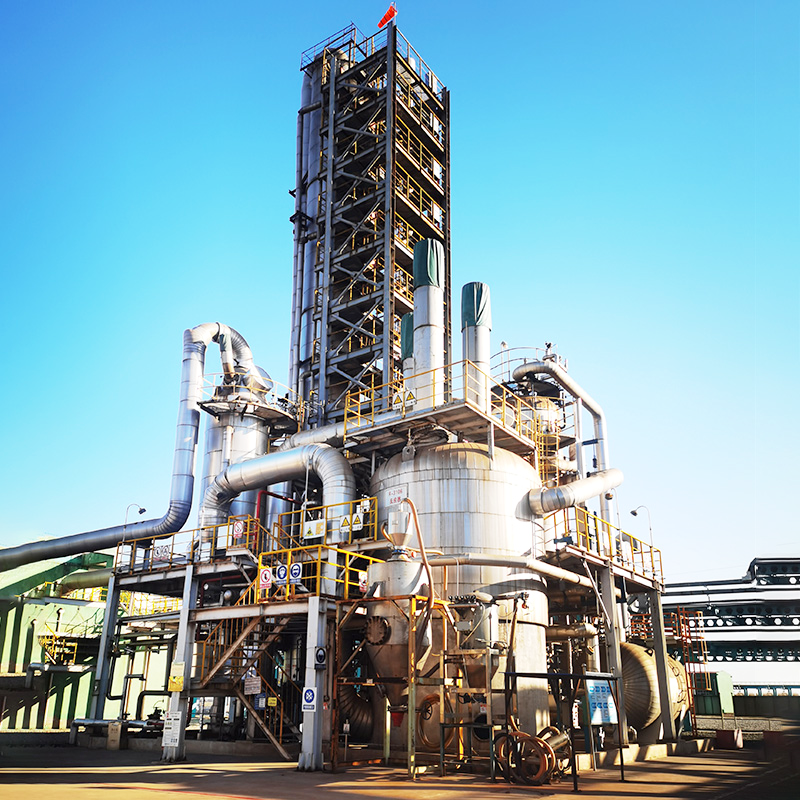
We offer advanced chemical industrial equipment supply for modern chemical plants. Our equipment incorporates the latest technologies, such as energy-efficient pumps and smart skid-mounted systems. These products help you optimize your chemical production, reduce energy consumption, and improve overall plant performance.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Advanced Chemical Production Technologies and Process Optimization

Our company masters advanced chemical production technologies covering multiple chemical product production processes. Whether it's chemical synthesis using jacketed glass reactors, uniform particle size achievement in paint production with basket mills, or solid - liquid separation with agitated nanofiltration filters, we can precisely control the production process. Moreover, our experienced technical team helps clients identify and implement the most efficient chemical processes and select appropriate technical solutions to enhance operational efficiency, reduce waste, and lower costs.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

Related products

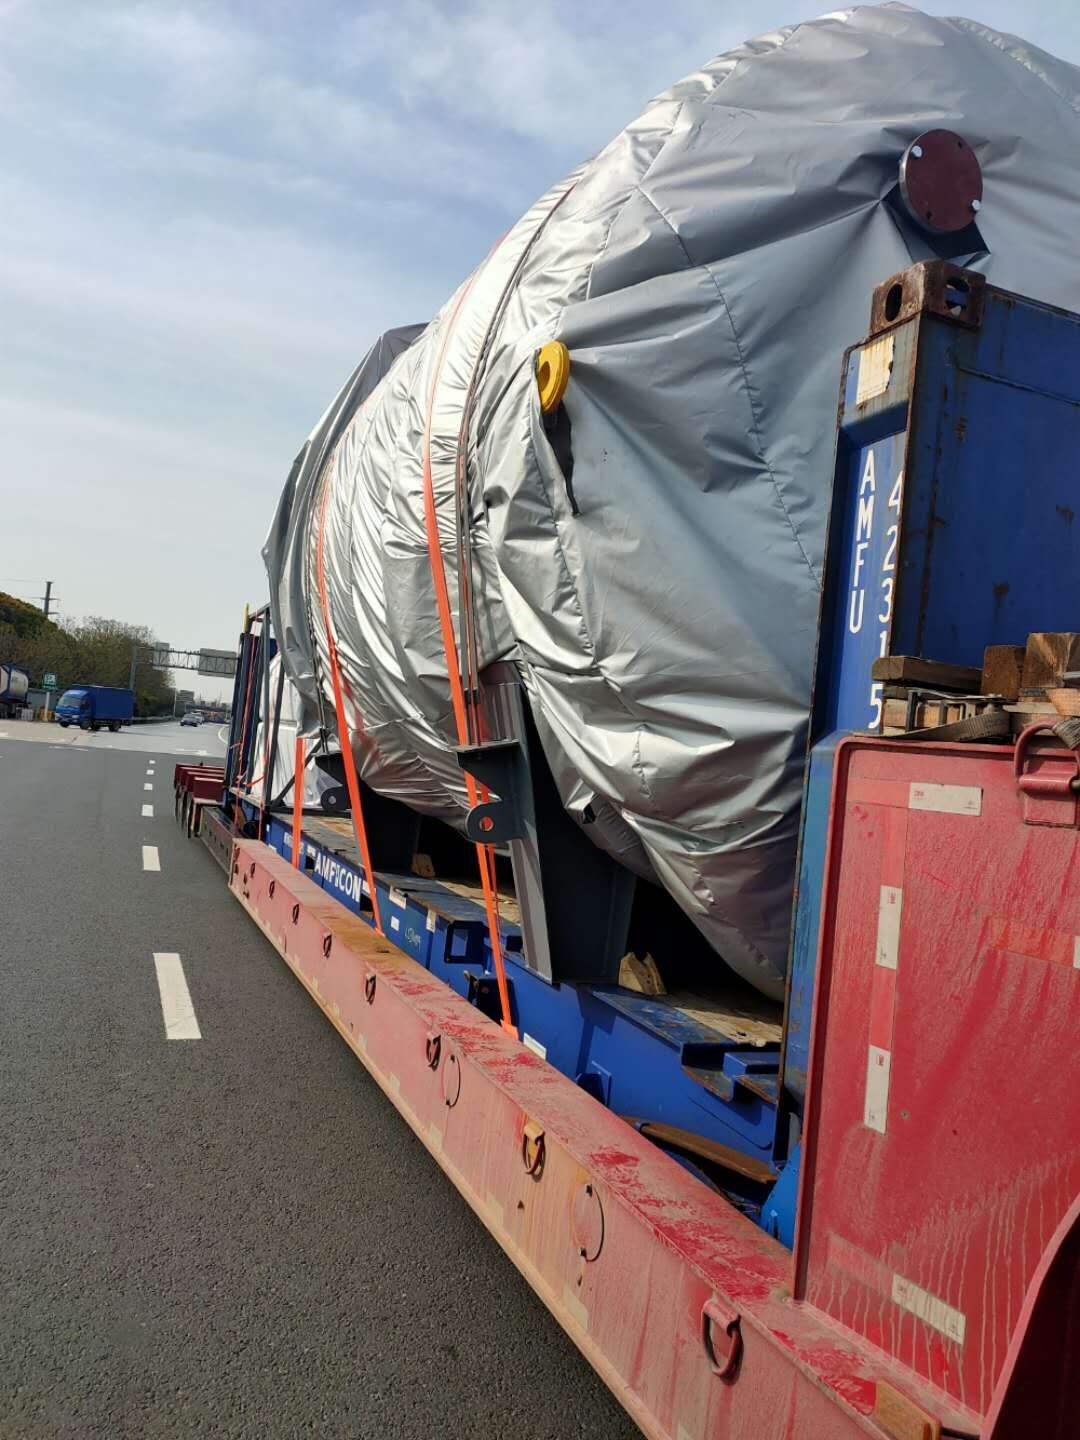
The realm of chemical industrial equipment supply is characterized by a constant pursuit of excellence and innovation. Changzhou Sanli Tech International Trade Co., Ltd. is committed to providing cutting-edge equipment that enhances the performance and reliability of chemical processes. Our product range includes advanced pumps like progressive cavity pumps and rotary lobe pumps, which are designed for applications requiring precise flow control and gentle handling of chemicals. For example, our progressive cavity pumps are widely used in the food and beverage industry for transferring viscous and shear-sensitive products, ensuring minimal product degradation and consistent quality. A client in the dairy industry needed a pump that could handle high-viscosity dairy products without altering their texture or consistency. We supplied them with our progressive cavity pumps, which provided a gentle and reliable solution, enhancing their production efficiency and product quality. In addition to pumps, we offer skid-mounted systems that incorporate the latest technology for improved process control and monitoring. These systems can be equipped with sensors, actuators, and advanced control systems, allowing for real-time data collection and analysis. A client in the chemical processing industry implemented our skid-mounted system with integrated control, which enabled them to optimize their process parameters, reduce waste, and improve product quality. Our chemical industrial equipment supply is supported by a team of experts who provide comprehensive support, ensuring our clients achieve the best possible outcomes.

Frequently Asked Questions

What on - site guidance services does the company offer for chemical plant operation?

For new chemical plants, it helps operators get familiar with equipment operation rules, processes, and safety precautions. For running plants, when production failures or process problems occur, on - site engineers can quickly diagnose and solve them, such as finding the root cause of abnormal tower pressure drops and proposing solutions.
It uses big data analysis to collect, analyze, and mine production data for process optimization, fault prediction, and quality improvement. Artificial intelligence algorithms enable intelligent control of production parameters. IoT technology allows remote monitoring and management of equipment, enabling engineers to check status, receive alarms, and perform operations remotely.
During factory design, it optimizes processes and equipment selection, like using efficient heat exchangers. In production, it uses advanced automation systems to adjust equipment parameters in real - time. It also offers energy management consulting to help establish monitoring and management systems for continuous energy efficiency improvement.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.

Related Articles

Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

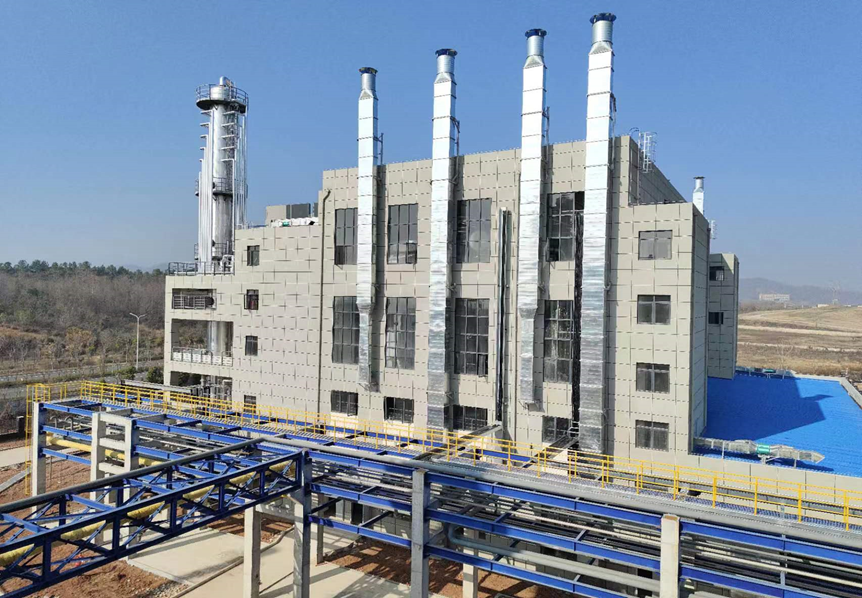
Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Role of Polymers in the Development of High - tech Industries

23

Jul

The Role of Polymers in the Development of High - tech Industries

Discover how polymer innovations are revolutionizing high-tech sectors, transforming manufacturing, sustainability, and technology applications. Explore the uses of photopolymers, high-performance polymers in aerospace, polyethylene glycol in drug delivery, and cutting-edge recycling methods for a greener future.
View More
The Intersection of Chemistry and Engineering in Production Technology

23

Jul

The Intersection of Chemistry and Engineering in Production Technology

Explore the transformative role of chemical engineering in production technology, digital transformation in chemical manufacturing using AI and IoT, sustainable material innovations, and future trends in polymer manufacturing and nanotechnology. Understand the significance of optimizing processes for efficiency and sustainability.
View More

Customer Reviews

Amanda Anderson

We have complete trust in this company as a chemical industrial equipment supplier. They have a good reputation in the industry, and their products have consistently performed well. We plan to continue our long - term cooperation with them.

John Smith

The chemical industrial equipment supplied by this company is of top - notch quality. The materials used are durable and can withstand harsh chemical environments. The pumps, for example, have been running smoothly in our plant for a long time without any major issues. Highly recommended!

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.