
high quality chemical industrial equipment supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
High-Capacity Chemical Industrial Equipment Supply for Large-Scale Plants

High-Capacity Chemical Industrial Equipment Supply for Large-Scale Plants

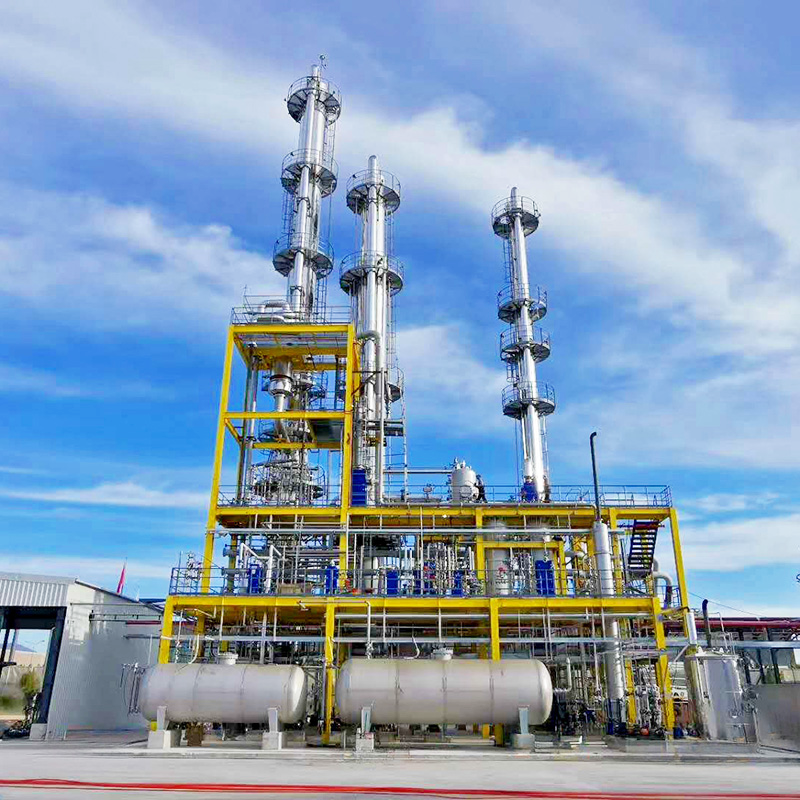
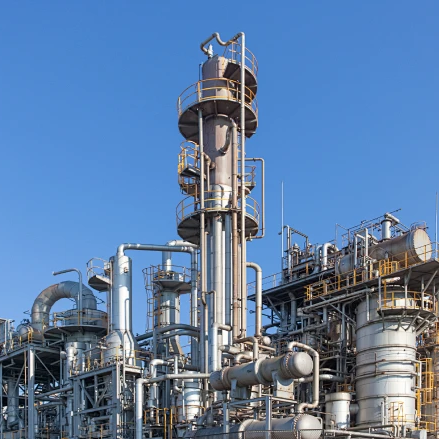
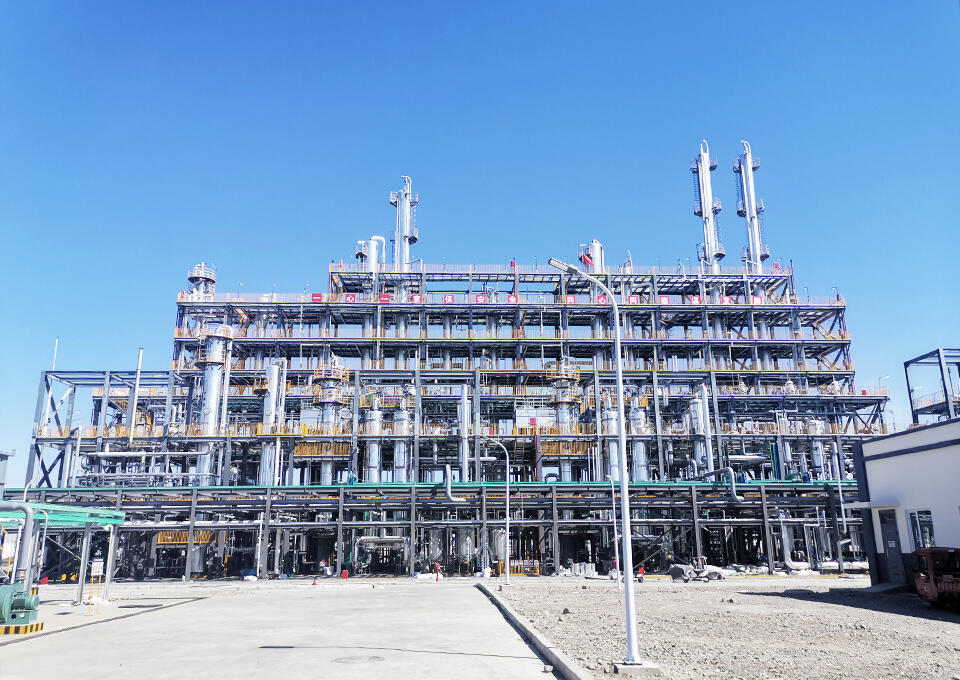
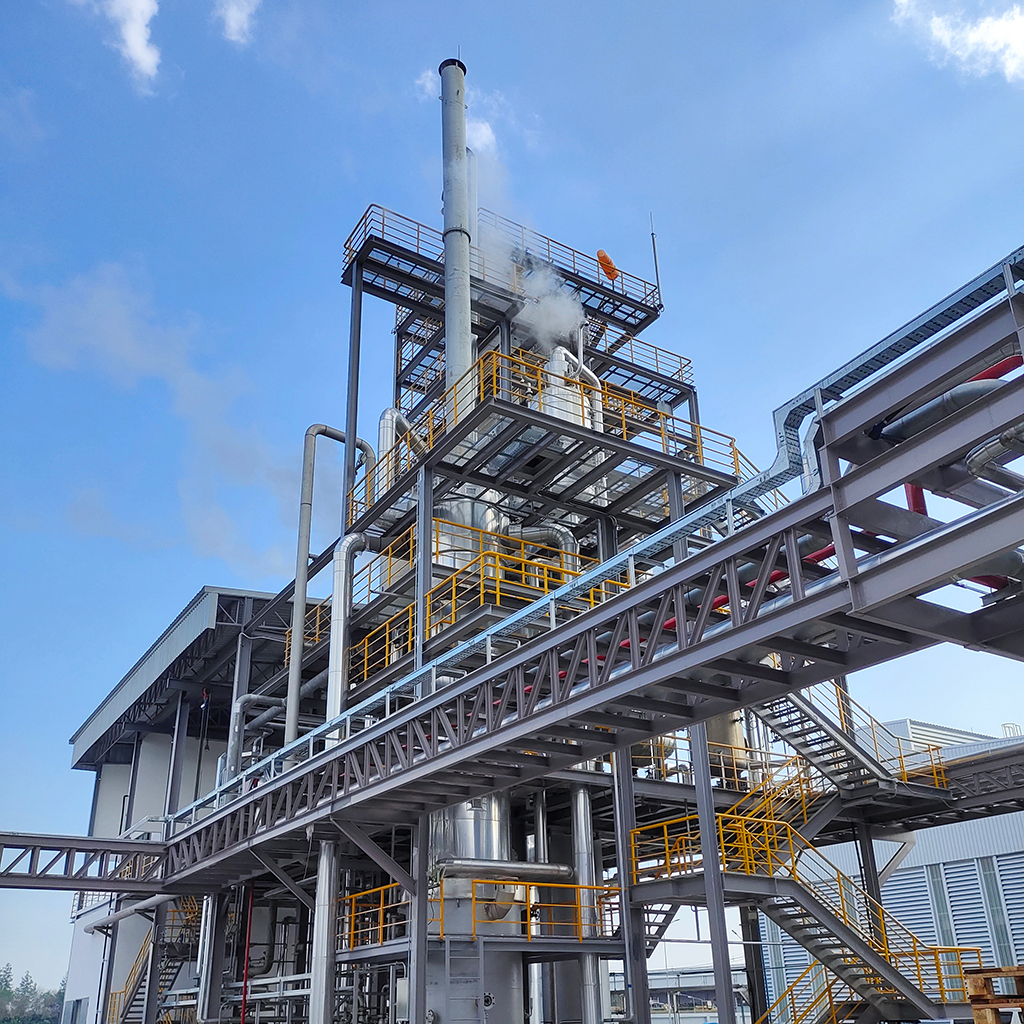
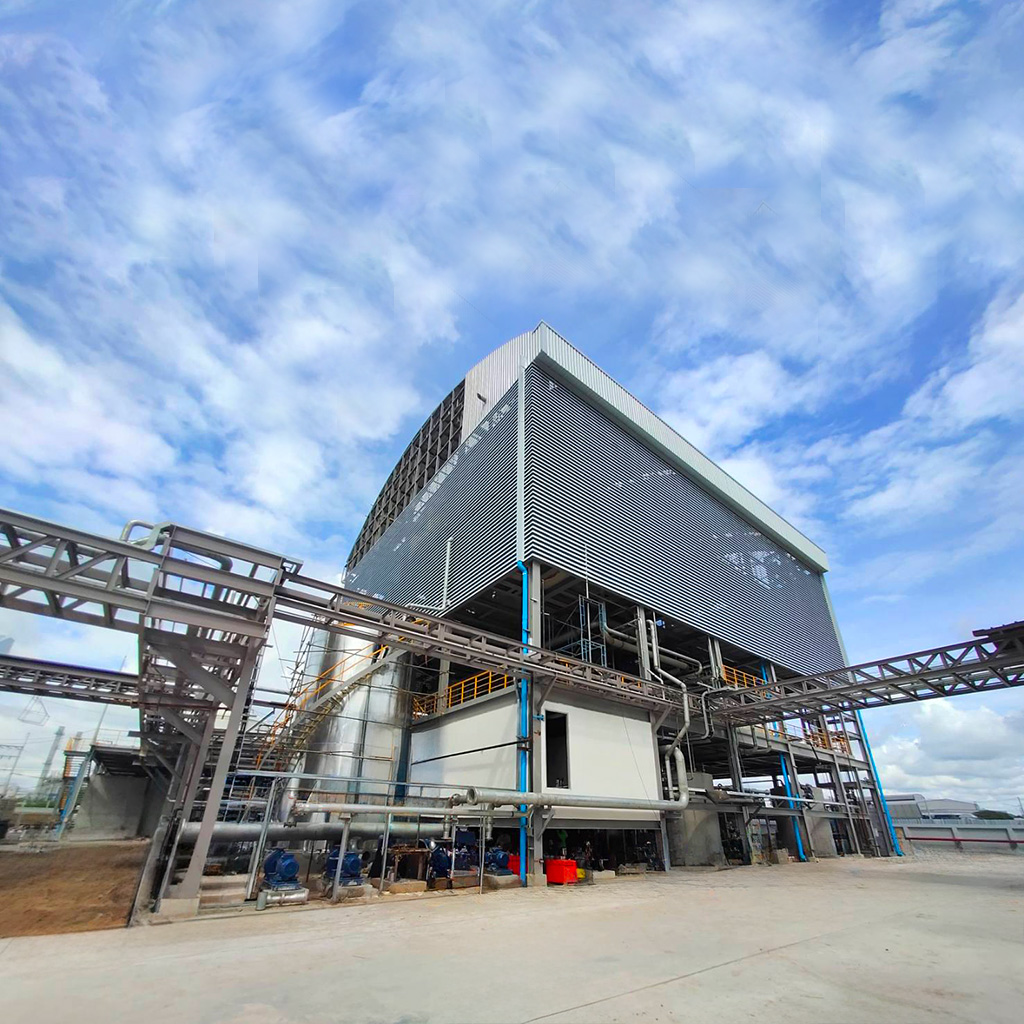
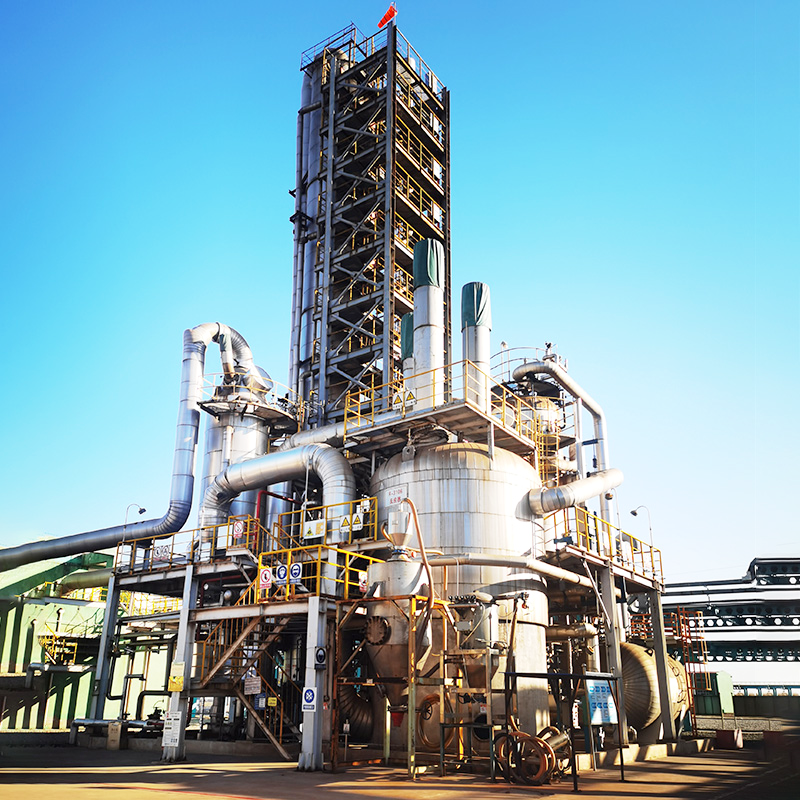
For large-scale chemical plants, we provide high-capacity chemical industrial equipment supply. Our pumps and skid-mounted systems are capable of handling high volumes of chemicals, ensuring uninterrupted production. With our robust equipment, you can meet your production targets and scale up your operations efficiently.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

Chemical industrial equipment supply is a fundamental aspect of ensuring the seamless operation of chemical manufacturing processes. At Changzhou Sanli Tech International Trade Co., Ltd., we specialize in providing a comprehensive range of industrial equipment designed to withstand the rigorous demands of the chemical industry. Our equipment is crafted from top-tier materials, ensuring durability and resistance to various chemicals, including solvents, paints, bleaches, acids, oils, and saltwater. For instance, our pump products, such as barrel and container pumps, pneumatic diaphragm pumps, and eccentric disc pumps, are engineered to handle different viscosities and corrosive substances, making them ideal for a wide array of chemical applications. In a recent project, a client in the paint industry required a reliable pumping solution for transferring high-viscosity paint formulations. We provided them with our eccentric disc pumps, which not only handled the viscosity effectively but also ensured minimal product degradation, resulting in consistent paint quality. Additionally, our custom-engineered skid-mounted equipment offers a single-point connection, reducing installation costs and time. These skids can incorporate various components like fans, motors, couplings, and baseplates, all adhering to relevant API and ANSI standards, ensuring compliance and safety. By choosing our chemical industrial equipment supply, clients can expect enhanced operational efficiency, reduced downtime, and a significant return on investment.

Frequently Asked Questions

What on - site guidance services does the company offer for chemical plant operation?

For new chemical plants, it helps operators get familiar with equipment operation rules, processes, and safety precautions. For running plants, when production failures or process problems occur, on - site engineers can quickly diagnose and solve them, such as finding the root cause of abnormal tower pressure drops and proposing solutions.
It supplies a wide range of equipment for the chemical market. Pump types include barrel and container pumps, pneumatic diaphragm pumps, eccentric disc pumps, etc. Besides single pumps and fan components, it provides customized skid - mounted equipment for single - point connection and cost - reducing installation, complying with relevant API and ANSI standards.
The company's experienced team offers comprehensive services. In process optimization and technology selection, it helps identify and implement efficient processes. For environmental compliance, it assists in dealing with regulations and sustainable practices. In safety and risk management, it guides robust protocols. It also supports innovation and IP protection, and optimizes supply chains for seamless integration of raw material procurement, transportation, storage, and distribution.
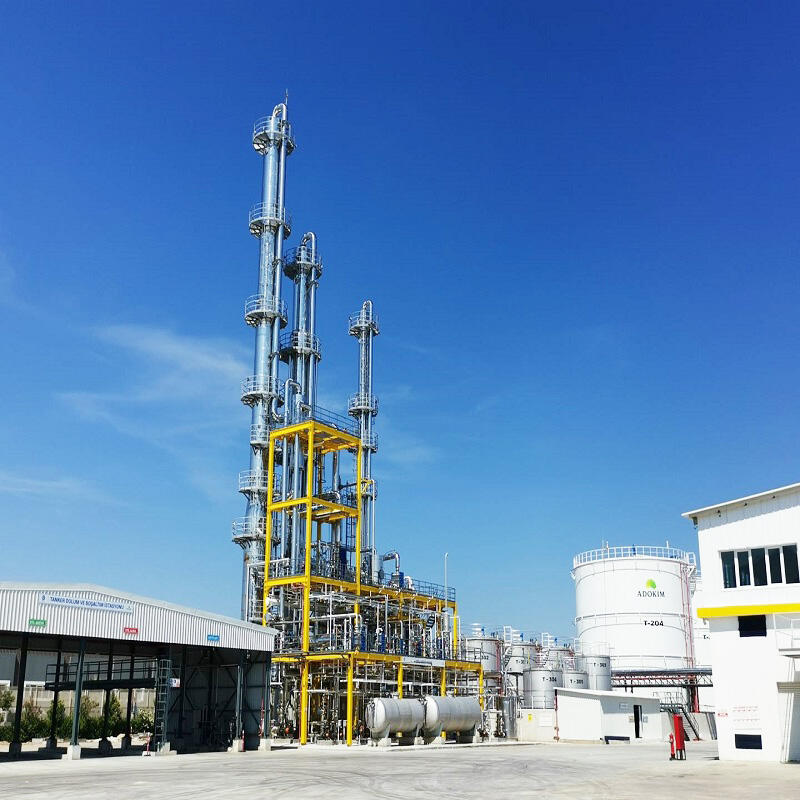
The company provides various types of towers and internals with rich materials including special alloys, ceramics, graphite, plastics, and stainless steel. For liquid distributors, there are Liquid Orifice Distributors, Liquid Trough Distributors, Liquid Ladder Distributors, and Liquid Spray Nozzle Distributors. It also offers gas distributors like Gas Distributor Spargers, packing supports, bed limiters, and mist eliminators such as Mesh Mist Eliminators and Chevron / Vane Type Mist Eliminators.

Related Articles

Challenges and Solutions in Chemical Production Technology

Challenges and Solutions in Chemical Production Technology

Explore the influence of geopolitical challenges on chemical supply chains, including trade conflicts, economic volatility, and technological innovations. Gain insights into strategies like supplier diversification and AI-driven optimization while addressing climate change and compliance for sustainable practices.
View More
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Intersection of Chemistry and Engineering in Production Technology

23

Jul

The Intersection of Chemistry and Engineering in Production Technology

Explore the transformative role of chemical engineering in production technology, digital transformation in chemical manufacturing using AI and IoT, sustainable material innovations, and future trends in polymer manufacturing and nanotechnology. Understand the significance of optimizing processes for efficiency and sustainability.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

David Miller

Along with the equipment, the company provides excellent technical support. Their engineers are knowledgeable and can quickly solve any problems we encounter during installation or operation. They also offer valuable advice on equipment selection and usage.

Sarah Davis

The manufacturing quality of the chemical industrial equipment is outstanding. The equipment is precisely made, and the attention to detail is evident. The non - metallic pumps we purchased have excellent corrosion resistance, which is crucial for our chemical processing.

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.