
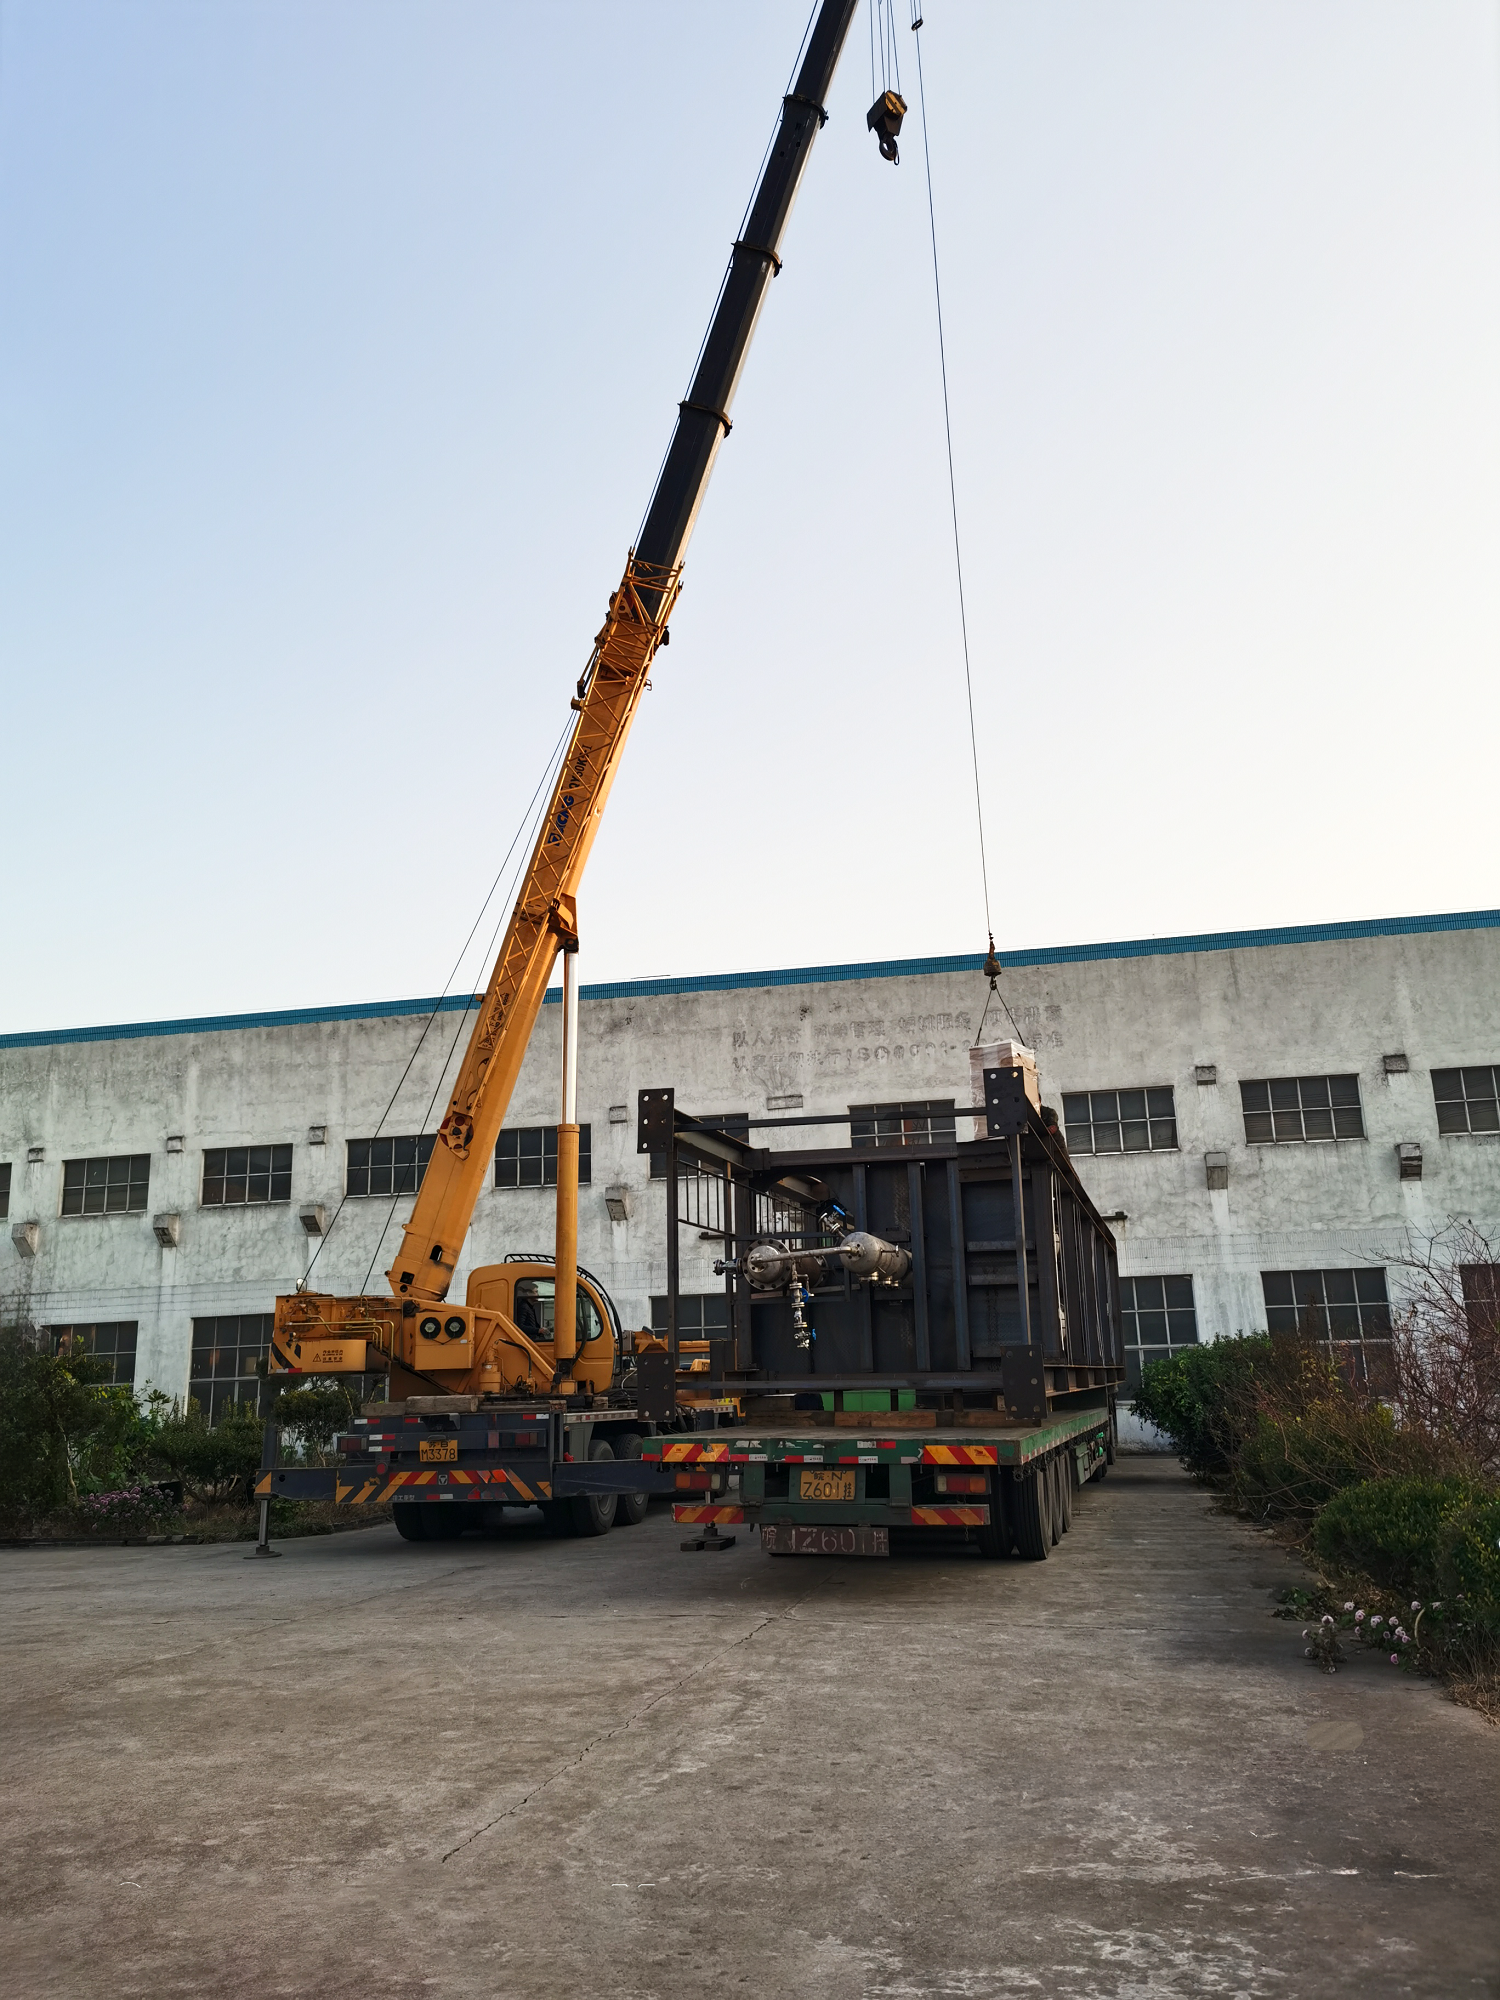
small scale chemical industrial skid mounted equipment supply|Advanced Chemical Industrial Equipment Supply | Smart & Energy-Efficient Solutions

All Categories
Global Chemical Industrial Equipment Supply Network

Global Chemical Industrial Equipment Supply Network

With our global chemical industrial equipment supply network, we can serve customers worldwide. We have established partnerships and distribution channels to ensure timely delivery of our high-quality products, including pumps and skid-mounted equipment, to any location. No matter where you are, we can meet your chemical equipment needs.
Get A Quote

Why choose us?

Comprehensive Chemical Industrial Equipment Supply with Top - grade Materials

We offer a wide range of chemical industrial equipment made from top - grade materials. These materials can withstand chemicals of different viscosities, corrosiveness, and abrasiveness, such as solvents, paints, bleaches, acids, oils, and saltwater. From various pumps like barrel pumps, diaphragm pumps, to customized skid - mounted equipment, all meet relevant API and ANSI standards, ensuring reliable and long - lasting performance in chemical processes.

Integrated Intelligent Chemical Engineering Solutions

We integrate cutting - edge information technology with chemical engineering. By leveraging big data analytics, we collect, analyze, and mine a large amount of data in the chemical production process to optimize production flow, predict equipment failures, and improve product quality stability. Artificial intelligence algorithms enable intelligent control of the production process, automatically adjusting parameters like reaction temperature and pressure. Additionally, the Internet of Things technology allows for remote monitoring and management of equipment, enhancing production operational efficiency and reliability.

All - round Services from On - site Guidance to Personnel Training

We provide comprehensive services throughout the entire chemical plant lifecycle. Our professional engineer teams offer on - site guidance for both newly - built and running chemical plants, ensuring correct equipment startup, stable operation, and timely troubleshooting. We also offer in - depth personnel training courses covering different positions and skill requirements, from operation skills and process control for operators to process optimization and new technology application for technicians, and industry management knowledge for managers, facilitating the efficient operation of chemical plants.

Related products

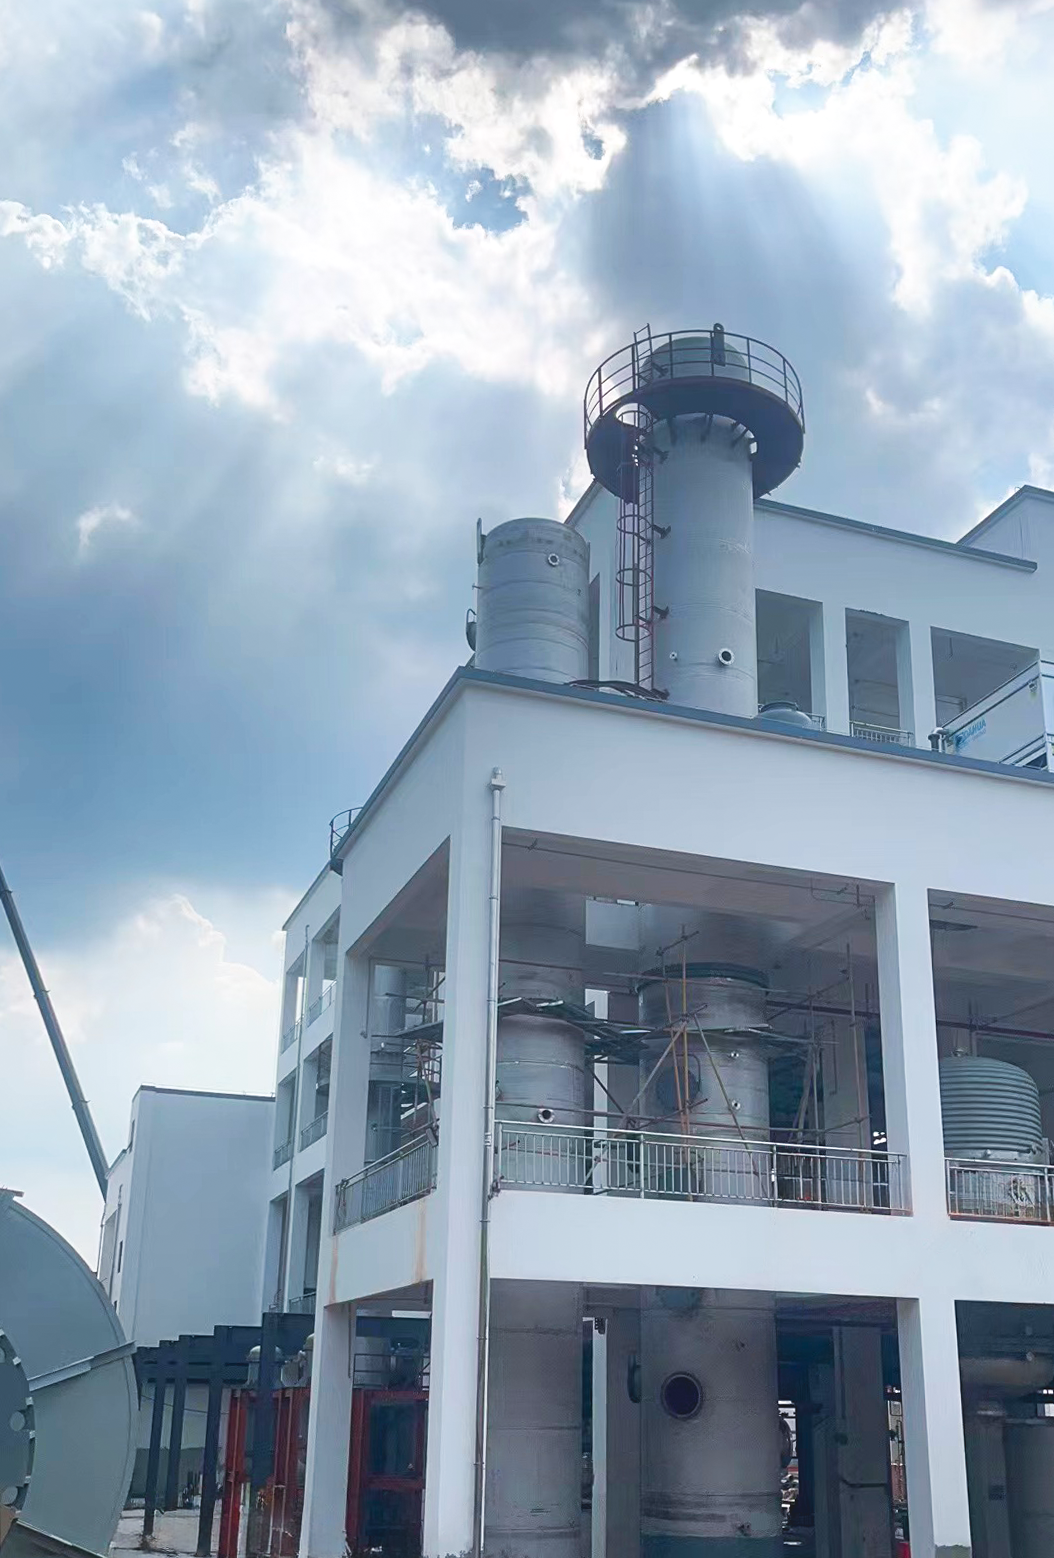
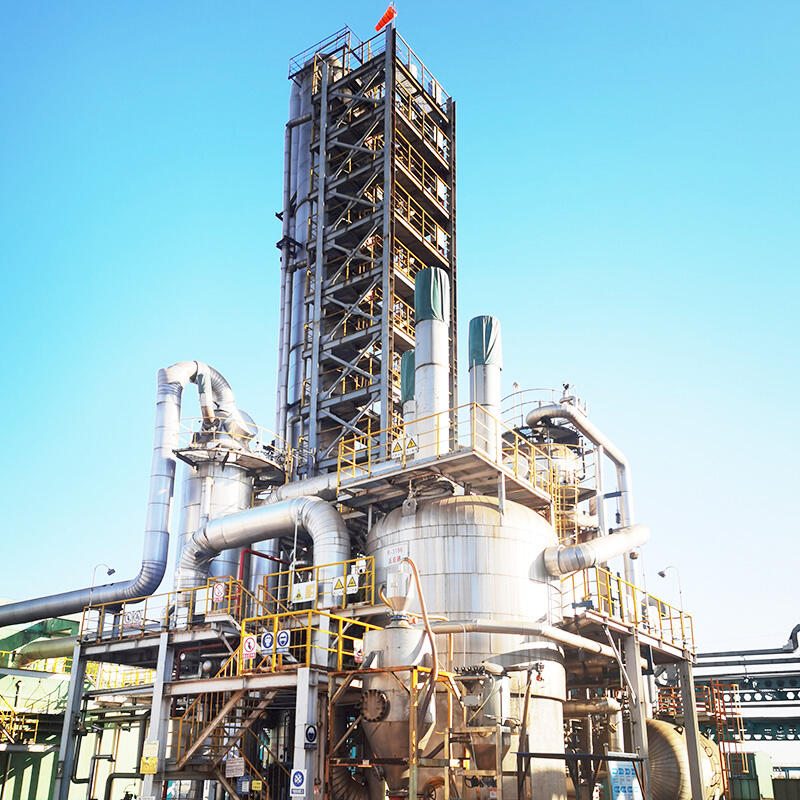
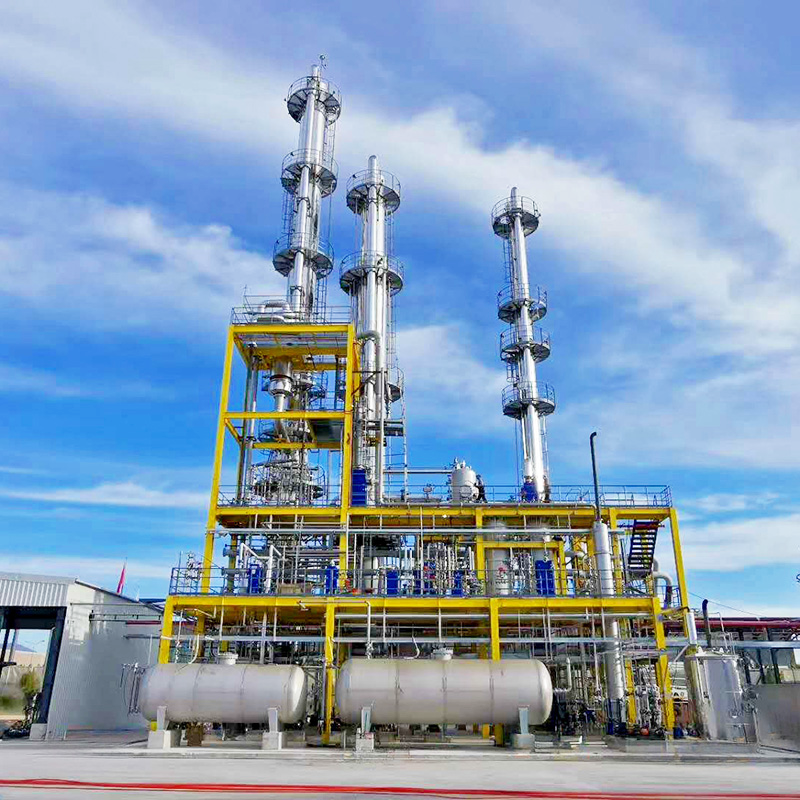
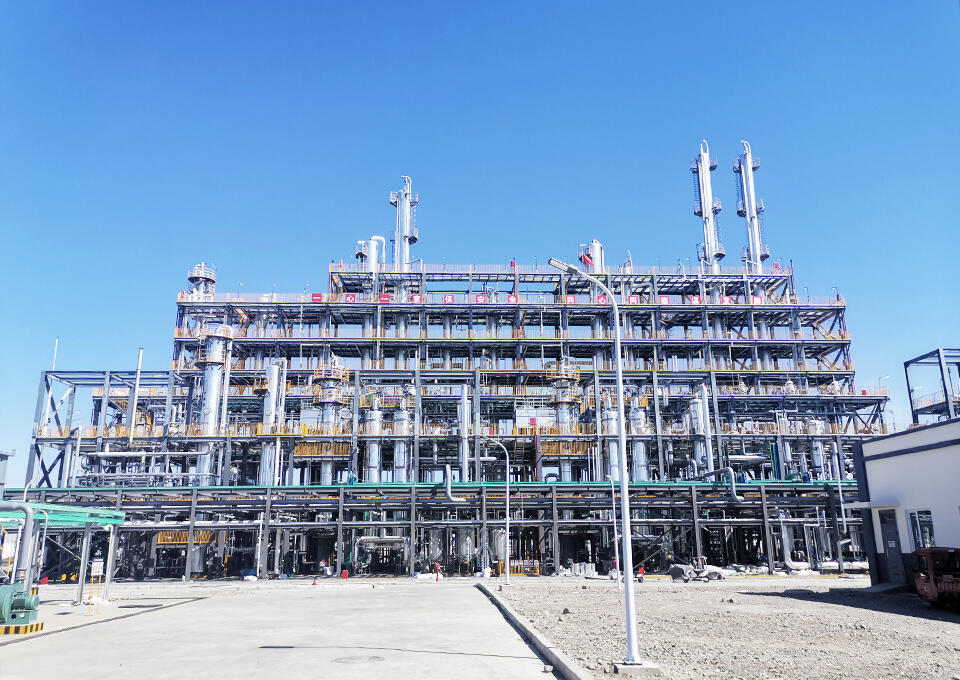
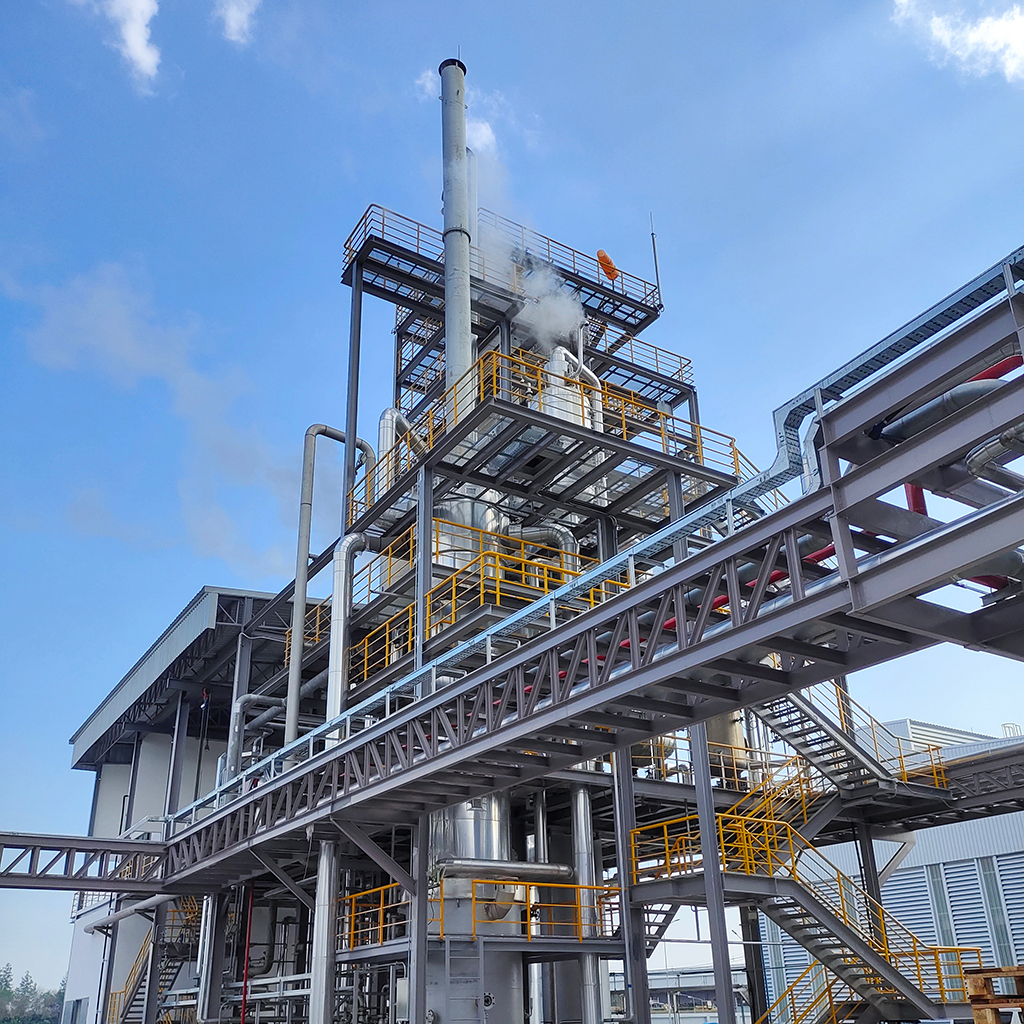
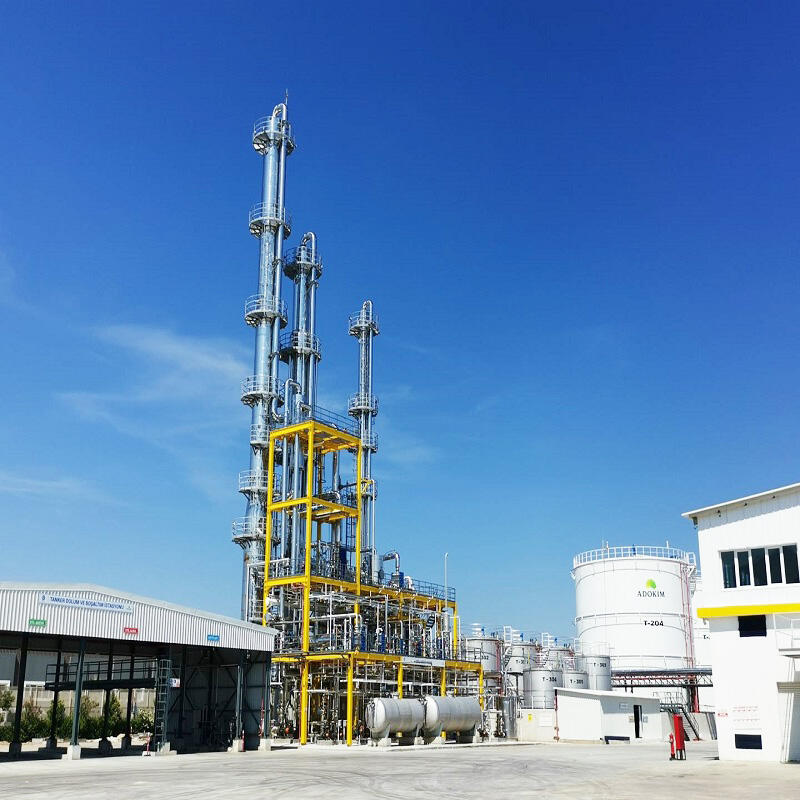
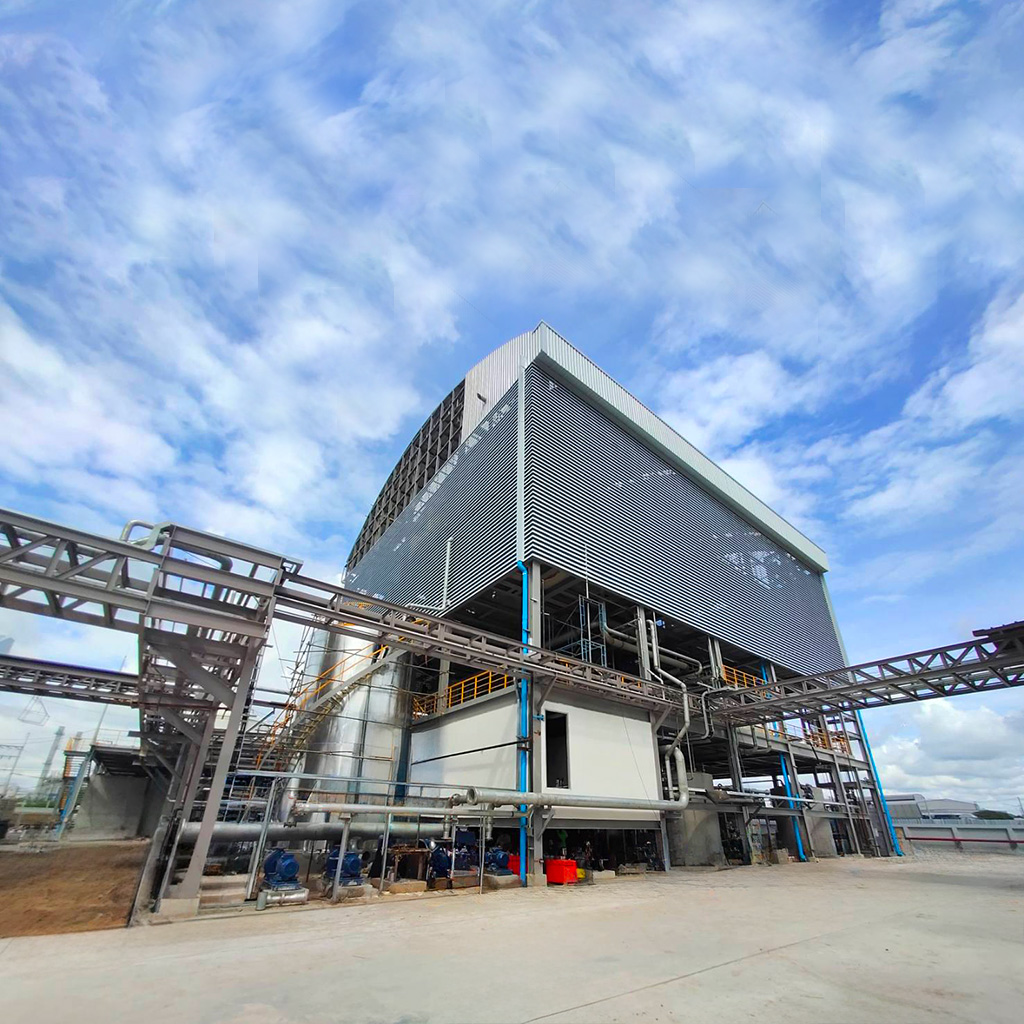
In the realm of chemical industrial equipment supply, precision and reliability are paramount. Changzhou Sanli Tech International Trade Co., Ltd. stands out by offering a diverse portfolio of equipment that meets the stringent requirements of chemical processing. Our product lineup includes a variety of pumps, such as centrifugal vertical/horizontal pumps, non-metallic pumps, and metering pumps, each designed to handle specific chemical properties and process conditions. For example, our non-metallic pumps are constructed from materials that resist corrosion, making them suitable for handling aggressive chemicals like acids and alkalis. A client in the chemical processing industry recently faced challenges with their existing pumps, which were failing due to corrosion. We supplied them with our non-metallic pumps, which not only resolved the corrosion issue but also improved the overall efficiency of their process. Beyond pumps, we also provide custom skid-mounted systems that integrate multiple components into a single, compact unit. These skids are designed for easy installation and maintenance, reducing the total cost of ownership. In another case, a client required a skid-mounted system for their new chemical production line. We designed and delivered a skid that included a pump, motor, and control system, all pre-assembled and tested, ensuring a smooth startup and minimal disruption to their operations. Our commitment to quality and customer satisfaction is reflected in every piece of equipment we supply, making us a trusted partner in the chemical industry.
Frequently Asked Questions

What personnel training courses does the company provide for chemical plants?

For operators, it covers equipment operation skills, process control, and safety rules through theory, demonstration, and practice. For technicians, it focuses on process optimization, equipment maintenance, and new technology application. For managers, it offers management knowledge training in production planning, quality, safety, and supply chain management.
It uses big data analysis to collect, analyze, and mine production data for process optimization, fault prediction, and quality improvement. Artificial intelligence algorithms enable intelligent control of production parameters. IoT technology allows remote monitoring and management of equipment, enabling engineers to check status, receive alarms, and perform operations remotely.
During factory design, it optimizes processes and equipment selection, like using efficient heat exchangers. In production, it uses advanced automation systems to adjust equipment parameters in real - time. It also offers energy management consulting to help establish monitoring and management systems for continuous energy efficiency improvement.
In chemical synthesis, it uses a 150L jacketed glass reactor for precise temperature control. For paint and varnish production, it employs basket mills for uniform particle size. For solid - liquid separation, it uses stirred nanofiltration filters for sealed handling of hazardous substances. It also uses stirred bead mill reactors for cleaner and safer molecular synthesis in continuous flow.

Related Articles

Analysis On Production Technology And Industrial Chain Of FM

28

Nov

Analysis On Production Technology And Industrial Chain Of FM

View More
Uses and Safety Precautions of Formaldehyde in Industry

23

Jul

Uses and Safety Precautions of Formaldehyde in Industry

Explore the industrial applications, safety measures, regulatory frameworks, and innovation trends of formaldehyde. Discover its role in resin production, healthcare disinfectants, wood composites, and alternatives like bio-based adhesives and low-VOC resins.
View More
The Role of Polymers in the Development of High - tech Industries

23

Jul

The Role of Polymers in the Development of High - tech Industries

Discover how polymer innovations are revolutionizing high-tech sectors, transforming manufacturing, sustainability, and technology applications. Explore the uses of photopolymers, high-performance polymers in aerospace, polyethylene glycol in drug delivery, and cutting-edge recycling methods for a greener future.
View More
The Intersection of Chemistry and Engineering in Production Technology

23

Jul

The Intersection of Chemistry and Engineering in Production Technology

Explore the transformative role of chemical engineering in production technology, digital transformation in chemical manufacturing using AI and IoT, sustainable material innovations, and future trends in polymer manufacturing and nanotechnology. Understand the significance of optimizing processes for efficiency and sustainability.
View More

Customer Reviews

Jennifer Lee

The delivery of the chemical industrial equipment was extremely fast. We placed an urgent order, and the company managed to ship it within the promised time frame. This quick response helped us avoid production delays and keep our operations running smoothly.

John Smith

The chemical industrial equipment supplied by this company is of top - notch quality. The materials used are durable and can withstand harsh chemical environments. The pumps, for example, have been running smoothly in our plant for a long time without any major issues. Highly recommended!

Get a Free Quote

Our representative will contact you soon.
Contact Us

Contact Us

Opting for Changzhou Sanli Tech International Trade Co., Ltd. means choosing professionalism and reliability! We offer a wide range of chemical products, including tower and internals, chemical industrial equipment, and various chemicals. Moreover, we possess advanced chemical production technologies, providing comprehensive services from process design to on-site operation guidance to fully meet your needs. Our team of experienced chemical technology experts can deliver customized technical support and consulting services. They help you optimize processes, reduce costs, and ensure environmental compliance and safety. In terms of energy-saving chemical plants and intelligent chemical engineering solutions, we keep pace with the times and utilize cutting-edge technologies to create efficient, intelligent, and energy-saving chemical production modes for you.