 EN
Quick Links
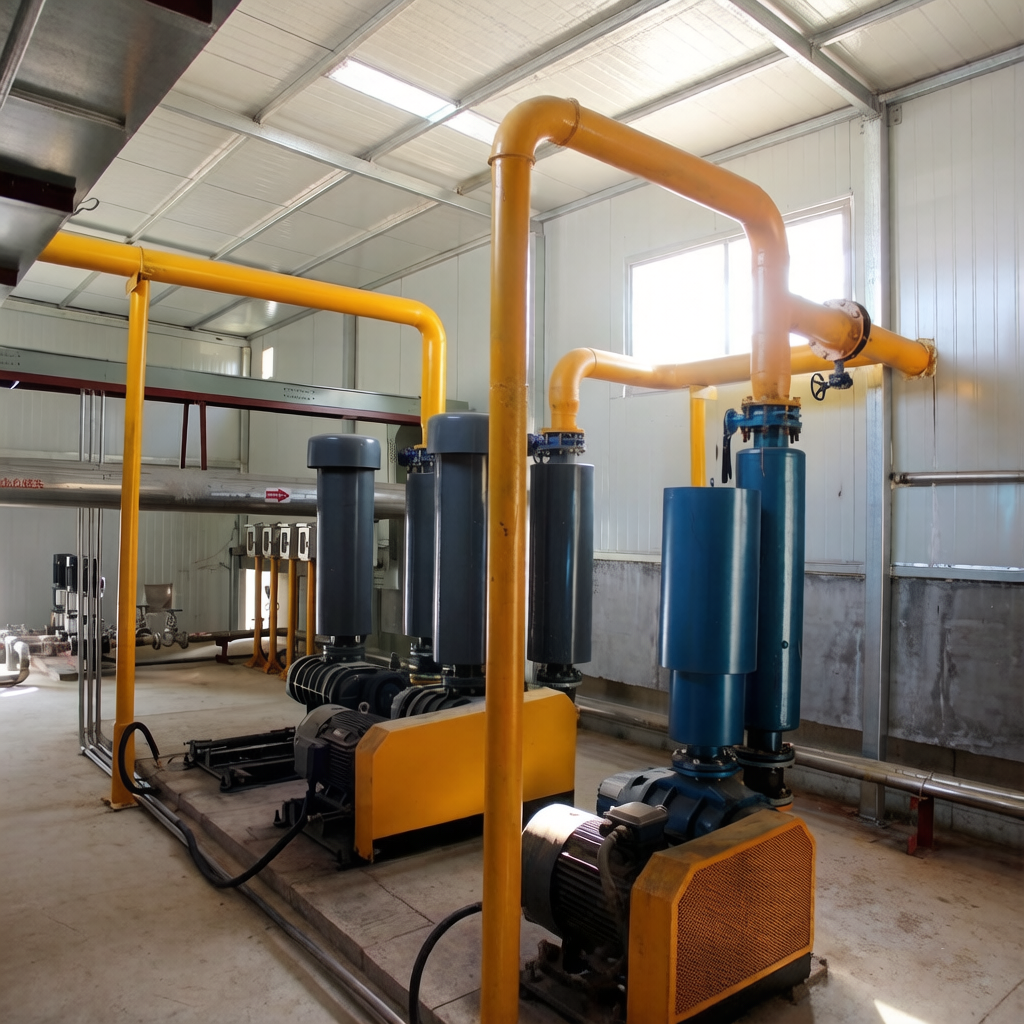
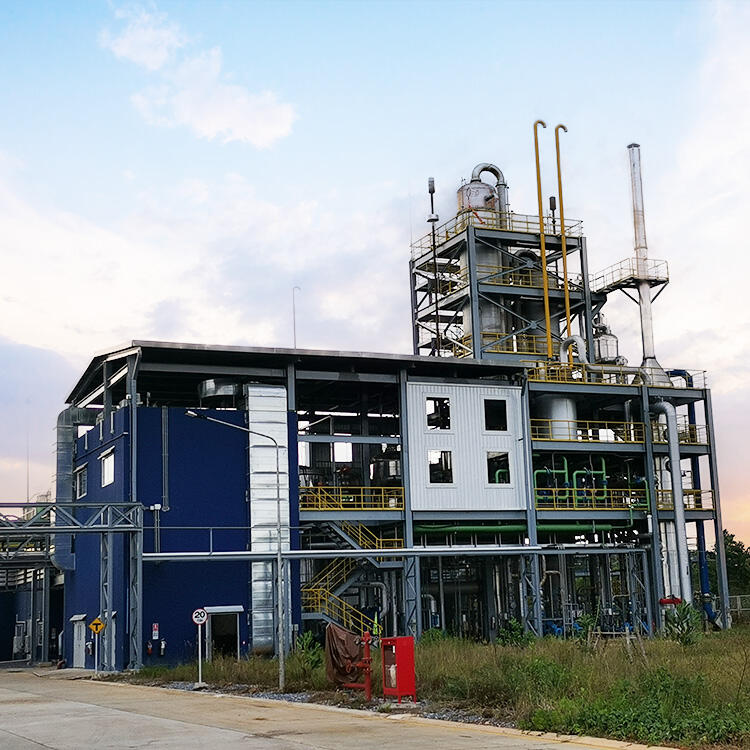
Our dedication to process intensification at Changzhou Sanli Tech International Trade Co., Ltd. is a direct reflection of our commitment to innovation and sustainability. We recognize that the chemical industry is under increasing pressure to reduce energy consumption and emissions, and we see process intensification as a primary means to achieve these goals without compromising productivity. For instance, in a Sulfuric Acid Plant, we can apply intensified technologies such as double absorption processes and advanced heat recovery systems that dramatically improve energy efficiency and reduce SO₂ emissions. In the production of specialty chemicals like Iso-Butyl Acetate, we can utilize membrane separation or reactive distillation to simplify the process and eliminate waste streams. Our approach to process intensification also enhances safety by reducing the volume of hazardous materials in process vessels at any given time. In a high-pressure Methanol Plant, this can mean designing smaller, more robust reactors that are inherently safer. By partnering with us, clients gain access to a technology provider that doesn't just build plants but actively engineers them to be smarter, safer, and more sustainable through the practical application of process intensification across a wide spectrum of chemical production technologies.
28
Nov
27
May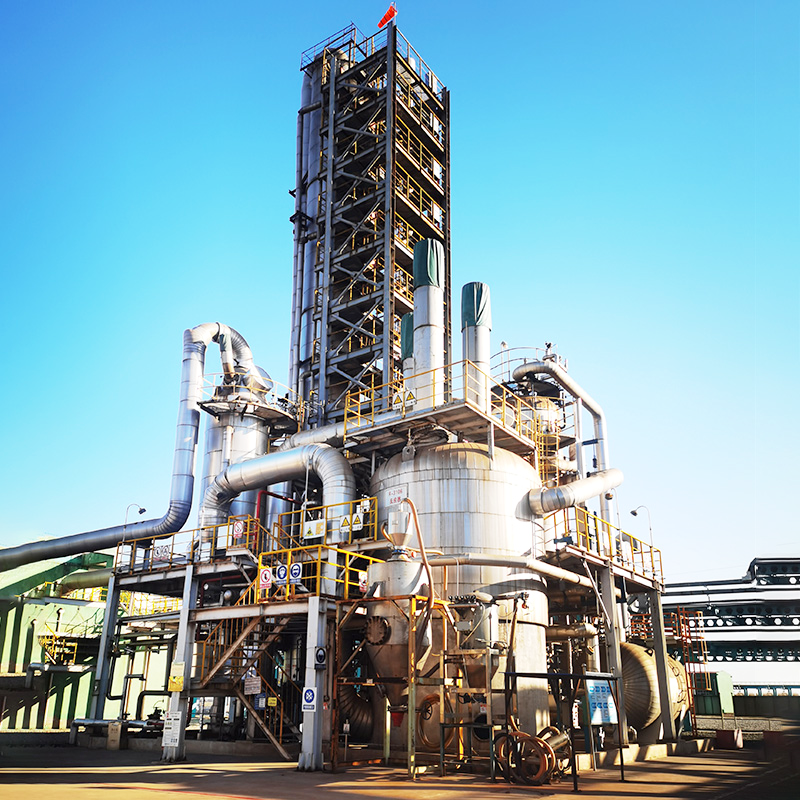
23
Jul