
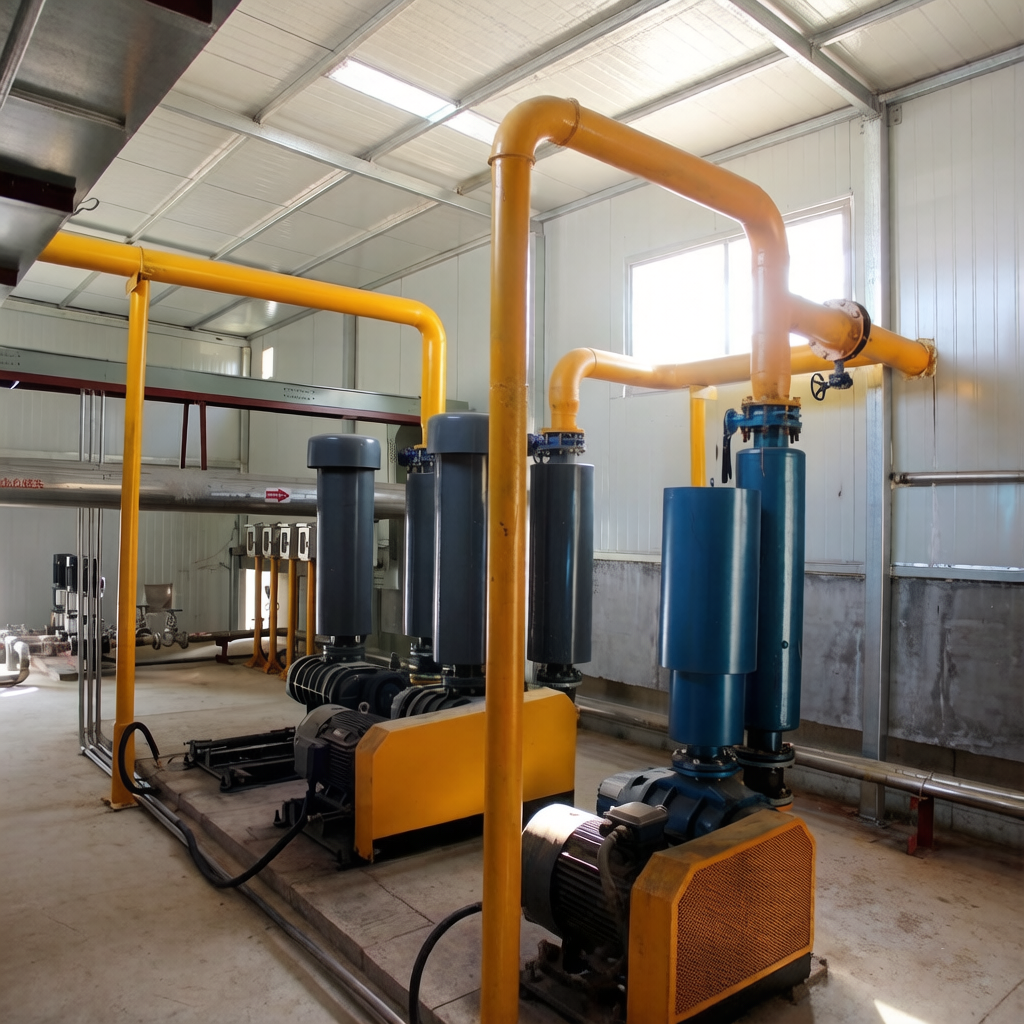
Process Intensification Solutions for Chemical Plants

All Categories
Innovative Process Intensification

Innovative Process Intensification

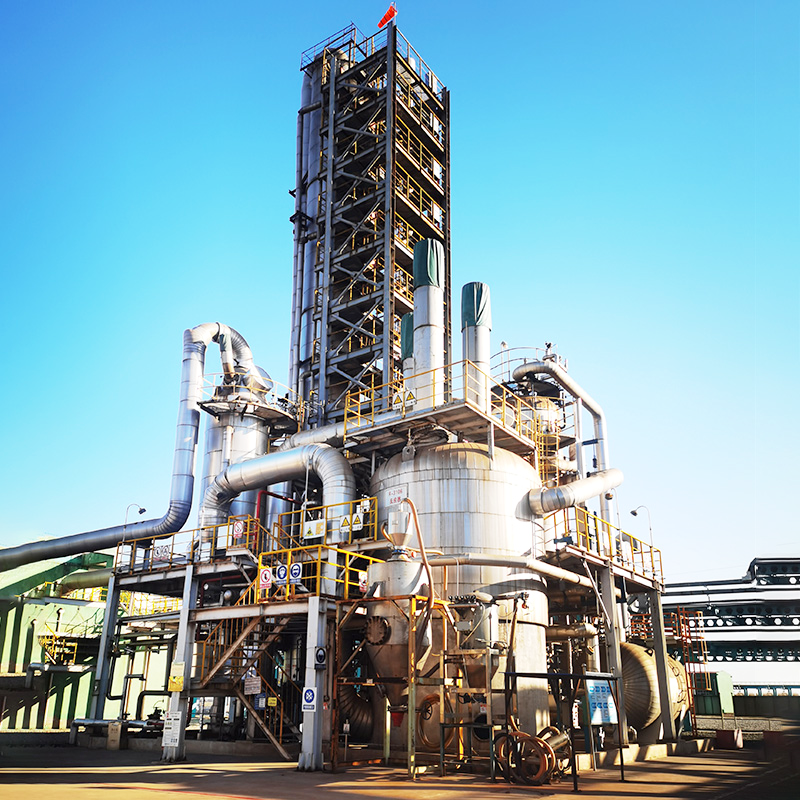
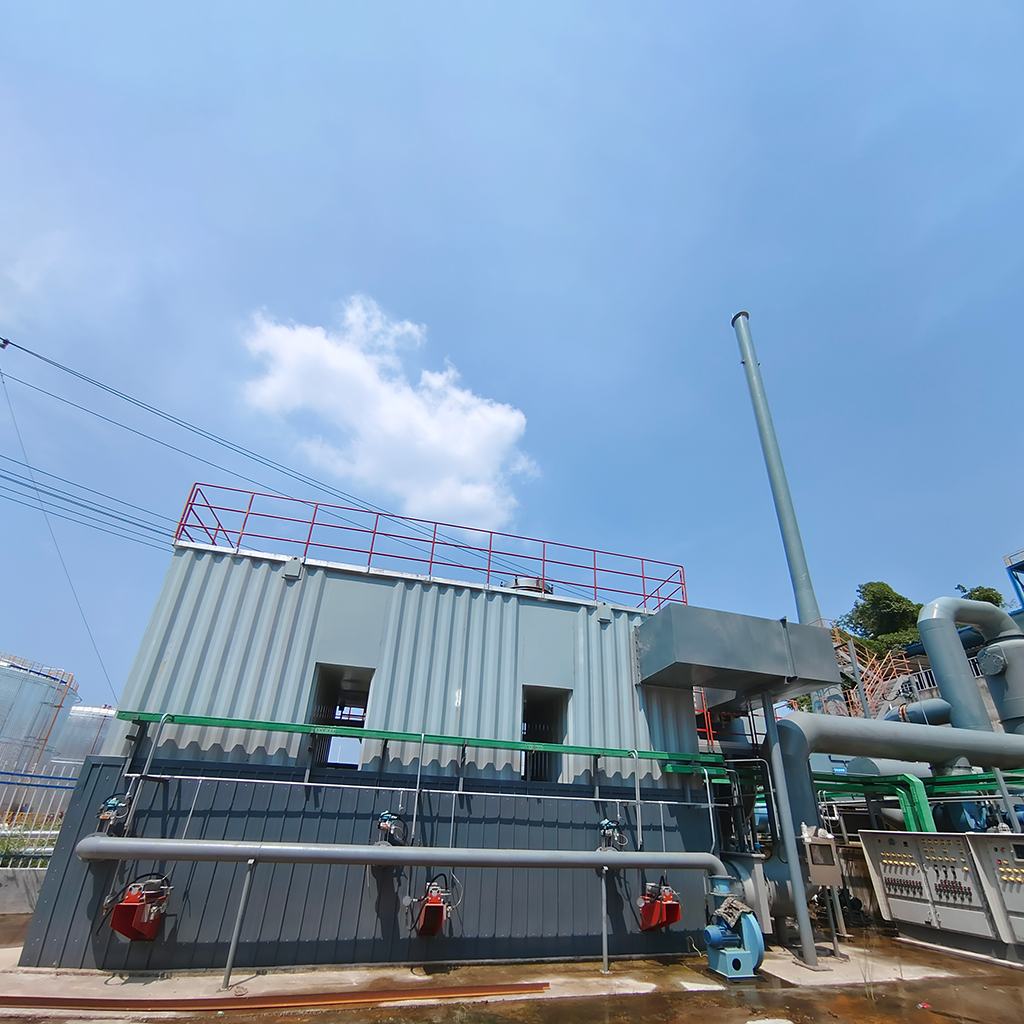
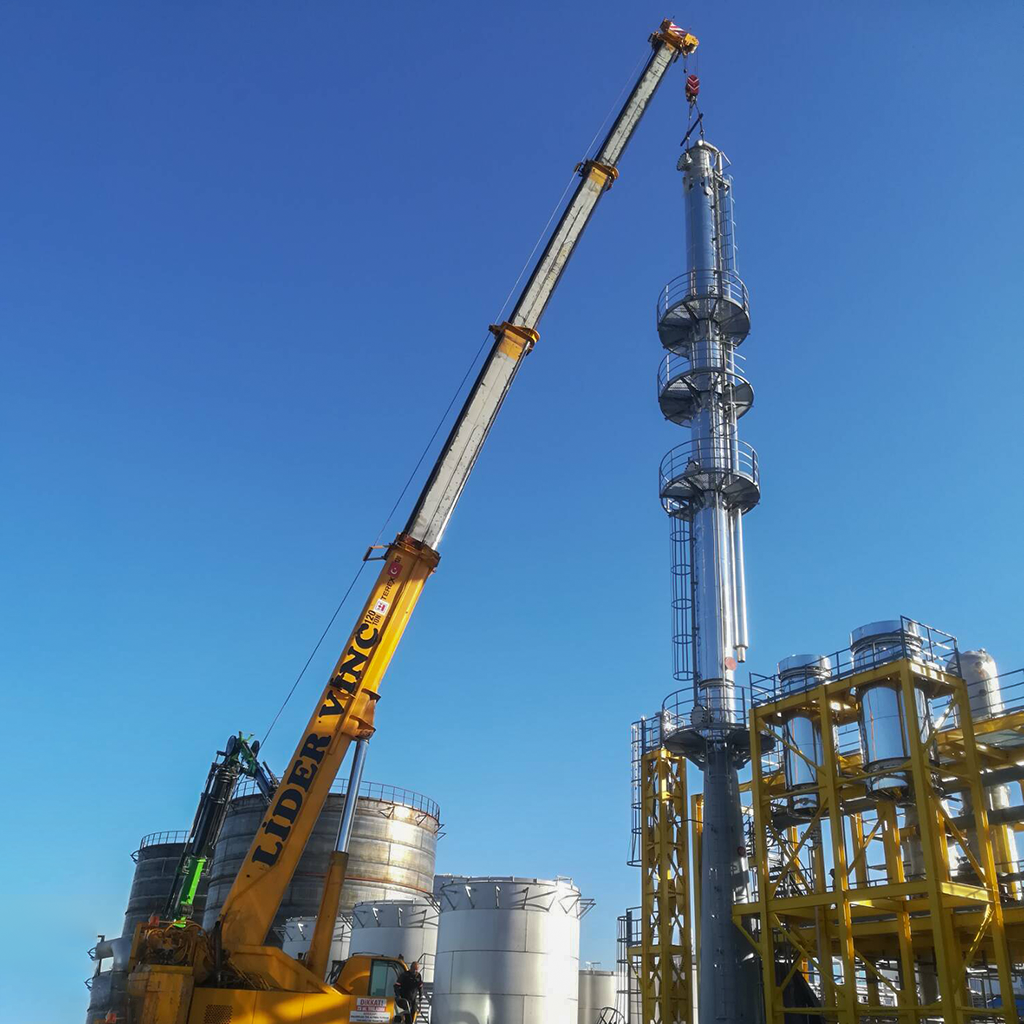
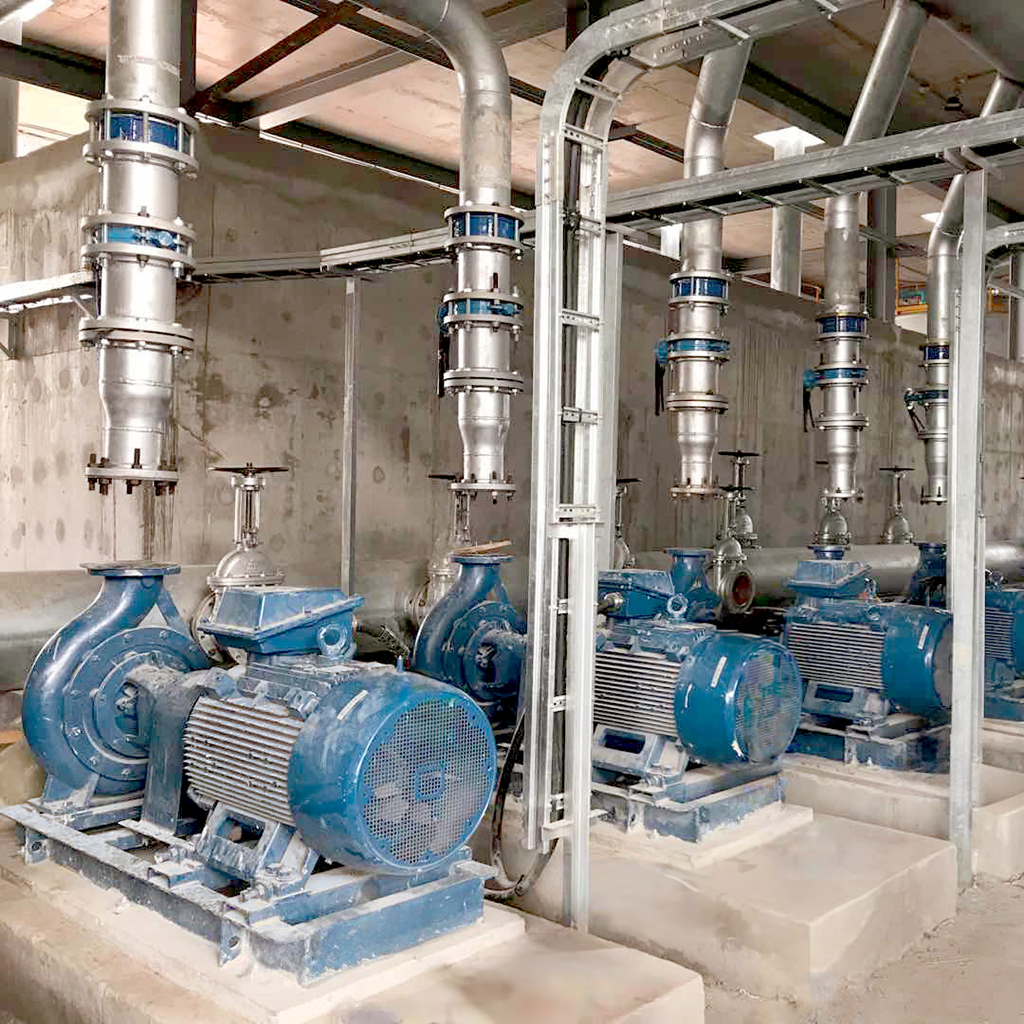
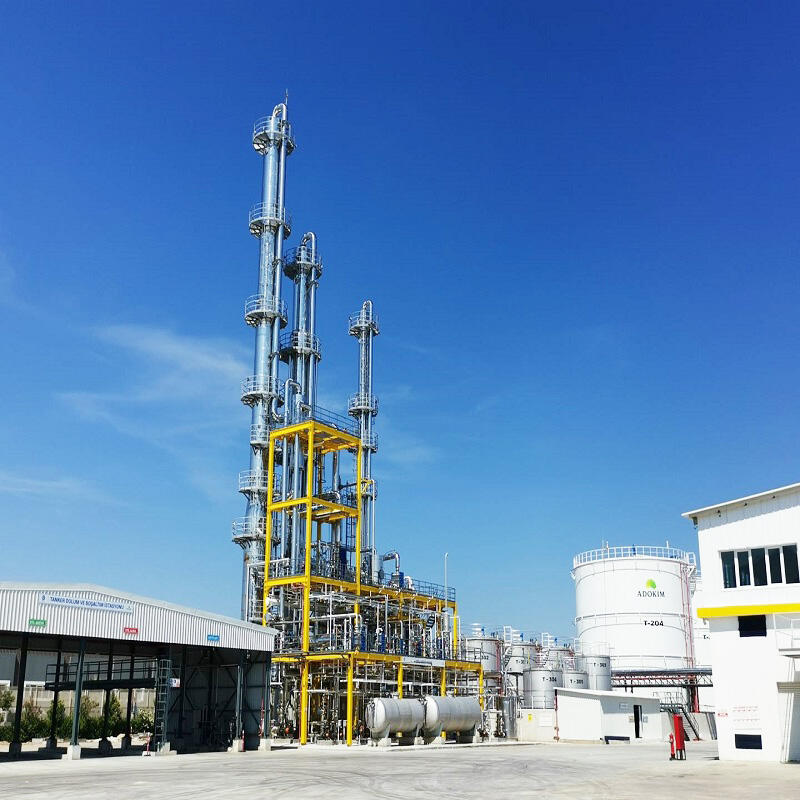
SL-TECH is at the forefront of process intensification, integrating novel concepts like reactive distillation and advanced mixing technologies into our plant designs. This innovative approach delivers superior performance for processes like Methylal and Ethyl Acetate production.
Get A Quote

Why choose us?

Resource-Efficient Production Routes

Our process intensification philosophy is evident in our plant designs for Methylamines and DMMn, where we develop resource-efficient routes that minimize byproducts and raw material consumption for a more sustainable operation.

Optimized Separation Technologies

By employing intensified separation technologies, such as in our spray dryer and vacuum rake dryer processes for Paraformaldehyde, we achieve higher product purity and production efficiency with reduced equipment footprint.

Advanced Catalyst and Process Integration

We integrate advanced catalytic processes, like the Fe-molybdenum and Silver methods for Formaldehyde, as a form of process intensification to maximize conversion rates and selectivity, leading to more compact and efficient plants.

Related products

Changzhou Sanli Tech International Trade Co., Ltd. leverages process intensification to overcome traditional trade-offs between capital cost, operating cost, and safety in chemical plant design. Our engineering teams are skilled in identifying opportunities to replace conventional, large-scale equipment with innovative, multifunctional units that deliver multiple process benefits simultaneously. For a complex process like a Bisphenol-A Plant, we can apply intensified crystallization and separation technologies that yield high-purity product with fewer processing steps, reducing the overall equipment count and simplifying the plant layout. In the production of Hexamine via the Gas Phase Process, we utilize intensified reactor designs that achieve high conversion rates in a single pass, eliminating the need for large recycle loops and associated equipment. Process intensification also plays a critical role in our new materials offerings. For the UHMWPE (Ultra High Molecular Polyethylene) Plant, we have developed intensified reactor systems that ensure precise temperature and mixing control, which is crucial for achieving the target molecular weight and particle size distribution. By deploying these intensified solutions, we help our clients achieve a more rapid return on investment, reduce their carbon footprint, and operate safer, more responsive plants that can adapt quickly to changing market demands.
Frequently Asked Questions

How do your instrumentation and control systems enhance plant operation?

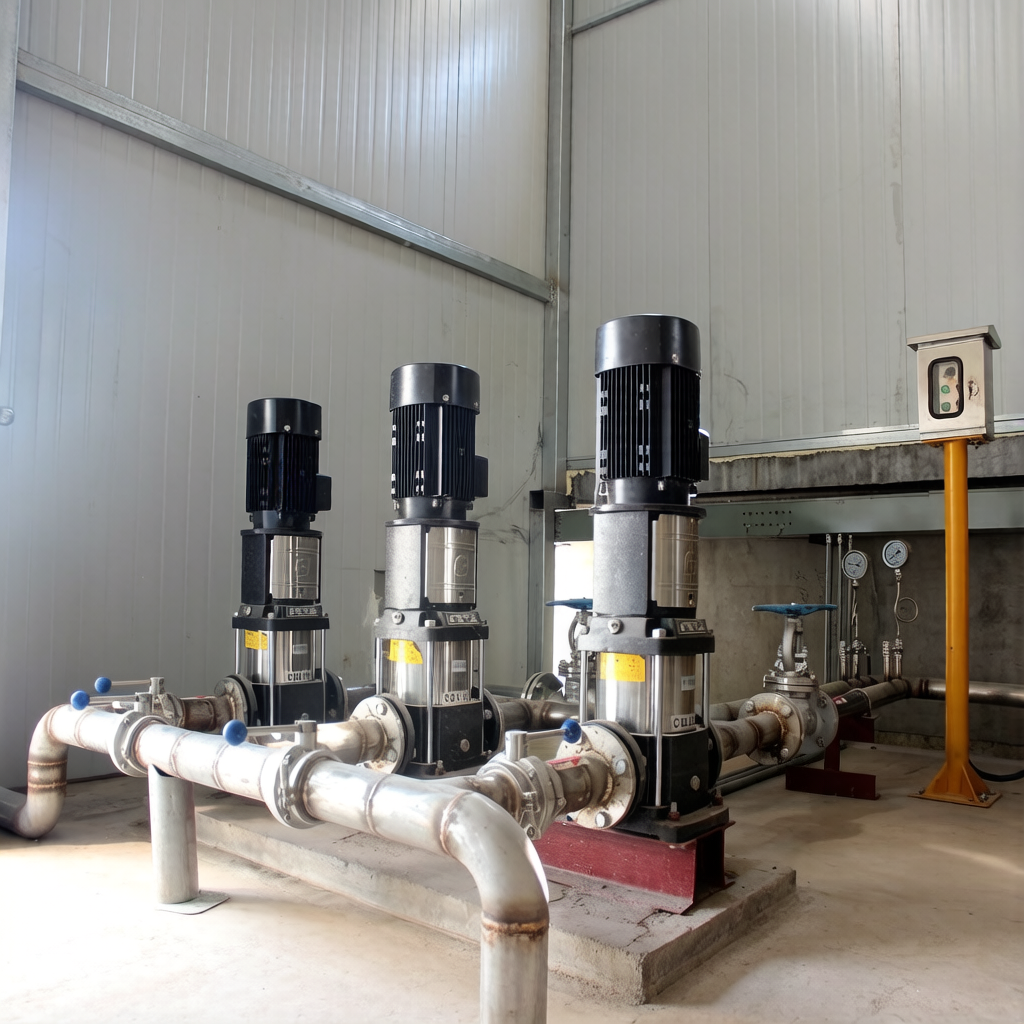
We design and implement advanced instrumentation and control systems as the central nervous system of the plant. This includes a robust Distributed Control System (DCS) and independent Safety Instrumented Systems (SIS) for precise control, safe operation, and real-time data monitoring, enabling operators to optimize performance and maintain product quality.
Yes, we offer comprehensive chemical process design and licensing services. Our licensing package includes a detailed process engineering package (PEP) with all the data needed to design and build the plant. We also provide technical support during engineering, procurement, and commissioning to ensure a successful technology transfer.
Skid-mounted modular plants are pre-fabricated and pre-tested in a controlled factory environment. This approach significantly reduces on-site construction time, minimizes site-related risks, and ensures high quality. They are ideal for fast-track projects, remote locations, or brownfield sites where space is limited.
Our turnkey service provides a single point of responsibility for your entire project. We manage everything from the initial engineering design and procurement of all equipment to construction, installation, commissioning, and start-up. This streamlines the process, reduces your project management burden, and ensures a seamless transition to full operation.

Related Articles

Polysulfone: The Star Performer in Advanced Engineering Plastics

03

Mar

Polysulfone: The Star Performer in Advanced Engineering Plastics

View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
The Role of Polymers in the Development of High - tech Industries

23

Jul

The Role of Polymers in the Development of High - tech Industries

Discover how polymer innovations are revolutionizing high-tech sectors, transforming manufacturing, sustainability, and technology applications. Explore the uses of photopolymers, high-performance polymers in aerospace, polyethylene glycol in drug delivery, and cutting-edge recycling methods for a greener future.
View More
Formic Acid: The Small Molecule Driving a Global Industry

22

Dec

Formic Acid: The Small Molecule Driving a Global Industry

View More

Customer Reviews

William Grant

The process intensification strategies used by Sanli Tech in our DMC (Dimethyl Carbonate) plant have improved both safety and efficiency. By minimizing in-process inventory and enhancing mixing in the reactor, they created a safer environment while achieving high conversion rates. The plant’s performance demonstrates the tangible benefits of their engineering philosophy.

Javier Fernandez

Sanli Tech used an intensified reactive distillation design for our Ethyl Acetate plant. This innovation combines reaction and separation, significantly reducing equipment count and energy use. The plant achieves high purity with a simpler process flow. It was a cost-effective and efficient solution that met all our production targets.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/Whatsapp
Name
Company Name
Message
0/1000
Innovative Process Intensification For Efficiency And Safety

Innovative Process Intensification For Efficiency And Safety

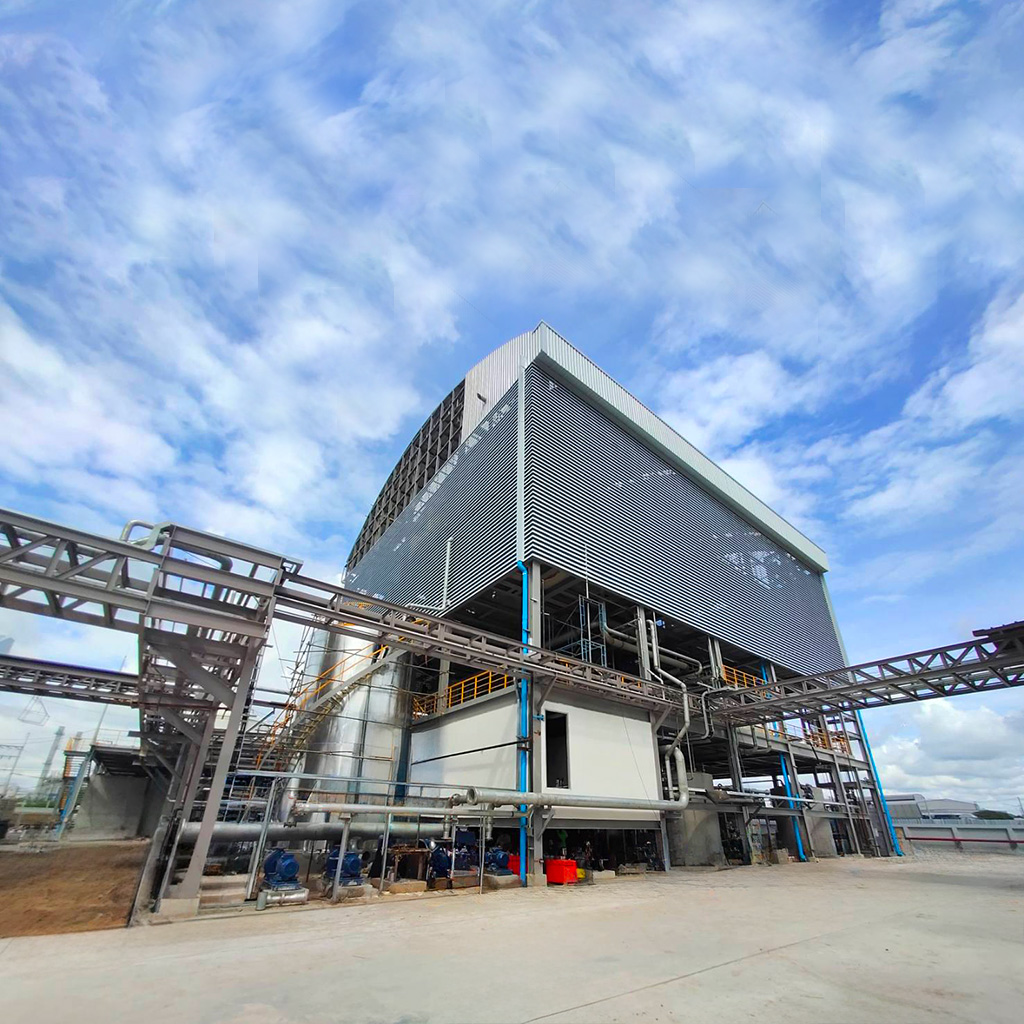
We embed process intensification principles into every design to create plants that are more efficient, safer, and more sustainable. Our solutions include intensified reactive distillation, advanced heat integration, and compact reactor designs that reduce footprint, lower energy consumption, and minimize in-process inventory, leading to significant operational cost savings.