
Chemical Plant Supplier | Scalable, Turnkey Solutions

All Categories
Quality-Focused Chemical Plant Supplier

Quality-Focused Chemical Plant Supplier

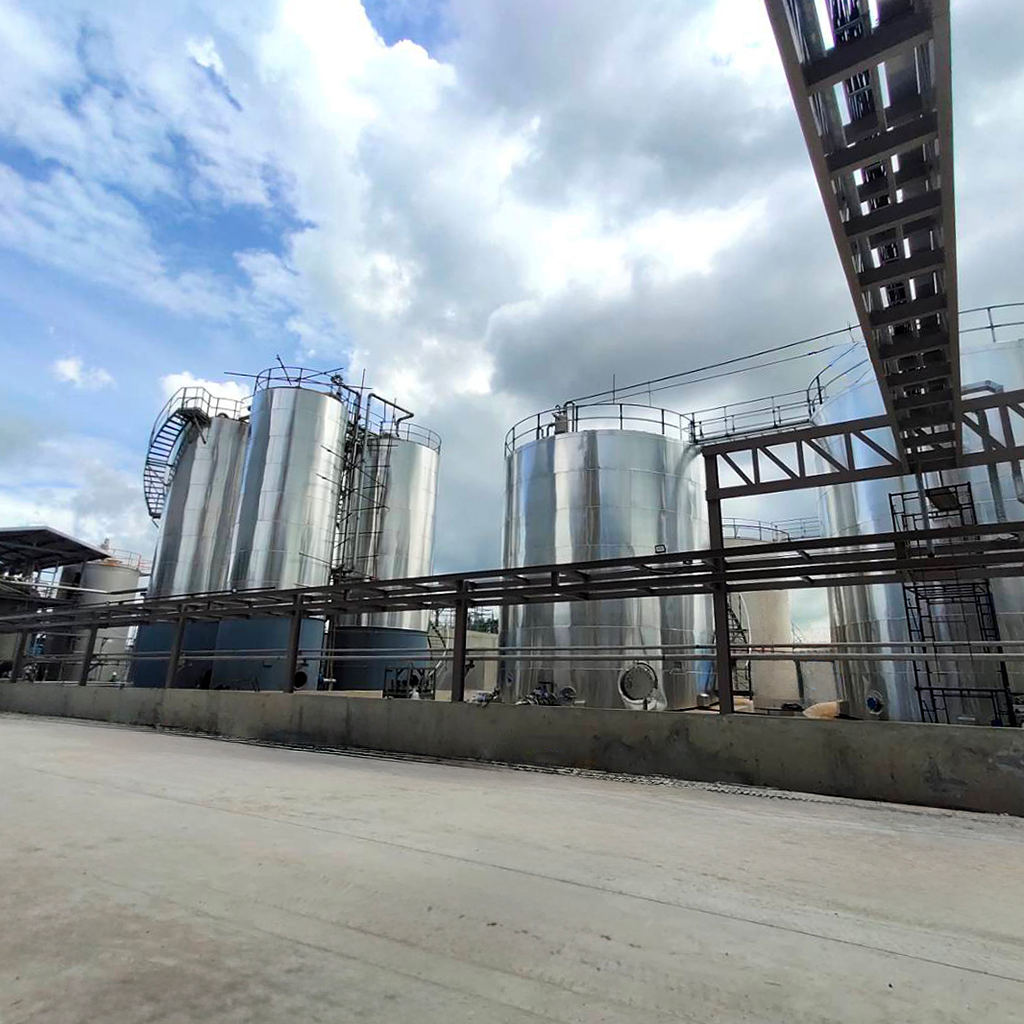
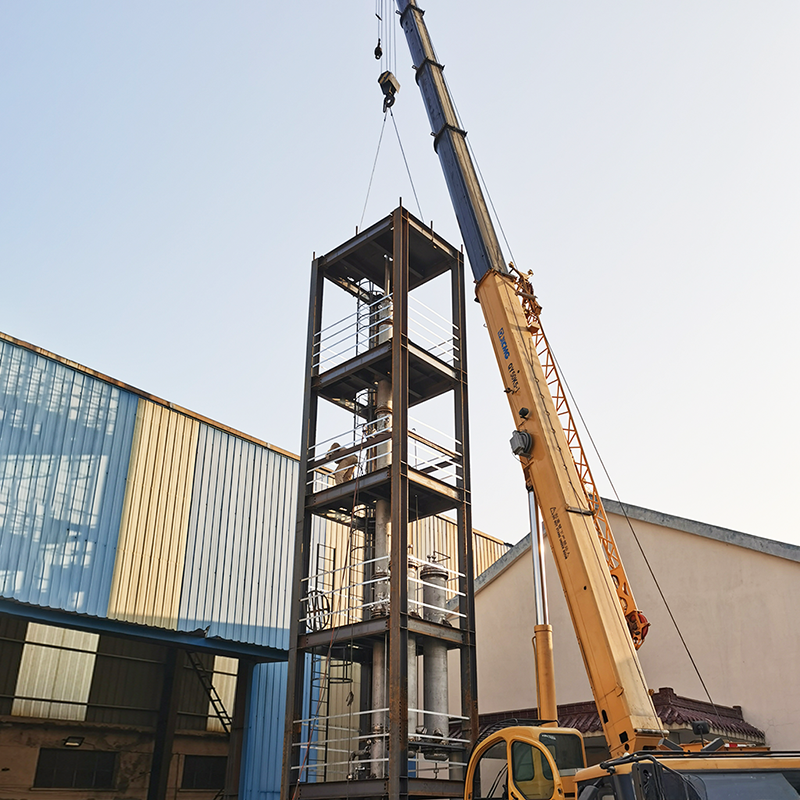
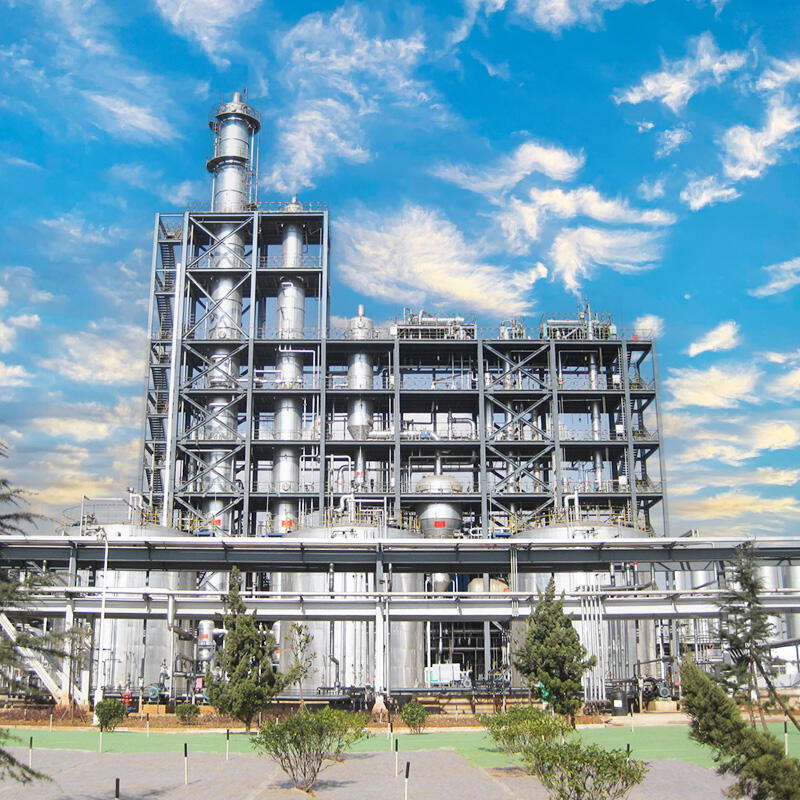
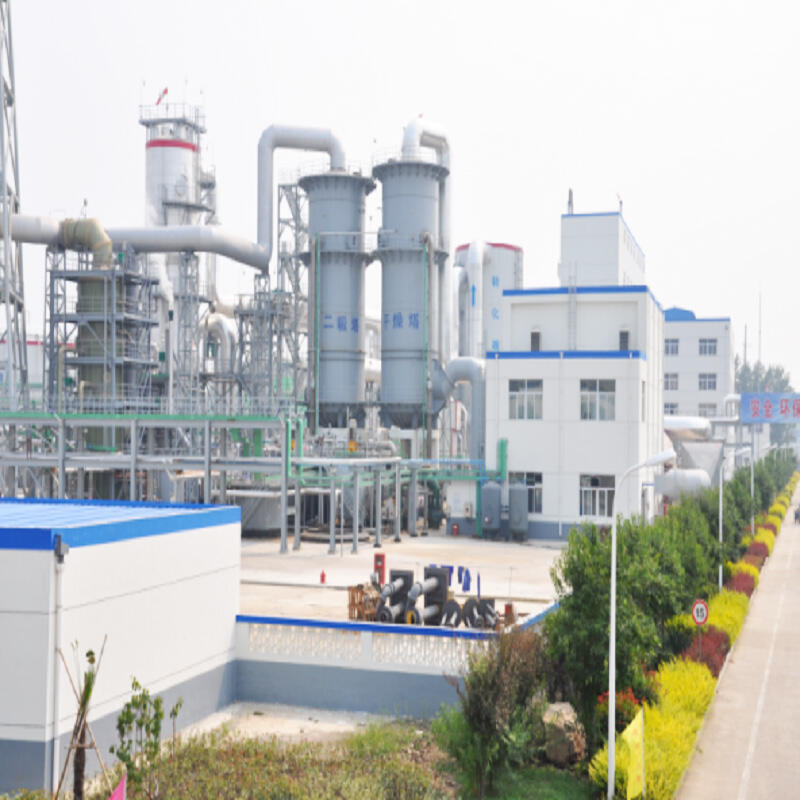
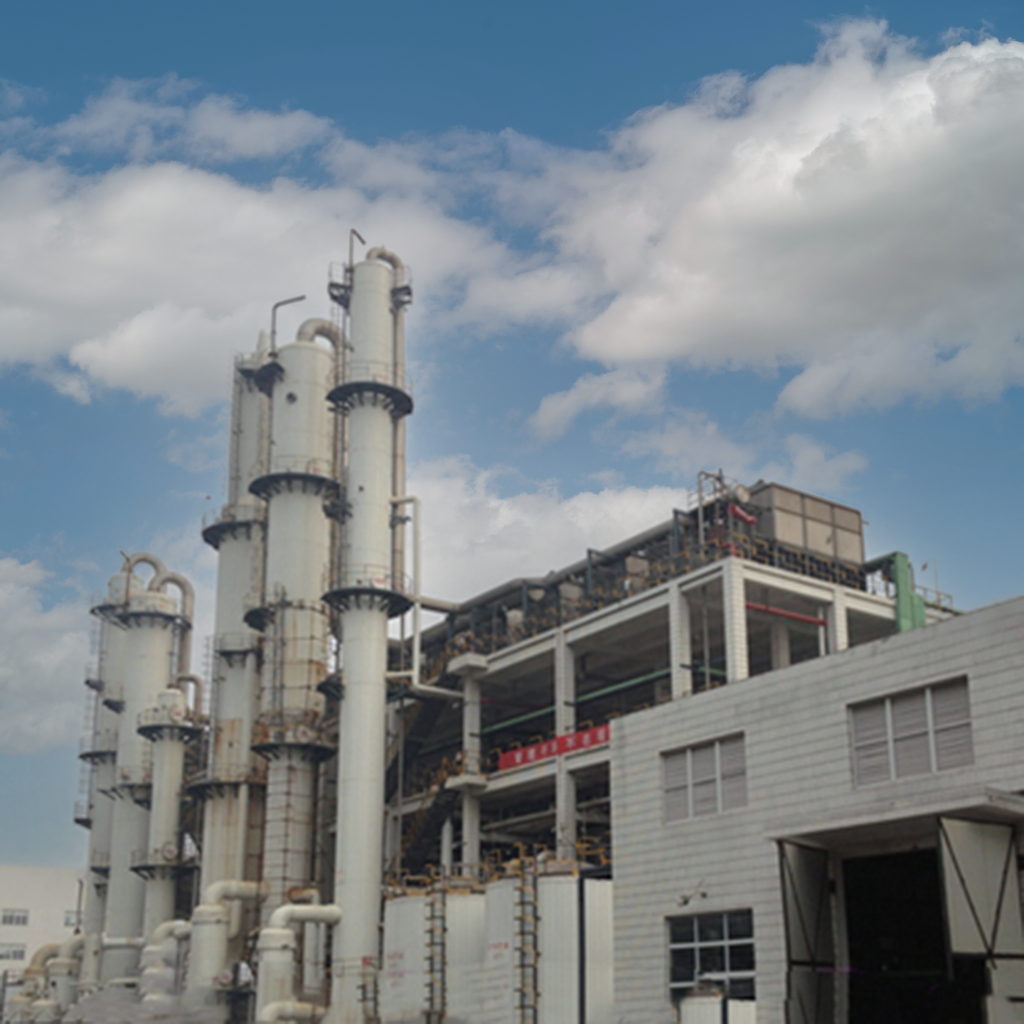
Quality is our priority. As a chemical plant supplier, SL-TECH adheres to the highest standards in engineering, equipment procurement, and construction, ensuring your plant is built for long-term reliability and safety.
Get A Quote

Why choose us?

Delivering Complete, Operational Chemical Plants

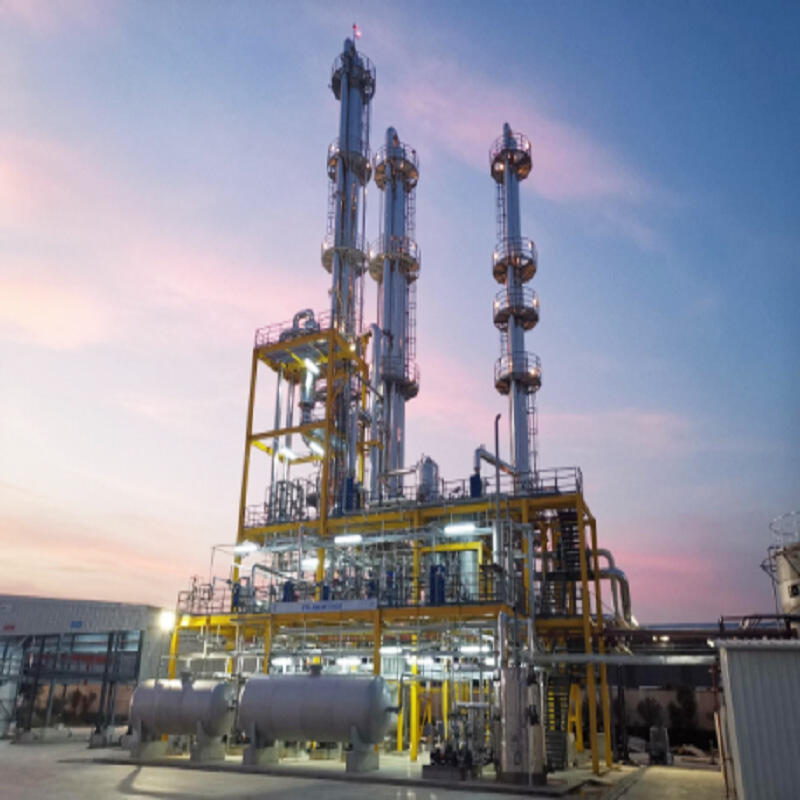
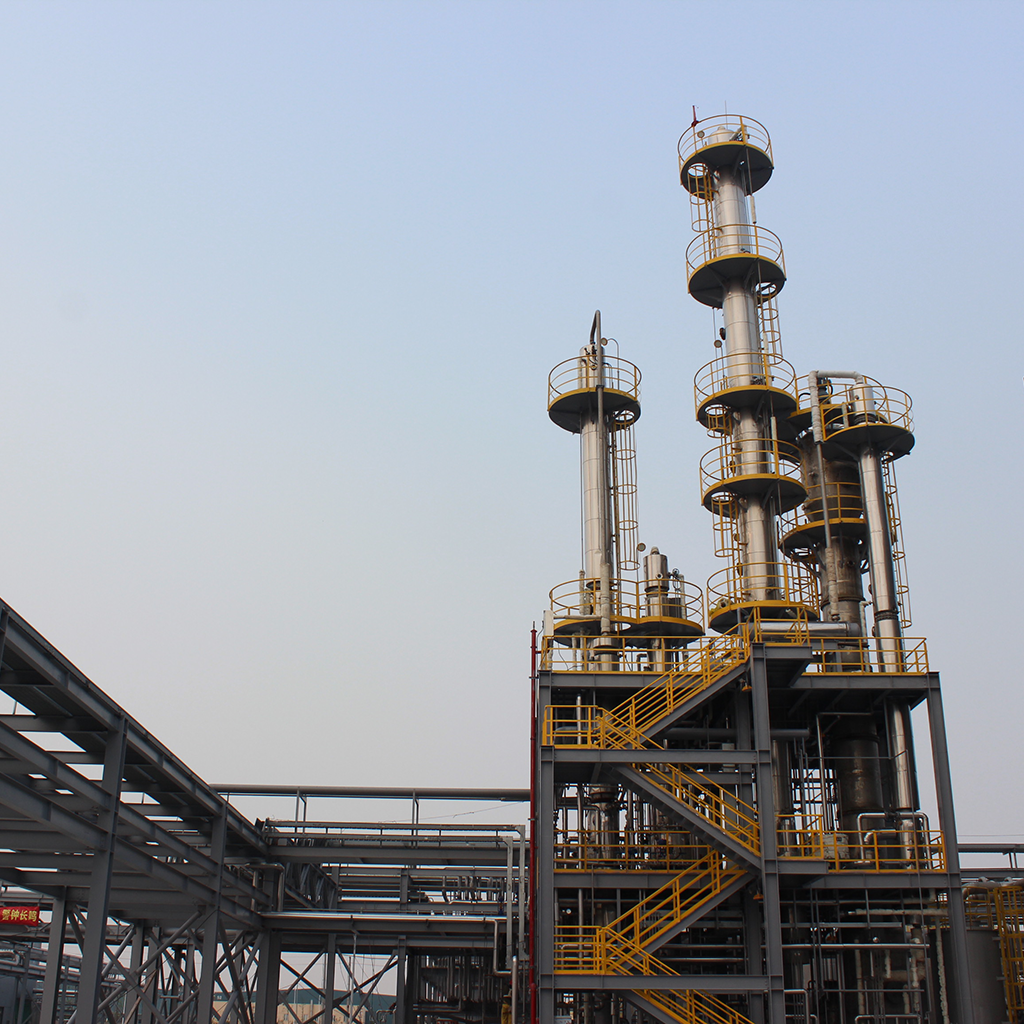
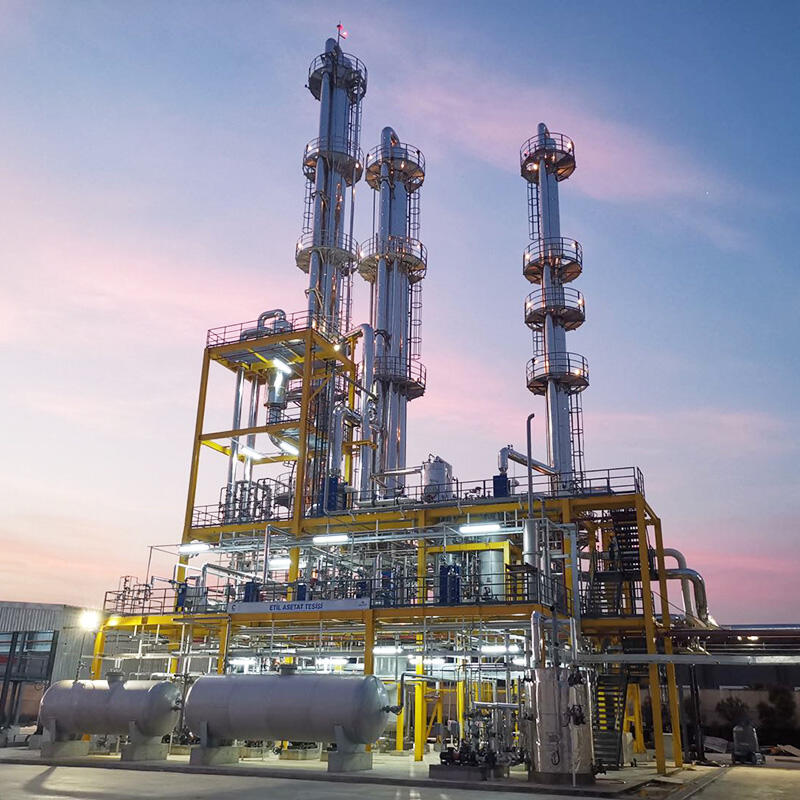
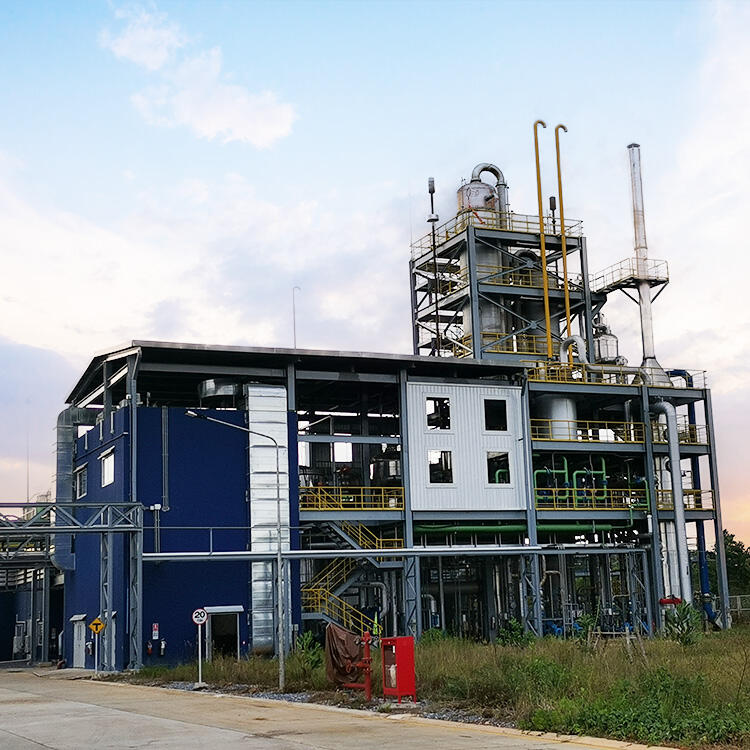
As a chemical plant supplier, we deliver more than just equipment; we provide complete, operational plants designed and built to produce specific chemicals like Formic Acid, MMA, or DMC, ready for start-up.

One-Stop Service from Design to Training

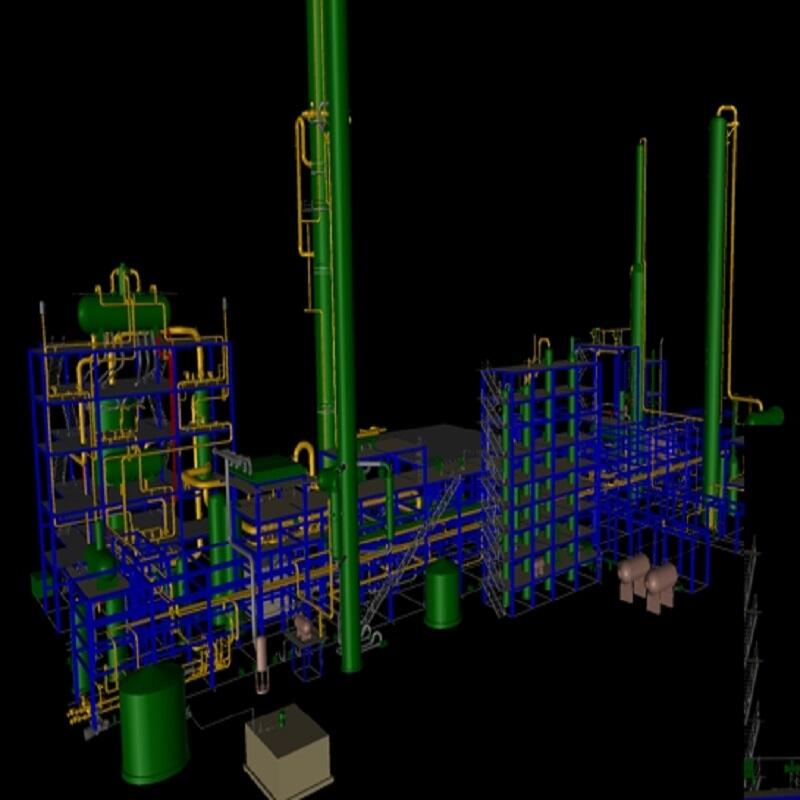
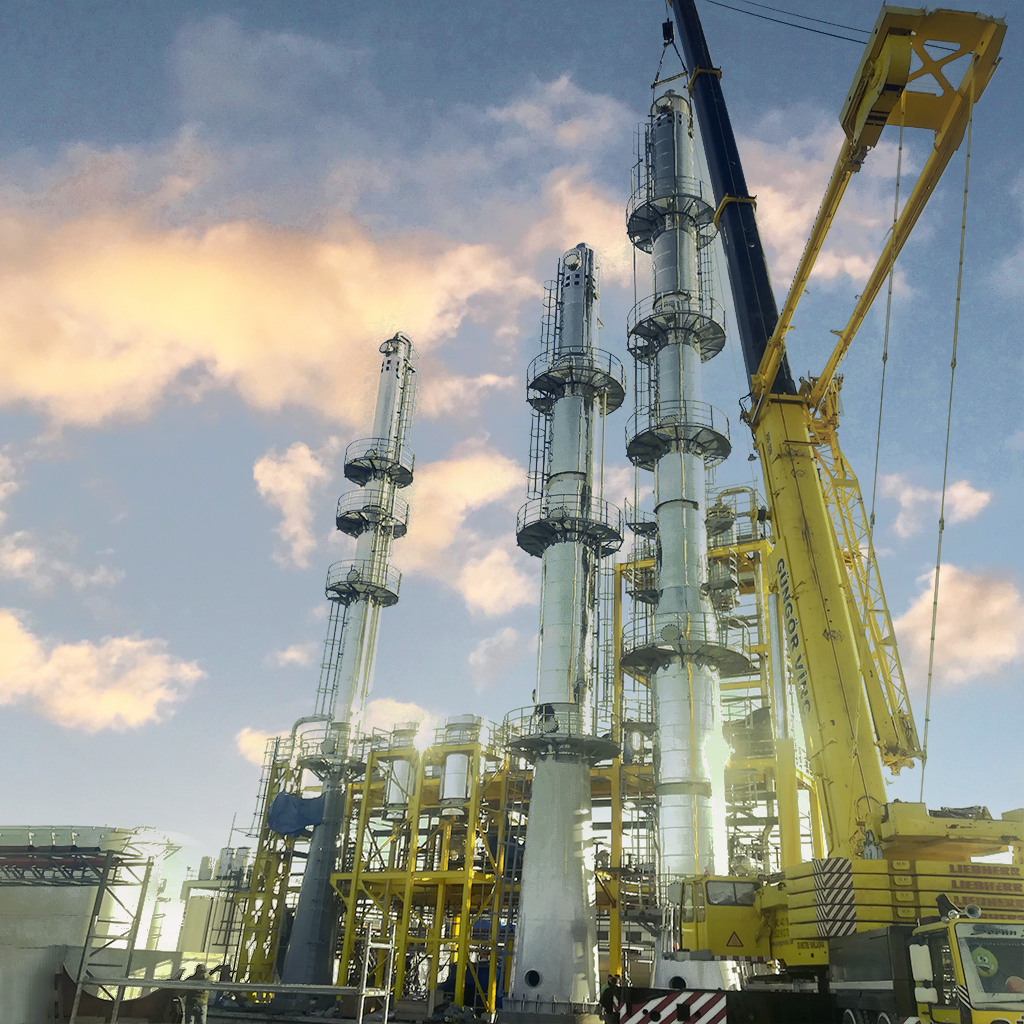
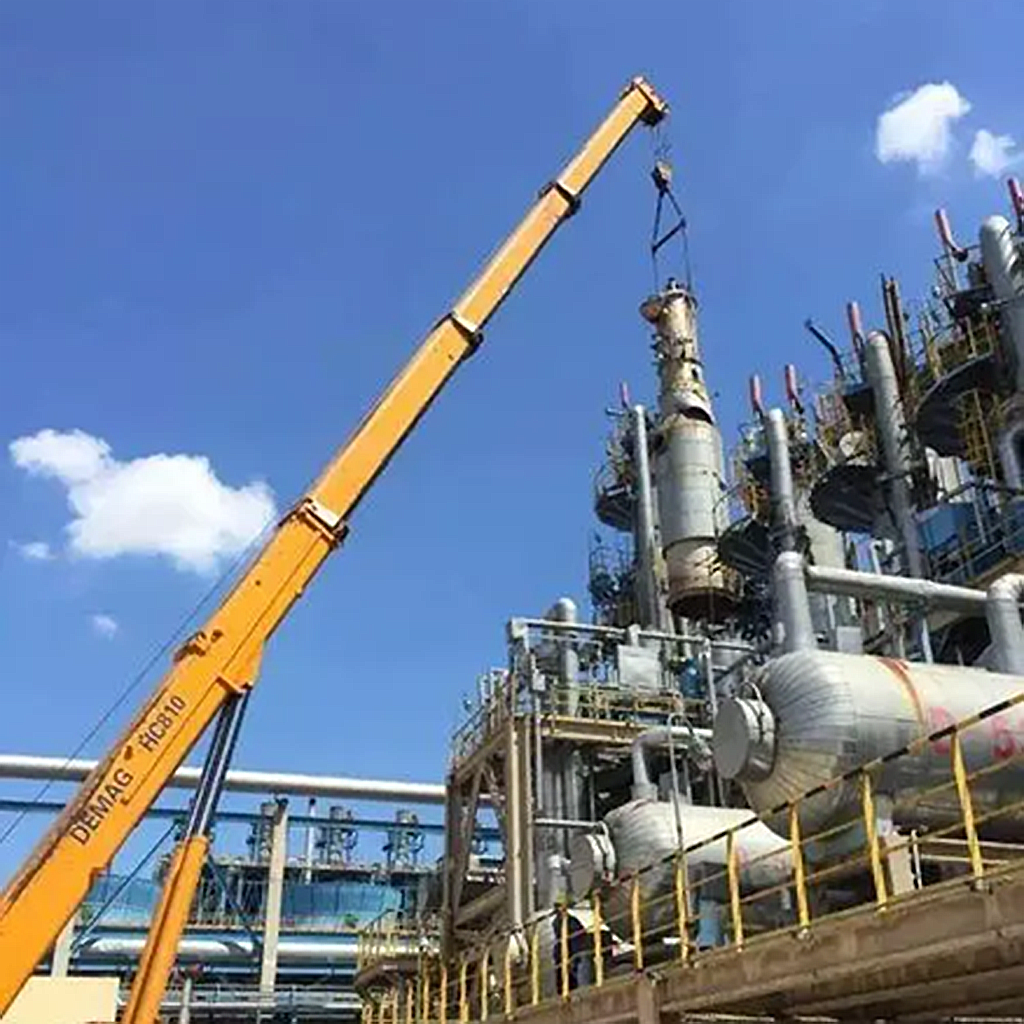
We supply chemical plants as part of our one-stop service model, taking responsibility for engineering design, procurement, installation, commissioning, and training, so you receive a fully functional facility with a single point of contact.

Tailored Solutions for Diverse Chemical Needs

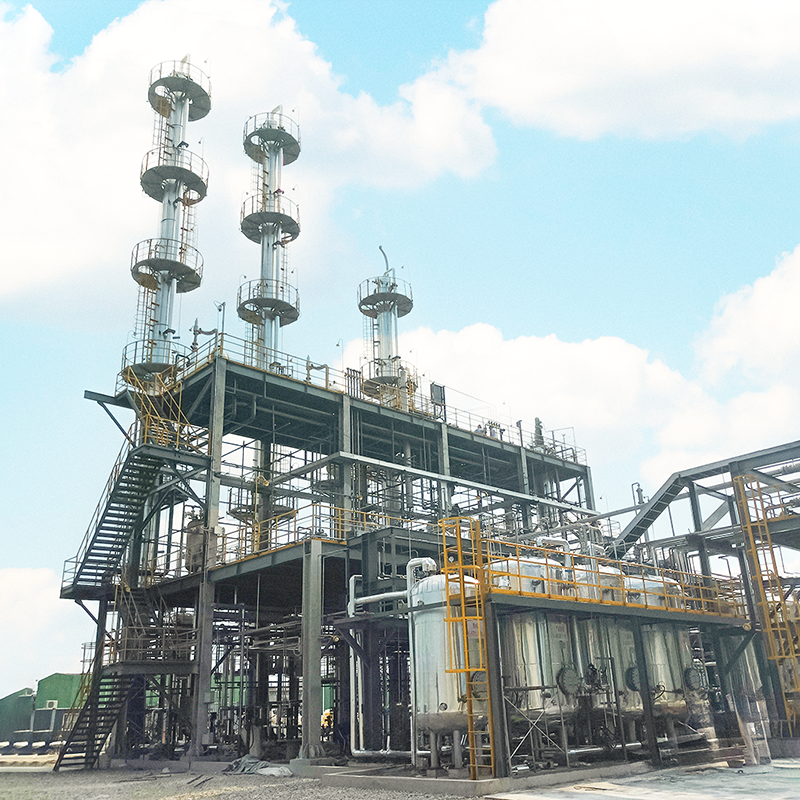
We supply chemical plants tailored to a wide range of chemical needs, from large-scale Methanol and Ethylene Oxide plants to specialized units for Methylal and Bisphenol-A, providing custom solutions for any project scale.

Related products

At Changzhou Sanli Tech International Trade Co., Ltd., our role as a chemical plant supplier is defined by our commitment to delivering comprehensive, high-quality, and reliable manufacturing solutions. We understand that building a chemical plant is a complex undertaking, and our supply service is designed to simplify this process for our clients. We offer a complete package that includes our proprietary chemical technology, the necessary engineering design, and all the equipment required to build and operate the plant. For a client in the Ketones industry, we can act as the supplier for a complete MEK (Methyl Ethyl Ketone) Plant, providing everything from the reactor system to the final distillation columns. Our supply chain management ensures that all components, whether fabricated locally or sourced globally, meet the highest quality standards and are delivered on time. We also provide comprehensive installation and commissioning services, ensuring that the plant is handed over as a fully operational facility. Our project management team works closely with the client throughout the process, providing regular updates and ensuring that all milestones are met. By choosing us as your chemical plant supplier, you are partnering with a company that is dedicated to delivering a successful project outcome, backed by years of experience and a commitment to excellence.
Frequently Asked Questions

What is your company’s background and R&D capability?

Headquartered in Changzhou since 2015, we are a specialized and innovative enterprise. We have research and development centers in Tianjin, Qingdao, and Shanxi, and have established a strong collaboration with the Institute of Process Engineering of the Chinese Academy of Sciences. This partnership fuels our continuous innovation in chemical technology.
Yes, we are a one-stop partner providing comprehensive services. Our offerings include system integration and full process development. We cover solution communication and consulting before sale, procurement and installation during plant construction, commissioning, and personal training for your team after the plant is completed.
We have successfully set up chemical plants in over 9 cities, demonstrating our strong project execution capabilities. Our experience spans both greenfield and brownfield projects, and we have a proven track record of delivering reliable plants that run smoothly and add significant value to our customers’ operations.
As a global vendor for critical applications, we have a rigorous supplier qualification process. Our mechanical engineers develop detailed equipment specifications, and we partner with reputable manufacturers worldwide. We manage the entire procurement chain, including expediting and inspection, to ensure all equipment meets the highest quality and safety standards.

Related Articles

Analysis On Production Technology And Industrial Chain Of FM

28

Nov

Analysis On Production Technology And Industrial Chain Of FM

View More
Polysulfone: The Star Performer in Advanced Engineering Plastics

03

Mar

Polysulfone: The Star Performer in Advanced Engineering Plastics

View More
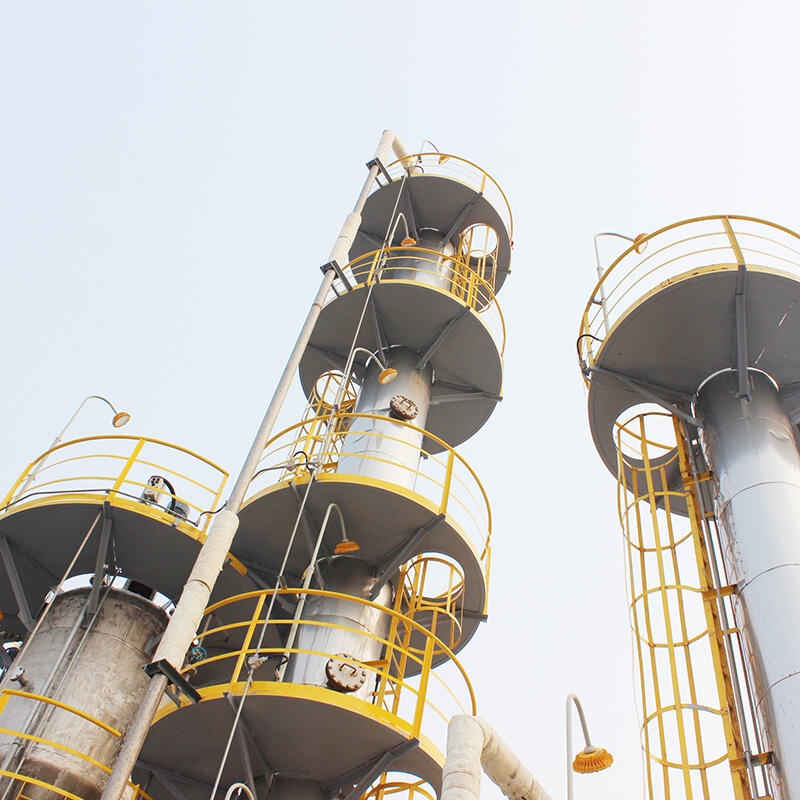
Key Considerations When Choosing Tower and Internals for Chemical Plants

23

Jul

Key Considerations When Choosing Tower and Internals for Chemical Plants

Explore the essential aspects of material compatibility in chemical plant towers, focusing on formaldehyde and ethylene glycol reactions, corrosion resistance, and process-specific design. Learn about sustainability practices and regulatory compliance in chemical processing operations.
View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More

Customer Reviews

Miguel Angel Fernandez

Sanli Tech is our trusted chemical plant supplier for skid-mounted modular units. They have supplied us with multiple Methylal plants. The modular approach, combined with their reliable supply chain, has allowed us to quickly and cost-effectively expand our production capacity to meet growing market demand.

James Wilson

As a chemical plant supplier, Sanli Tech delivered a complete MMA plant for us. Their scope included the technology, engineering, and all equipment. The plant’s performance has been outstanding, and the handover process was smooth. They are a reliable supplier we would work with again.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/Whatsapp
Name
Company Name
Message
0/1000
Premier Chemical Plant Supplier Delivering Complete Solutions

Premier Chemical Plant Supplier Delivering Complete Solutions

As a premier chemical plant supplier, we deliver more than just equipment; we provide complete, integrated manufacturing solutions. Our supply includes technology, engineering, equipment, and project management. This comprehensive approach ensures you receive a fully coordinated, high-quality facility that is ready to operate and deliver value from day one.