
Chemical Production Solutions | 178+ Plants Delivered

All Categories
Reliable Chemical Production Solutions for Global Clients

Reliable Chemical Production Solutions for Global Clients

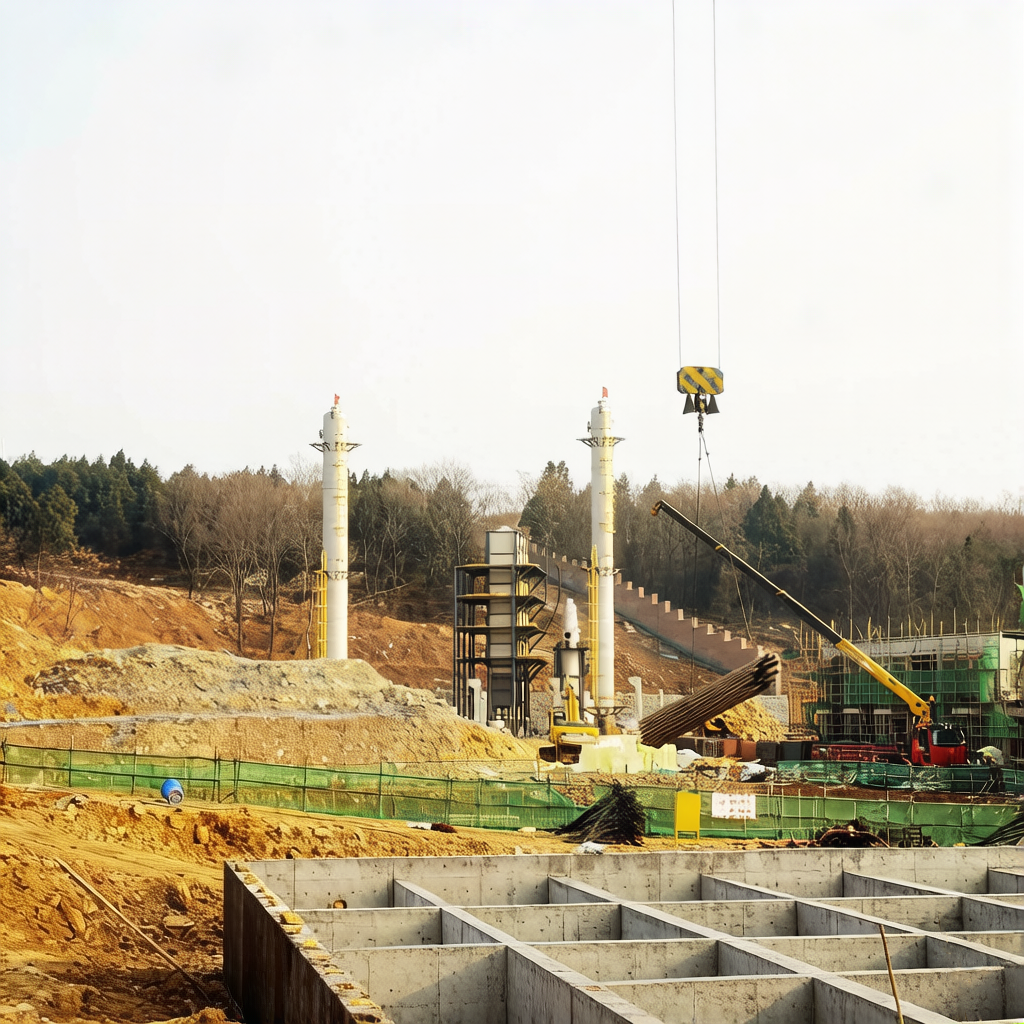
With over 178 complete sets of technology delivered, SL-TECH is a trusted global vendor. Our chemical production solutions are backed by extensive R&D and academic partnerships, guaranteeing robust, scalable, and proven processes for essential industries worldwide.
Get A Quote

Why choose us?

Advanced R&D Backed by CAS

Our chemical production solutions are developed in collaboration with the Institute of Process Engineering of the Chinese Academy of Sciences, ensuring cutting-edge technology and reliable process fundamentals for your plant.

Comprehensive C1 to New Materials Portfolio

We offer integrated chemical production solutions across a vast range of industries, from Methanol (C1) and Ethylene (C2) derivatives to high-value New Materials like Polysulfone and UHMWPE, providing a single source for diverse needs.

Full-Process Development Expertise

Beyond just technology, our chemical production solutions encompass full-process development, from initial consultation and system integration to final commissioning, ensuring a seamless transition from concept to profitable operation.

Related products

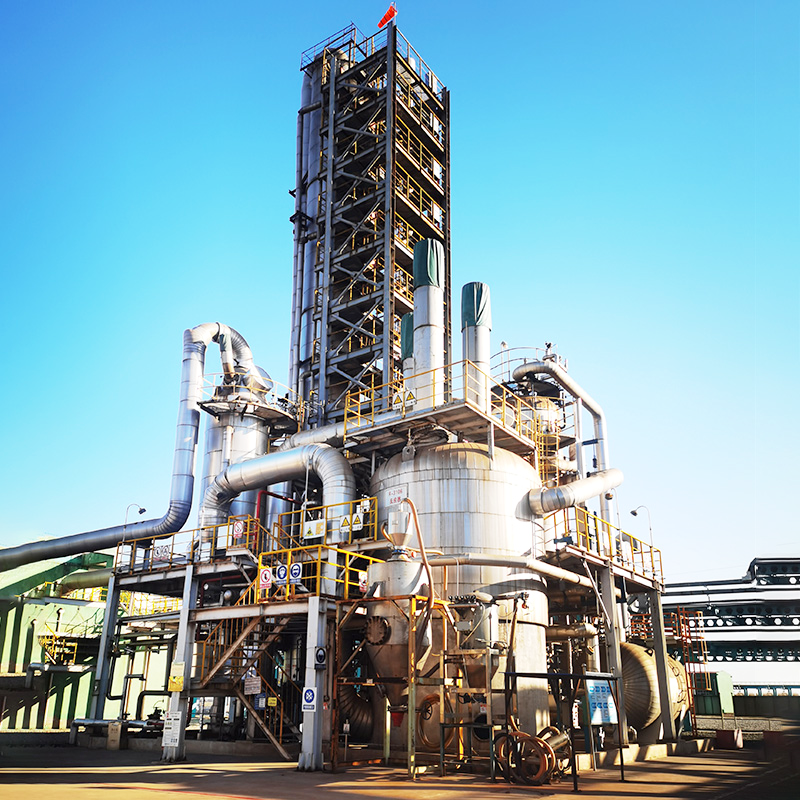
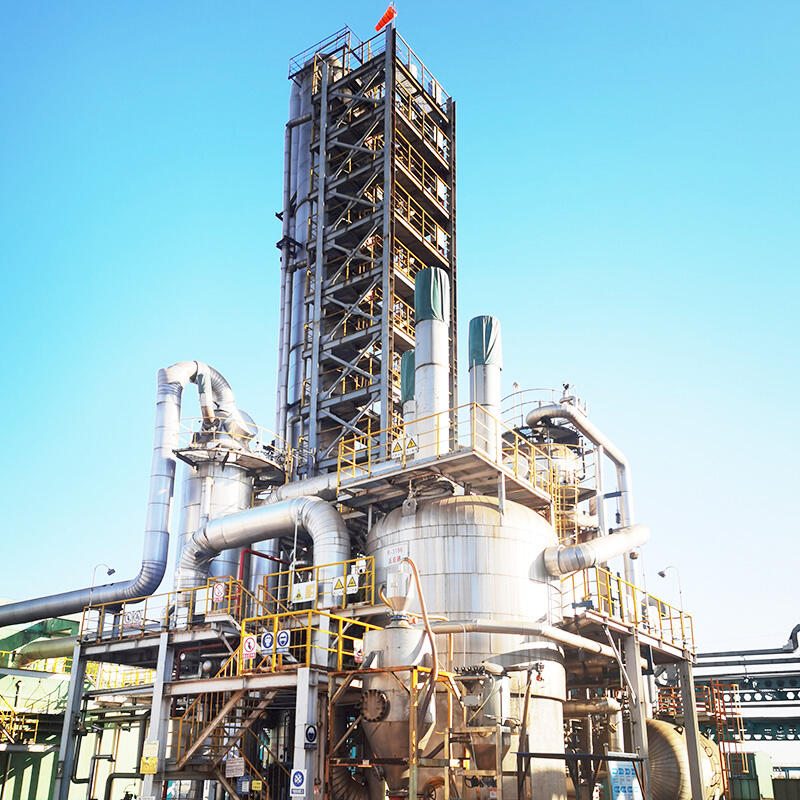
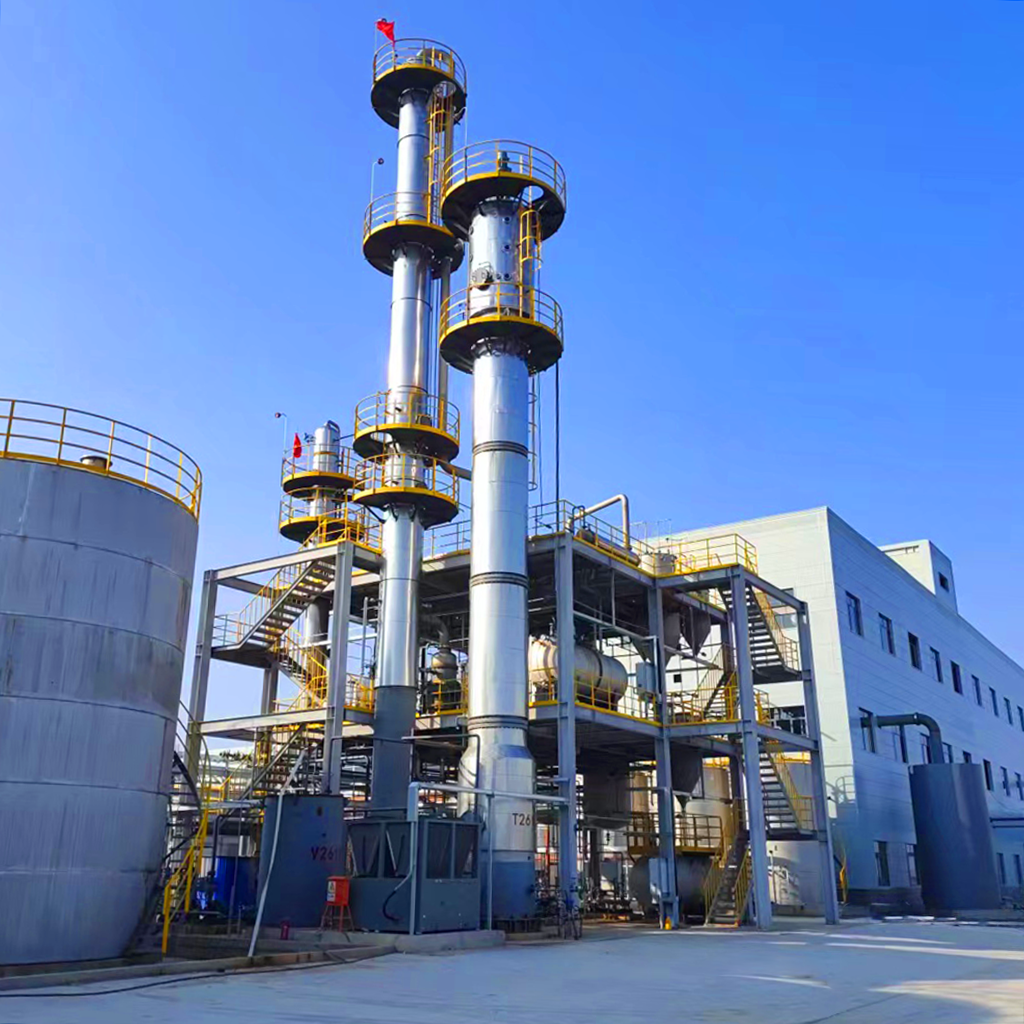
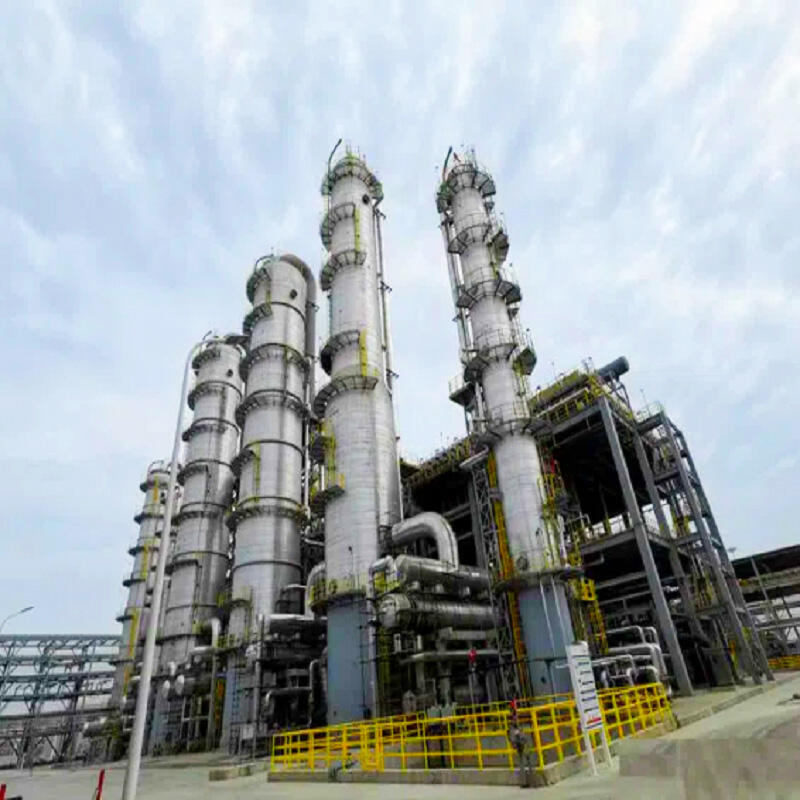
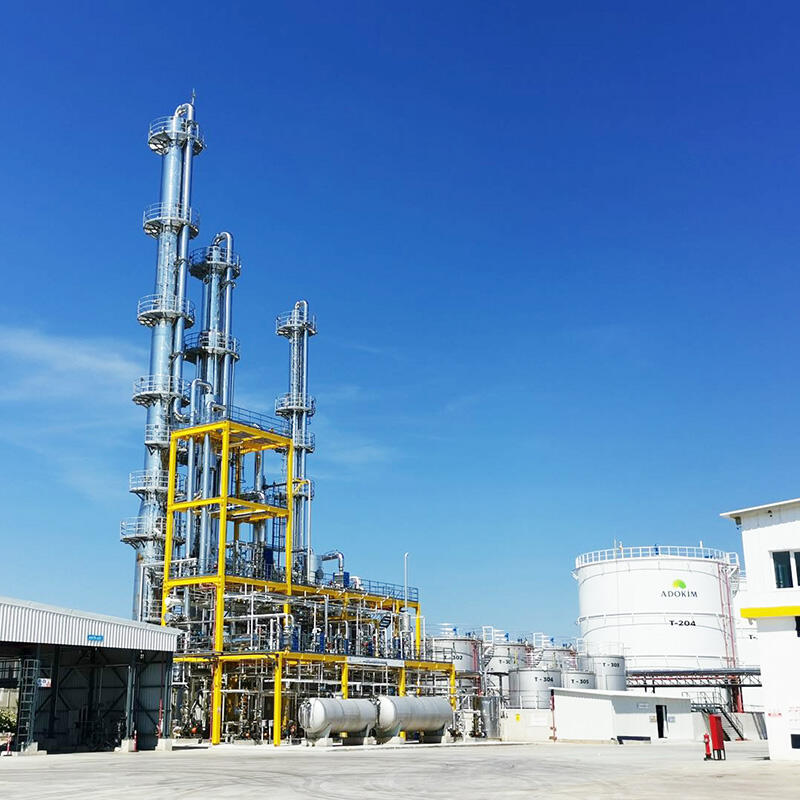
At Changzhou Sanli Tech International Trade Co., Ltd., we understand that chemical production is not merely about individual unit operations but a complex, integrated system demanding seamless coordination. Our chemical production solutions are built upon a foundation of over 172 complete sets of proprietary technologies, ranging from the Methanol Industry’s Formaldehyde (Fe-molybdenum and Silver Method) plants to advanced New Materials like the Polysulfone Plant. We serve as a one-stop partner, guiding clients from initial consultation through to full-scale production. For a client in the specialty chemicals sector seeking to establish a greenfield facility for Methylal via Pressure Swing Distillation, our solution begins with a deep analysis of feedstock availability and market demands, followed by the delivery of a customized process engineering package. Our solutions are particularly impactful in the Ethylene Industry, where we provide integrated plants for EO (Ethylene Oxide), MEG, and downstream derivatives like EOA and ETX, ensuring high-purity outputs and energy efficiency. By integrating system integration with full process development, and leveraging our R&D collaboration with the Institute of Process Engineering of the Chinese Academy of Sciences, we de-risk projects from the outset. Whether it’s a complex POM (Polyformaldehyde) plant or a specialized DMMn (Polyoxymethylene Dimethylether) unit, our solutions are engineered for profitability, reliability, and long-term operational excellence, ensuring that each plant runs smoothly and adds significant value to the customer’s factory.
Frequently Asked Questions

What is your experience in executing chemical plant projects?

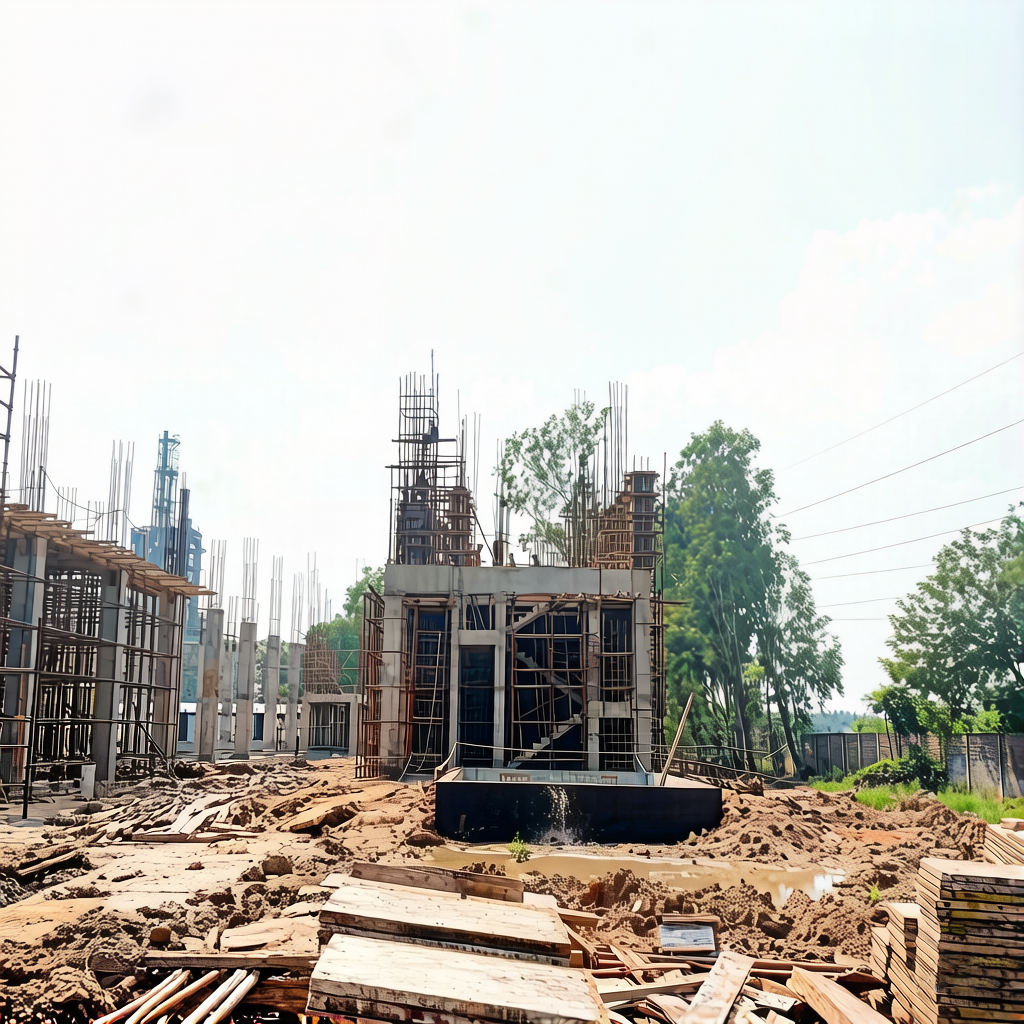
We have successfully set up chemical plants in over 9 cities, demonstrating our strong project execution capabilities. Our experience spans both greenfield and brownfield projects, and we have a proven track record of delivering reliable plants that run smoothly and add significant value to our customers’ operations.
Yes, we are a one-stop partner providing comprehensive services. Our offerings include system integration and full process development. We cover solution communication and consulting before sale, procurement and installation during plant construction, commissioning, and personal training for your team after the plant is completed.
We have developed and successfully deployed over 178 complete sets of chemical technology. This extensive portfolio demonstrates our deep expertise and ability to provide proven, reliable solutions for a diverse array of chemical production processes, from foundational C1 chemistry to advanced new materials.
We serve a vast range of essential chemical industries worldwide. Our portfolio includes the Methanol Industry (C1) with technologies for Formaldehyde, POM, DMMn, and Methylamines; the Ethylene Industry (C2) with EO, MEG, and derivatives; Ester Series; Acids; Phenol Series; Ketones; Ethers; New Materials like UHMWPE and Polysulfone; and specialized plants for Epichlorohydrin, DMSO, and Hydrogen Peroxide.

Related Articles

Polysulfone: The Star Performer in Advanced Engineering Plastics

03

Mar

Polysulfone: The Star Performer in Advanced Engineering Plastics

View More
Everything You Need to Know about Polysulfone Plastic

27

May

Everything You Need to Know about Polysulfone Plastic

View More
The Significance of Chemical Production Technology in Modern Manufacturing

23

Jul

The Significance of Chemical Production Technology in Modern Manufacturing

Explore sustainable manufacturing innovations in the chemical industry, highlighting green chemistry, energy efficiency, AI and IoT applications, polymer advancements, and compliance with global regulatory standards.
View More
The Role of Polymers in the Development of High - tech Industries

23

Jul

The Role of Polymers in the Development of High - tech Industries

Discover how polymer innovations are revolutionizing high-tech sectors, transforming manufacturing, sustainability, and technology applications. Explore the uses of photopolymers, high-performance polymers in aerospace, polyethylene glycol in drug delivery, and cutting-edge recycling methods for a greener future.
View More

Customer Reviews

Dr. Emily Carter

We selected Changzhou Sanli Tech to build our POM and Trioxane complex. Their integrated solution covered everything from process design to full plant commissioning. The team’s ability to handle both the Fe-molybdenum Formaldehyde unit and the downstream polymer plant as one seamless system was impressive. The plant achieved performance guarantees ahead of schedule, and the personal training provided ensured our operators were confident from day one.

Carlos Mendez

We contracted Sanli Tech for a grassroots EO and MEG facility. Their turnkey solution, which included the supply of all equipment and the installation of advanced control systems, simplified our project management. The solution was scalable, allowing us to add downstream EOA and GE units later with minimal disruption. The reliability of their technology and the professionalism of their project team were exceptional.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/Whatsapp
Name
Company Name
Message
0/1000
Integrated One-Stop Chemical Production Solutions

Integrated One-Stop Chemical Production Solutions

As a global vendor with over 178 complete sets of chemical technology, we provide fully integrated solutions that cover the entire project lifecycle. Our one-stop service includes solution communication, consulting, procurement, installation, commissioning, and personal training. We serve a vast range of essential industries, from the Methanol Industry to New Materials, ensuring each plant is designed for profitability and long-term operational excellence.